SET-UP AND SAFE OPERATING PROCEDURES
6-39
0056-0114
3. Open the torch handle oxygen valve. Release the pressure from the system and then close
the torch oxygen valve.
4. Turn the adjusting screw on the oxygen regulator counterclockwise to release all spring
pressure.
5. Open the torch handle fuel valve and release the pressure from the system. Close the torch
fuel valve.
6. Turn the adjusting screw on the fuel gas regulator counterclockwise to release all spring
pressure.
7. Check the inlet gauges after a few minutes to ensure the cylinder valves are turned off
completely and there is no pressure remaining in the system.
TIPS TO IMPROVE WELD QUALITY
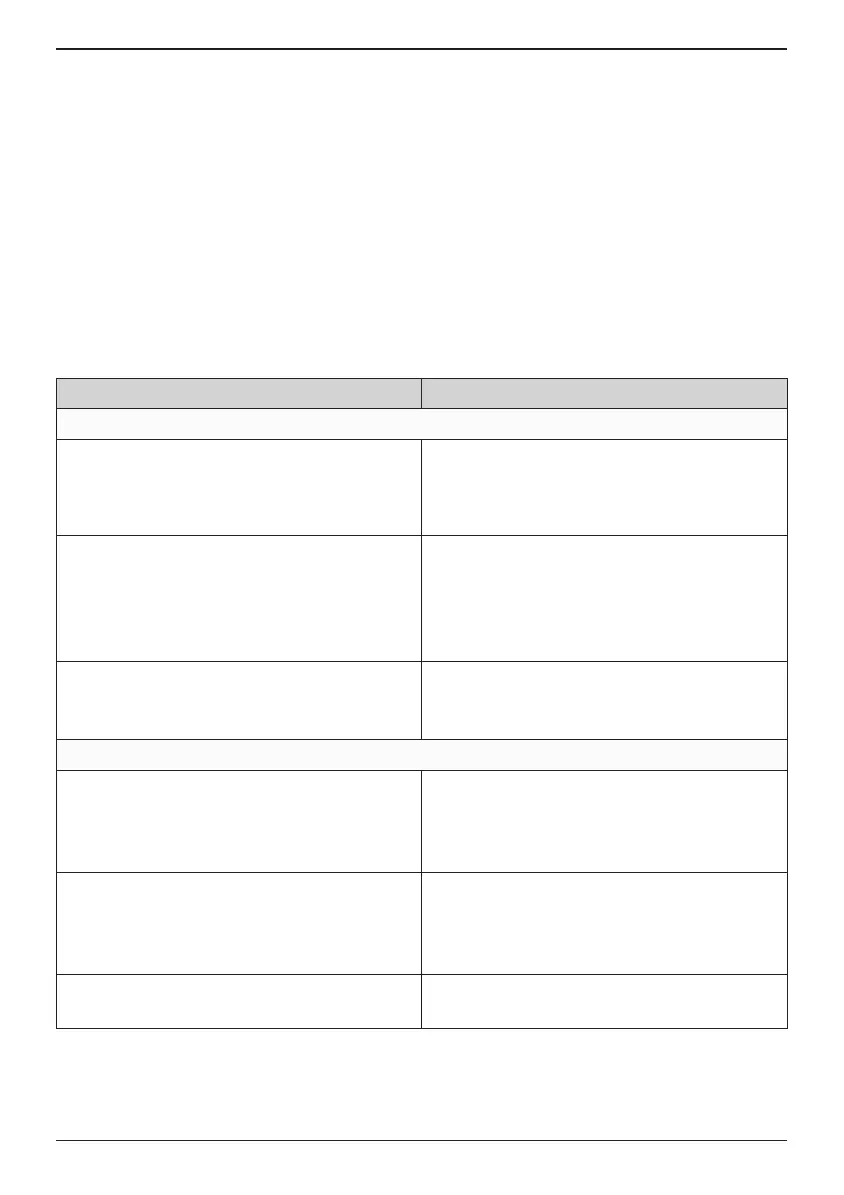
Problem Features Corrective Action
Distortion
1. Shrinkage of deposited metal, pulls welded
parts together and changes their relative
positions.
1. Properly clamp or tack parts to resist
shrinkage. Separate or preform parts
sufficiently to allow for shrinkage of the
welds.
2. Non-uniform heating of parts during
welding causes them to distort or buckle
before welding is finished. Final welding of
parts in distorted position prevents control
of desired dimensions.
2. Support parts of the structure to be welded
to prevent buckling in heated sections, due
to the eight of the parts themselves.
3. Improper welding sequence. 3. Study the structure and develop a definite
sequence of welding. Distribute welding to
prevent excessive local heating.
Welding Stresses
1. Joints too rigid. 1. Slight movement of parts during welding
will reduce welding stress. Develop
welding price duress that permits all parts
to be free to move as long as possible.
2. Incorrect welding procedure. 2. Make the weld in as few passes as
possible. Use special intermittent or
alternating welding sequences. Properly
clamp parts adjacent to the joint.
3. Inherent in all welds, especially in heavier
parts.
3. Peen each deposit of weld metal. Stress-
relieve finished product.
Welding Procedures


 To Next Page
 Loading...