ENGINE REPAIR (Cont'd)
To
Check Crankshaft Or Connection Rod
Bearings
With Plastigage
(Cont'd)
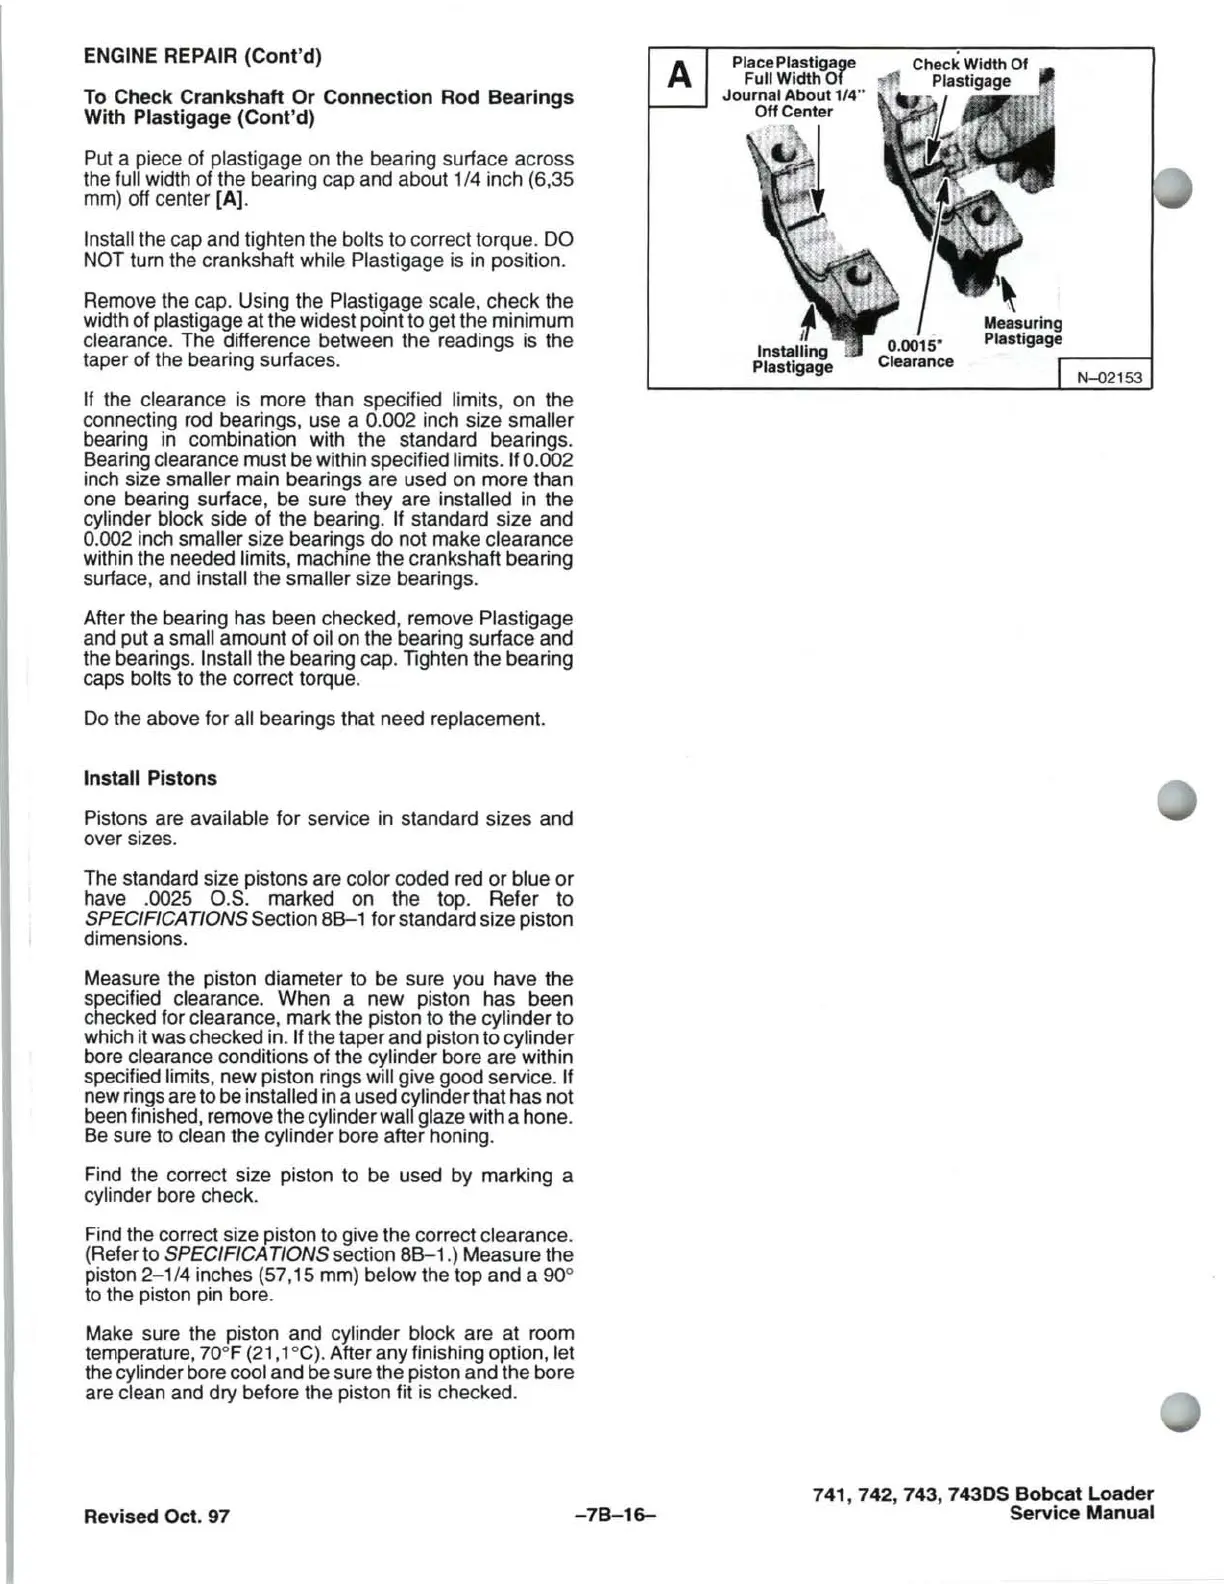
Put
a piece of plastigage on the bearing surface across
the
full width of the bearing cap and about 1/4 inch (6,35
mm)
off center [A].
Install the cap and tighten the bolts to correct torque. DO
NOT
turn the crankshaft while Plastigage
is
in
position.
Remove the cap. Using the
Plastigage scale, check the
width of
plastigage at the widest point to get the minimum
clearance. The difference between the readings is the
taper of the bearing surfaces.
If
the clearance
is
more than specified limits, on the
connecting
rod
bearings, use a 0.002 inch size smaller
bearing
in
combination with the standard bearings.
Bearing
clearance must be within specified limits. If 0.002
inch size smaller main bearings are used on more than
one bearing surface, be sure they are
installed
in
the
cylinder block side of the bearing. If standard size and
0.002 inch smaller size bearings do not make clearance
within the needed limits, machine the crankshaft bearing
surface, and
install the smaller size bearings.
After the bearing has been checked, remove
Plastigage
and put a small amount of oil on the bearing surface and
the bearings.
Install the bearing cap. Tighten the bearing
caps
bolts to the correct torque.
Do the above for
all bearings that need replacement.
Install Pistons
Pistons are available for service in standard sizes and
over sizes.
The standard size pistons are
color coded red or blue
or
have .0025 O.
S.
marked on the top. Refer to
SPECIFIC A TlONS Section
88-1
for standard size piston
dimensions.
Measure the piston diameter to be sure you have the
specified
clearance. When a new piston has been
checked for
clearance, mark the piston to the cylinder to
which it was checked in.
If the taper and piston to cylinder
bore clearance conditions of the cylinder bore are within
specified limits, new piston rings
will give good service. If
new rings are to be installed
in
a used cylinder that has not
been finished, remove the cylinder
wall glaze with a hone.
Be
sure to clean the cylinder bore after honing.
Find the correct size piston to be used by marking a
cylinder bore check.
Find the correct size piston to give the correct clearance.
(Refer to
SPECIFICATIONS section
88-1.)
Measure the
piston 2-1/4 inches (57,15 mm)
below the top and a 90°
to the piston pin bore.
Make sure the piston and
cylinder block are at room
temperature,
70
°F
(21
,1 °C). After any finishing option, let
the cylinder bore cool and
be
sure the piston and the bore
are clean and dry before the piston fit
is
checked.
Revised Oct. 97
-7B-16-
A
PlacePlastigage
Full
Width
Of
Journal
About
114"
Off
Center
N-{)2153
741,742,
743,
74305
Bobcat Loader
Service
Manual


 To Next Page
 Loading...