CYLINDER HEAD (Cont'd)
Servicing (Cont'd)
The correct width of the valve seat
is
0.0827 inch
(2,1
mm)
and the seat angle
is
45 degrees.
Grind the
valve seats as follows:
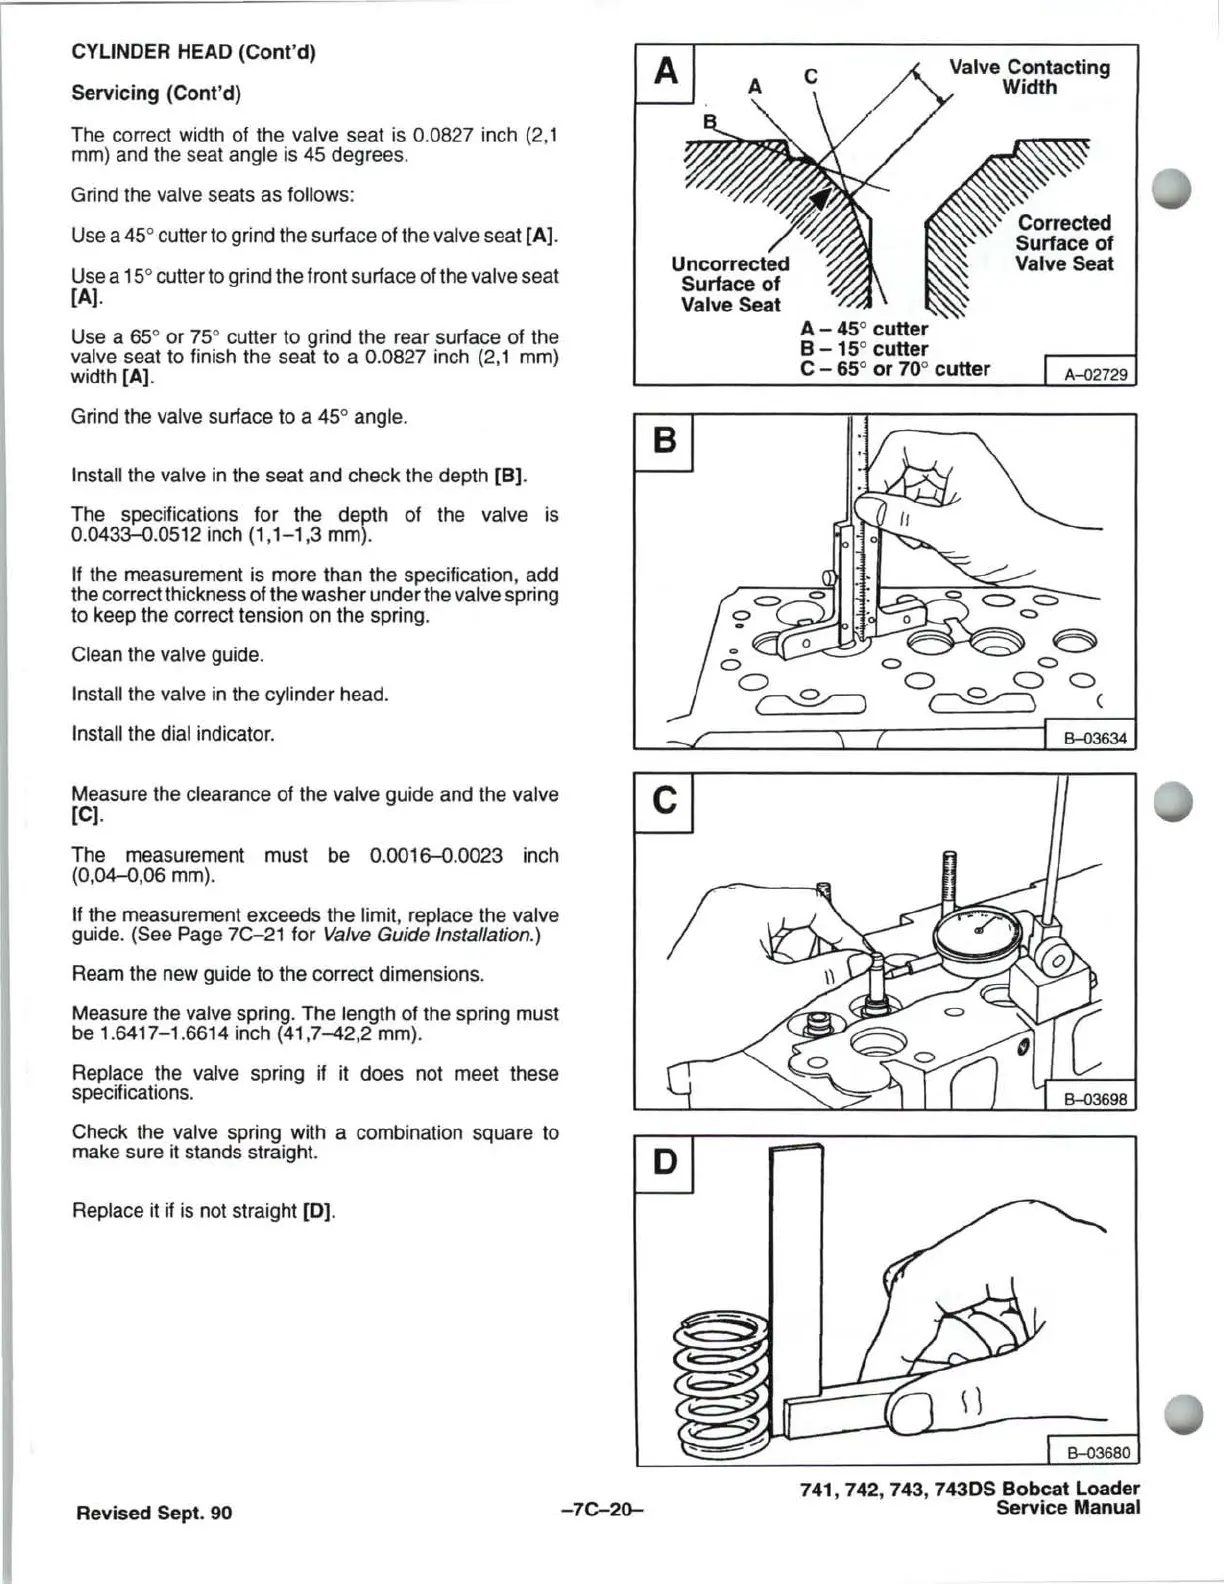
Use a 45° cutter to grind the surface of the valve seat [A).
Use a
15° cutter to grind the front surface
of
the valve seat
[A).
Use a
65
° or 75° cutter to grind the rear surface of the
valve seat to finish the seat to a 0.0827 inch
(2,1
mm)
width [A).
Grind the
valve surface to a 45° angle.
Install
the valve
in
the seat and check the depth
(8).
The specifications for the depth of the valve is
0.0433-0.0512 inch
(1
,
1-1,3
mm).
If
the measurement is more than the specification, add
the correct thickness of the washer under the
valve spring
to keep the correct tension on the spring.
Clean the valve guide.
Install the valve
in
the cylinder head.
Install the dial indicator.
Measure the clearance of the
valve guide and the valve
[C).
The measurement must be 0.0016-0.0023 inch
(0,04-0,06 mm).
If the measurement exceeds the limit, replace the valve
guide. (See Page 7C-21 for Valve Guide Installation.)
Ream the new guide to the correct dimensions.
Measure the
valve spring. The length of the spring must
be 1.6417-1.6614 inch (41,7-42,2 mm).
Replace the
valve spring if it does not meet these
specifications.
Check the
valve spring with a combination square to
A
B
make sure
it
stands straight. D
Replace it
if
is
not straight
[0]
.
Revised Sept. 90
-7C-2G-
..
A-45
°
cutter
8 - 15°
cutter
Valve Contacting
Width
Corrected
Surface
of
Valve Seat
C - 65°
or
70°
cutter
A-02729
a
o
o 0
° 0
~
°0°0
~
(
B-03634
741, 742, 743, 7430S
80bcat
Loader
Service Manual


 To Next Page
 Loading...