VALVES (Cont'd)
Reconditioning The
Valve And Valve Seat
Use
the correct equipment to grind the valve and valve
seats.
The
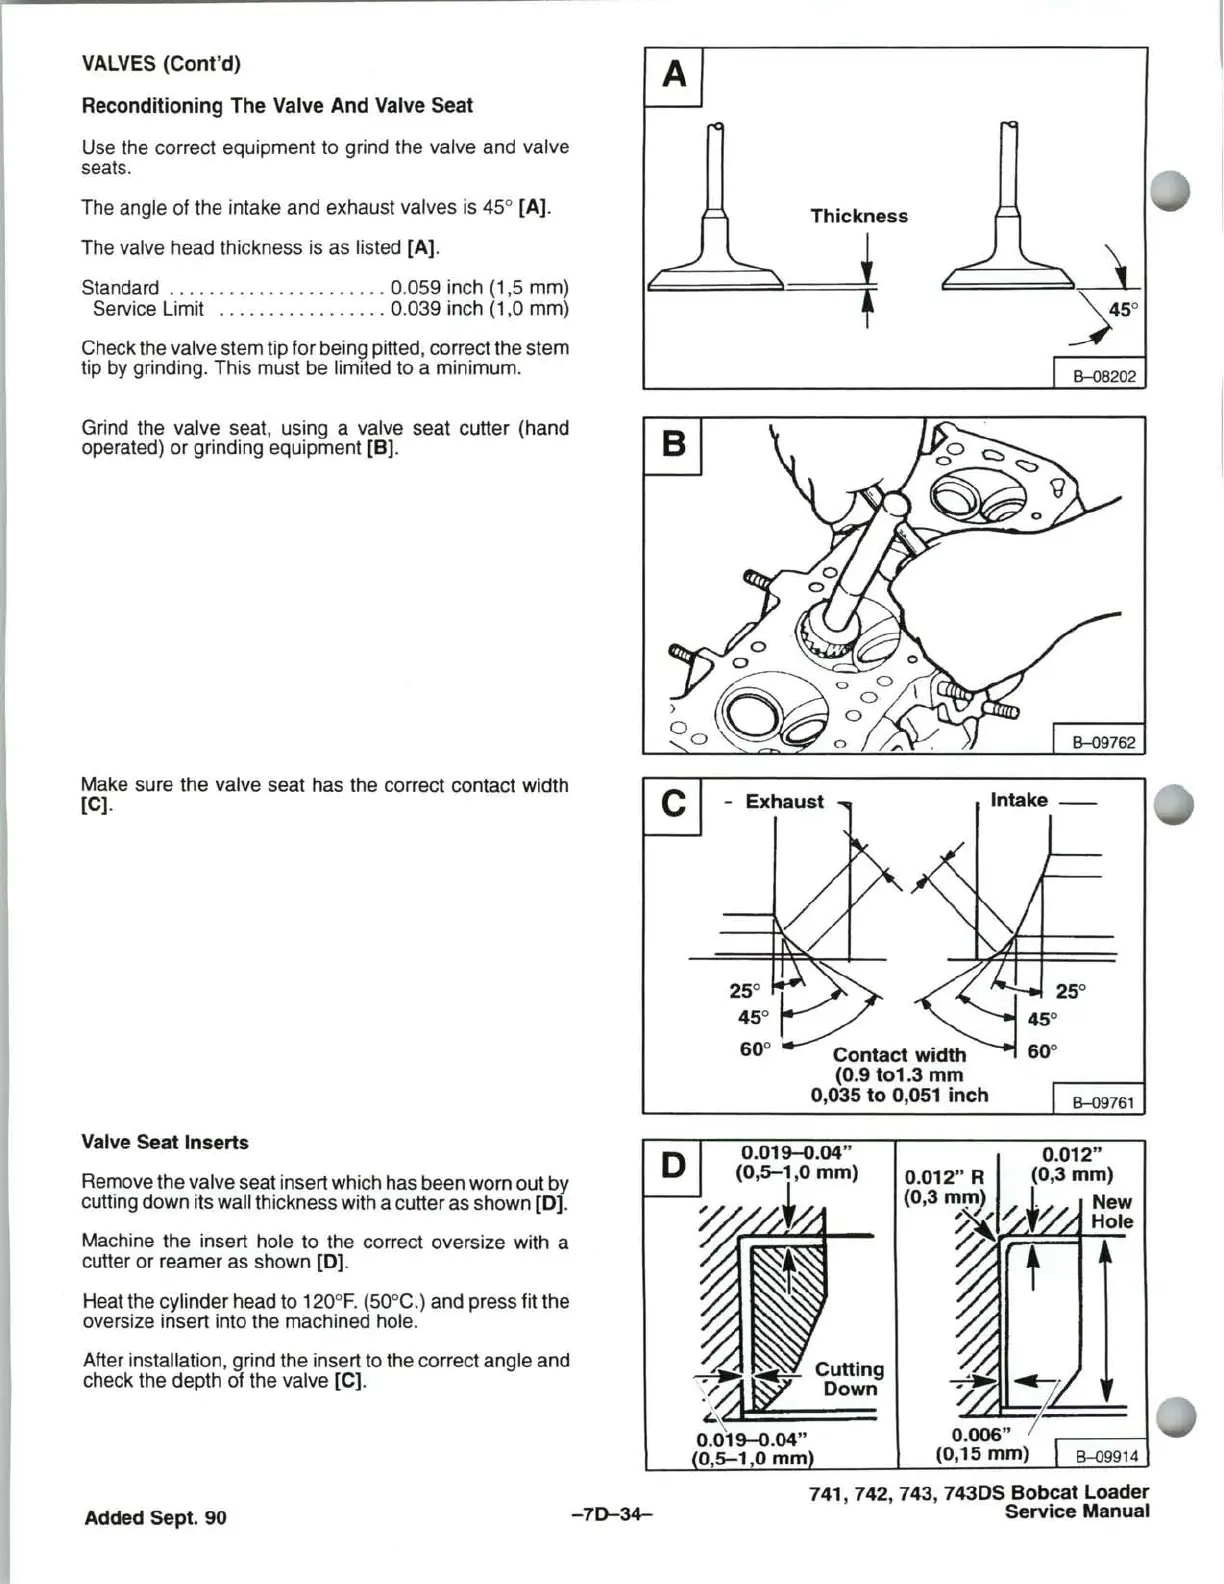
angle of the intake and exhaust valves is 45° [A].
The valve head thickness is as listed [A).
Standard
...................
..
. 0.059 inch (1,5 mm)
Service Limit
..
.
..
.
.....
......
0.039 inch
(1
,0 mm)
Check the
valve stem tip for being pitted, correct the stem
tip by grinding. This must be limited to a minimum.
Grind the valve seat, using a valve seat cutter (hand
operated) or grinding equipment [B].
Make sure the valve seat has the correct contact width
[C].
Valve Seat Inserts
Remove the valve seat insert which has been worn out by
cutting down its wall thickness with a cutter as shown
[0].
Machine the insert hole to the correct oversize with a
cutter or reamer as shown [0).
Heat the cylinder head to 120°
F.
(50°C.) and press fit the
oversize insert into the machined hole.
After installation, grind the insert to the correct angle and
check the depth of the valve [C).
Added
Sept. 90
A
c
-70-34-
Thickness
- Exhaust
Contact width
(0.9
tol.3
mm
0,035
to
0,051 inch
~
~
Cutting
'
~
<?1W
Down
L~
0.019-0.04"
0,5-1,0
mm
EH:l8202
EH:l9761
741,742,743,
7430S
Bobcat Loader
Service Manual


 To Next Page