233
by Schnell
Verificare che gli utensili montati
corrispondano al diametro del
tondino.
Operare come segue:
1 - Posizionare il selettore MAN/
PROG/AUT su “MAN” e
togliere la chiave.
2 - Portare l'albero di piega in
posizione centrale per
agevolare la regolazione della
vite di traslazione.
3 - Regolare la corsa della
traslazione del gruppo piega in
base al diametro "Ø" del ferro
e al diametro "D" del mandrino
centrale
La regolazione della corsa della
traslazione viene eseguita nel
seguente modo:
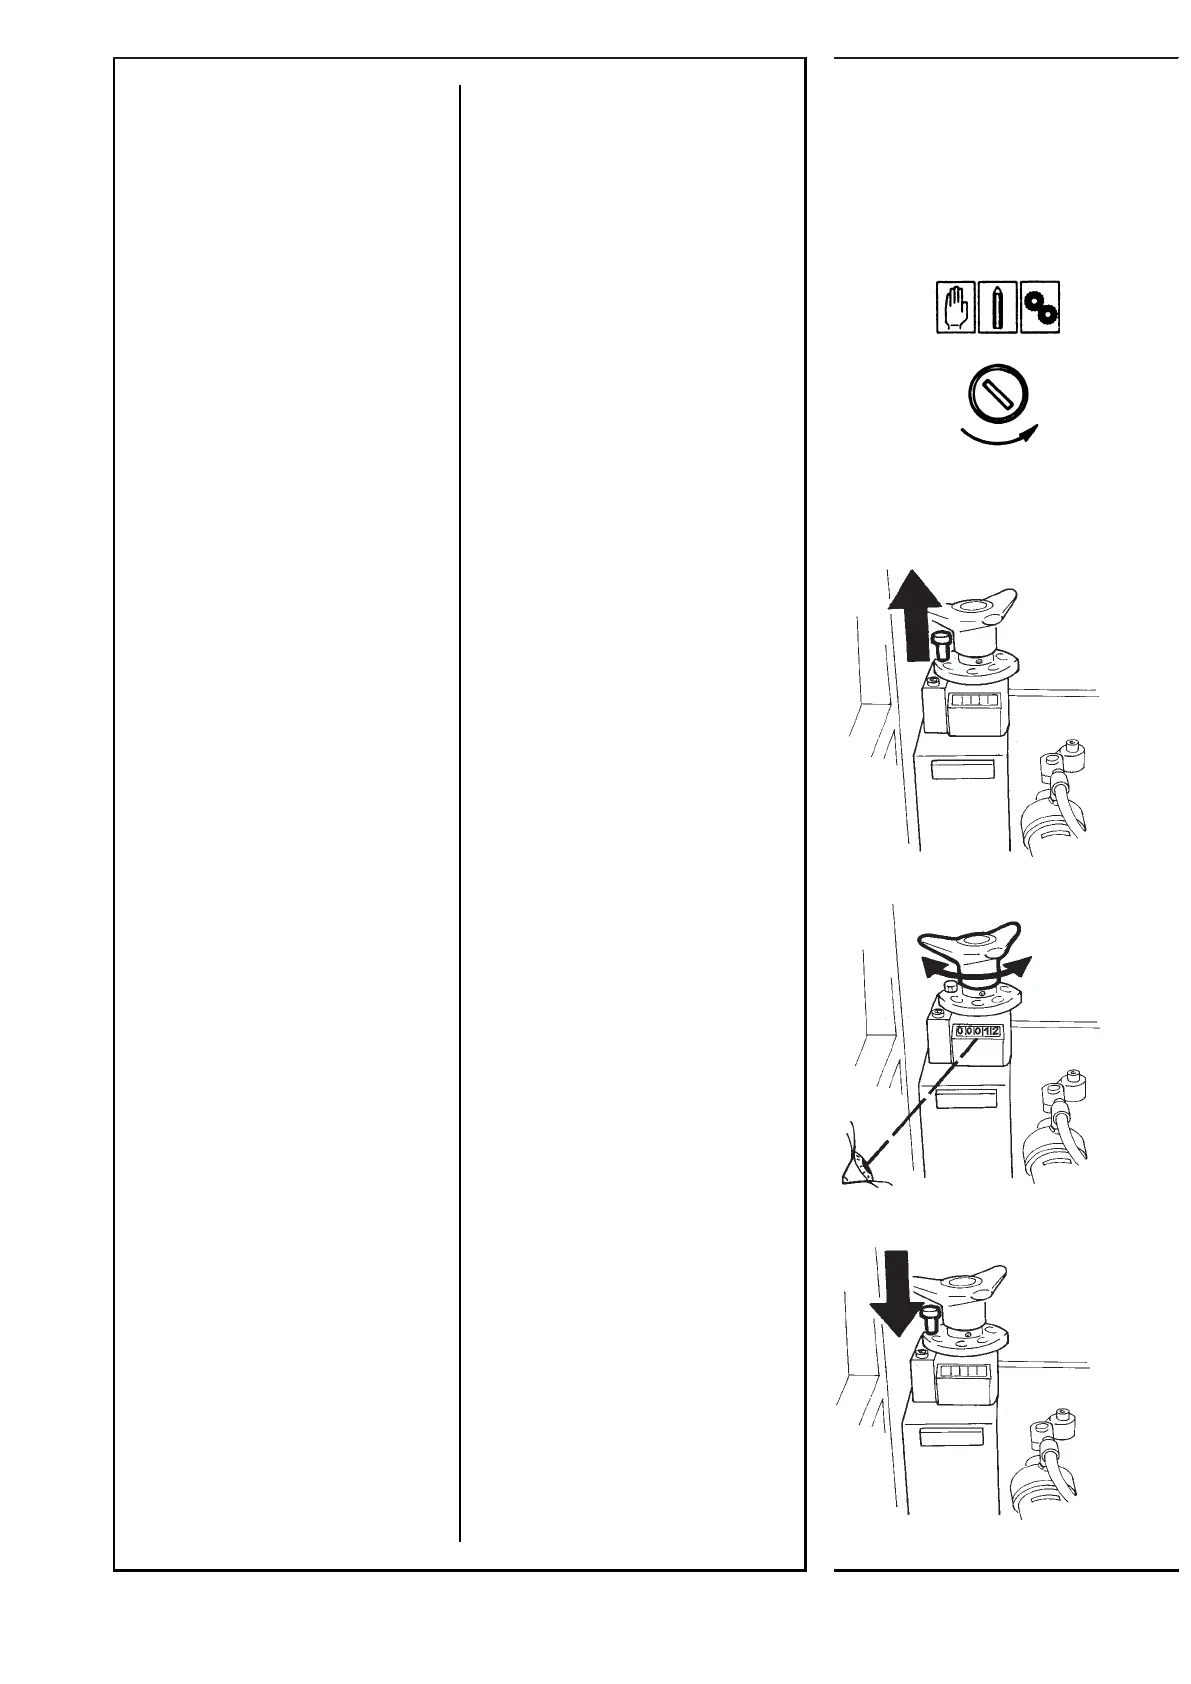
- Sbloccare il volantino togliendo
il perno impegnato nel foro di
bloccaggio.
- Ruotare il volantino, situato a
sinistra del gruppo di piega, in
senso orario o antiorario fino a
quando il visualizzatore digitale
non indicherà il valore richiesto
(considerare solamente le cifre
su fondo nero).
Tale valore è rappresentato dalla
somma del diametro "Ø" del
tondino in lavorazione con il
diametro "D" del mandrino centrale
di piega. Ad esempio, lavorando
un tondino di diametro Ø = 12 mm
con un mandrino di diametro D =
50 mm, si regolerà il volantino fino
a far apparire sul visualizzatore la
cifra 62.
Make sure the tools fitted
correspond to the diameter of the
rod.
Proceed as follows:
1 - Set the MAN/PROG/AUT
selector on “MAN” and remove
the key.
2 - Move the bending shaft into
central position to facilitate
adjustment of the translation
screw.
3 - Adjust the bending unit
translation travel on the basis
of the rod diameter “Ø” and the
diameter “D” of the central
mandrel.
The translation travel is adjusted
as follows:
- Release the handwheel by
removing the pin engaged in
the locking hole.
- Turn the handwheel, located
to the left of the bending unit,
clockwise or anticlockwise until
the digital display shows the
required value (only consider
the numbers on black
background).
This value is represented by the
sum of the diameter “Ø” of the rod
being machined and the diameter
“D” of the central bending mandrel.
For example, machining a rod of
diameter Ø = 12 mm with a mandrel
of diameter D = 50 mm, adjust the
handwheel until the number 62
appears on the display.


 To Next Page
 Loading...
