EasyManua.ls Logo

Taurus TIG200ACDC-HF-P - Page 25

Taurus TIG200ACDC-HF-P
29 pages
Print Icon
To Next Page IconTo Next Page
To Previous Page IconTo Previous Page
Loading...
OPERATION
25
Note: the above parameters originate from《Welding Dictionary》P150, Volume 1 of Edition 2.
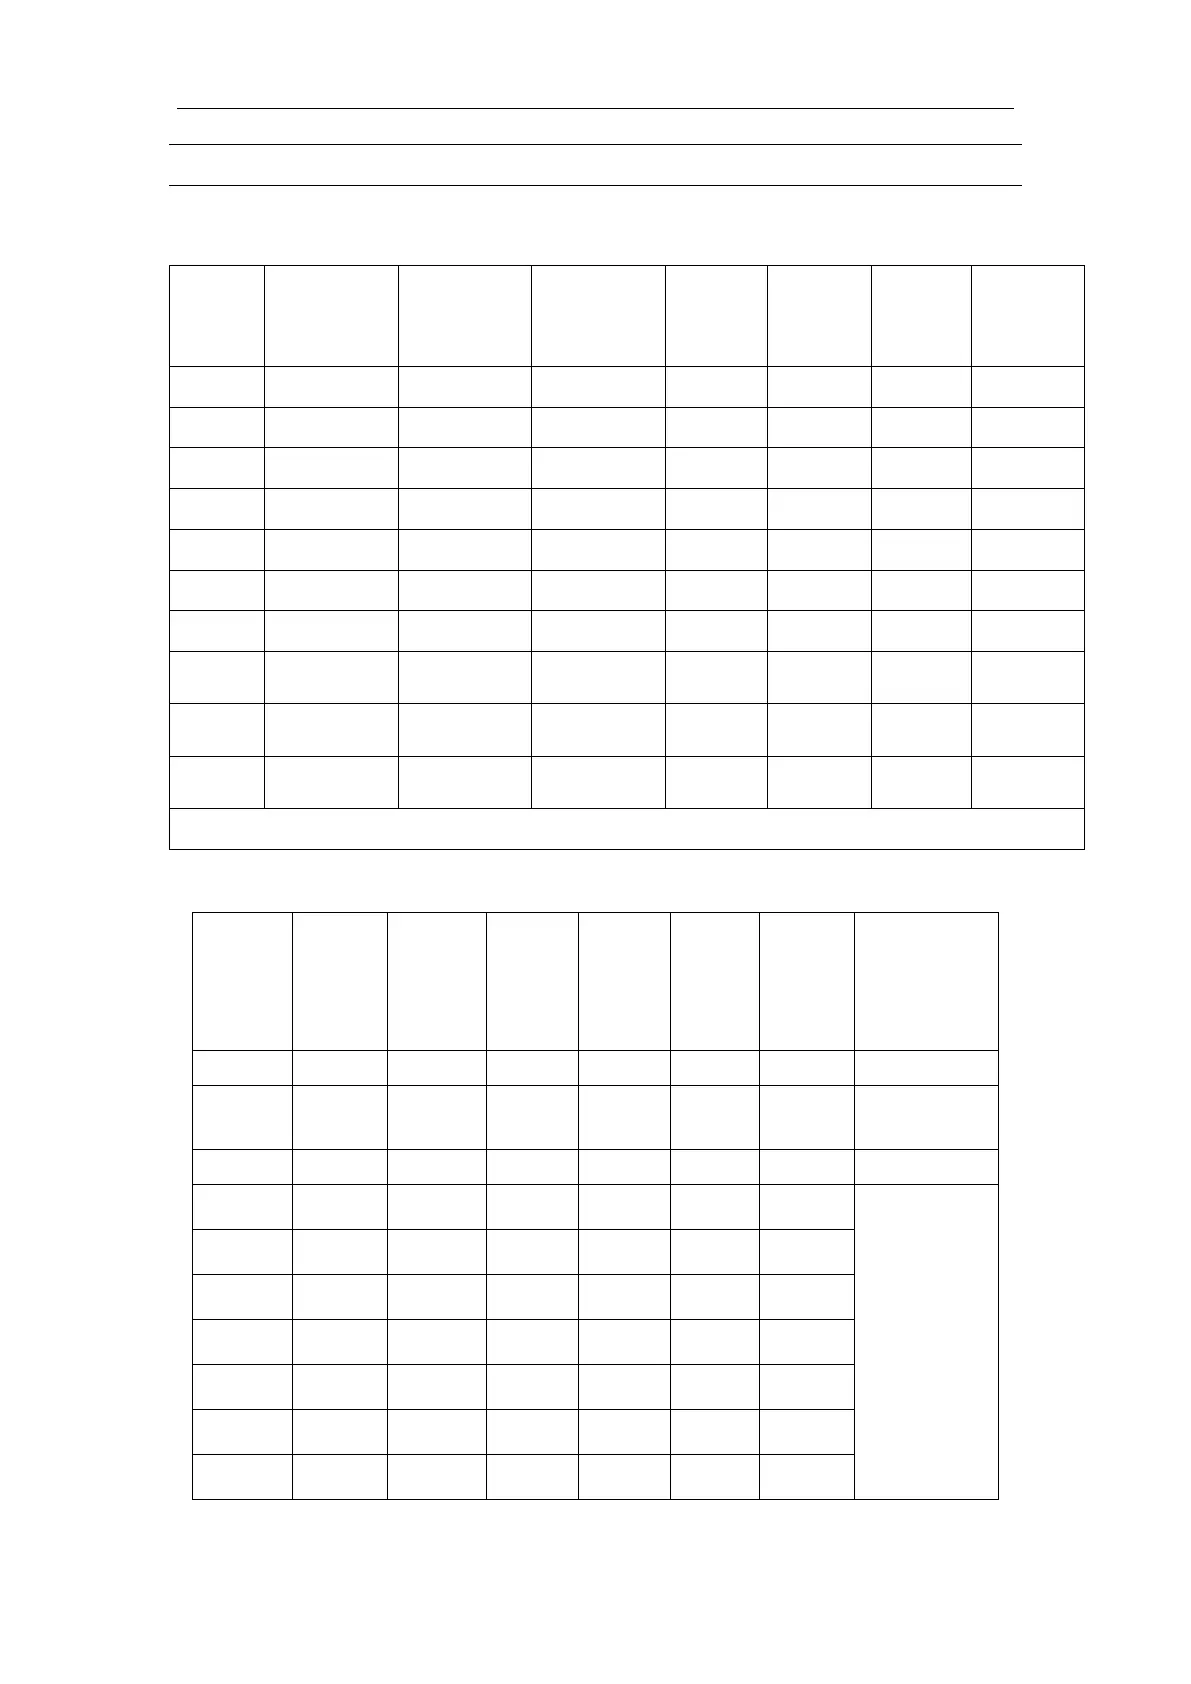
Parameters of AC TIG (MMA) for Aluminum and its alloy
Sheet
thickness
/mm
Welding
wire
diameter
/mm
Tungsten
electrode
diameter
/mm
Pre-heat
Temper
-ature
/℃
Welding
current
/A
Argon
flow
rate
/
L·min
-1
Gas
nozzle
diameter
/mm
Remark
1
1.6
2
-
45~60
7~9
8
Flange welding
1.5
1.6~2.0
2
-
50~80
7~9
8
Flange or butt
welding by one
side
2
2~2.5
2~3
-
90~120
8~12
8~12
Butt welding
3
2~3
3
-
150~
180
8~12
8~12
V-groove butt
welding
4
3
4
-
180~
200
10~15
8~12
5
3~4
4
-
180~
240
10~15
10~12
6
4
5
-
240~
280
16~20
14~16
8
4~5
5
100
260~
320
16~20
14~16
10
4~5
5
100~
150
280~
340
16~20
14~16
12
4~5
5~6
150~
200
300~
360
18~22
16~20
Parameters of piping back sealing welding for mild steel(DCEP)
Piping
diameter
Φ/mm
Tungsten
electrode
diameter/mm
Gas nozzle
diameter/mm
Welding
wire
diameter/mm
Welding
current/A
Arc
voltage/V
Argon
flow rate
/
L·min
-1
Welding
rate
/
cm·min
-1
38
2.0
8
2
75~90
11~13
6~8
4~5
42
2.0
8
2
75~95
11~13
6~8
4~5
60
2.0
8
2
75~100
11~13
7~9
4~5
76
2.5
8~10
2.5
80~105
14~16
8~10
4~5
108
2.5
8~10
2.5
90~110
14~16
9~11
5~6
133
2.5
8~10
2.5
90~115
14~16
10~12
5~6
159
2.5
8~10
2.5
95~120
14~16
11~13
5~6
219
2.5
8~10
2.5
100~
120
14~16
12~14
5~6
273
2.5
8~10
2.5
110~
125
14~16
12~14
5~6
325
2.5
8~10
2.5
120~
140
14~16
12~14
5~6
Note: the above parameters originate from《Welding Dictionary》P167, Volume 1 of Edition 2.

Related product manuals