SET-UP AND SAFE OPERATING PROCEDURES
6-37
0056-0114
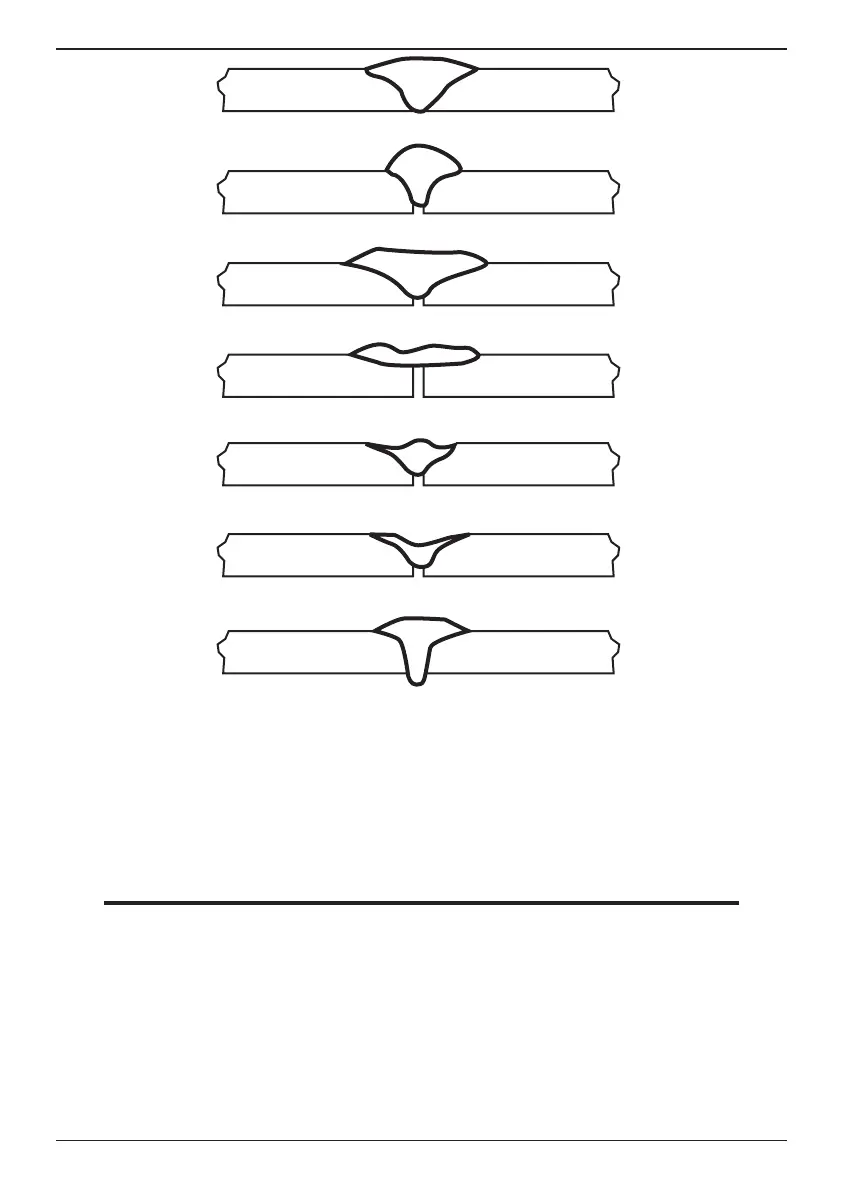
CORRECT WELD CONTOUR
EXCESSIVE REINFORCEMENT
EXCESSIVE WIDTH
LACK OF PENETRATION
UNDERCUTTING
UNDERFILL
BURN THROUGH
dwg-00389
Figure 16: Characteristics of Good and Bad Welding Joints
6.05 OXY-FUEL BRAZING AND BRAZE WELDING
Brazing is a process characterized by heating the base metal to temperatures above 840 °F, while
remaining below the metal’s melting point. Generally speaking, most metals can be joined with a
simple brazing operation as long as the correct filler rod or flux is used.
NOTE
Always ensure you are using the proper filler rod and flux for the job at hand.
Contact your local VICTOR
®
supplier for charts on the various filler rods and fluxes that are available.
Flux is required to prepare the metals for joining.
Like Arc Welding, brazing uses molten metal to join two pieces of metal. The metal added during the
process has a melting point lower than that of the work piece. Brazing uses metals with a higher
melting point, (840 °F).
Brazing does not melt the metal being worked on. The brazing process does not normally create
distortions or weaknesses in the metal work piece that may occur with other welding applications.
Welding Procedures


 To Next Page
 Loading...