6-36
SET-UP AND SAFE OPERATING PROCEDURES
0056-0114
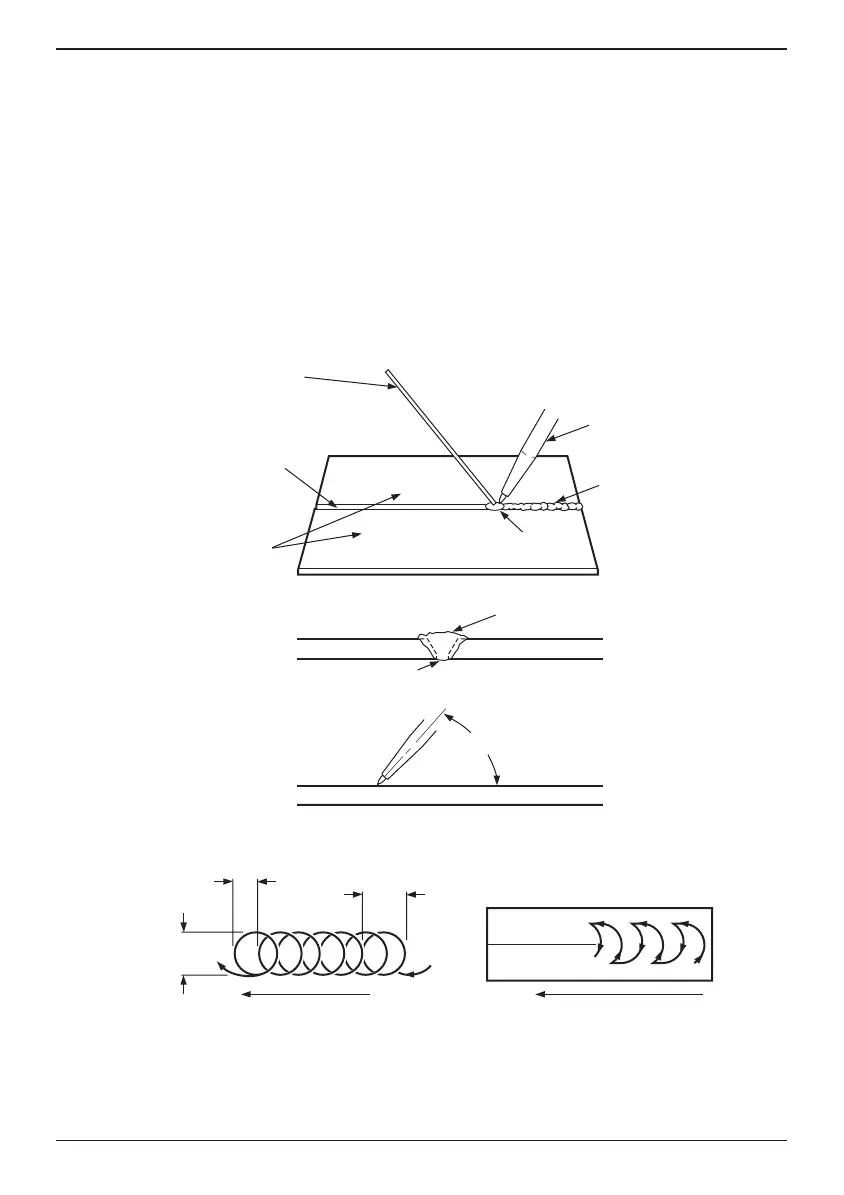
Move the torch nozzle over the starting edges of the joint. Rotate the flame near the metal 3.
in a circular or semicircular motion until the base metals run into a small puddle.
Dip the end of the filler rod in and out of the molten puddle, this melts the rod and adds to 4.
the puddle.
Continue the dipping motion of the filler rod into the puddle. Then move the torch back and 5.
forth across the joint.
Advance the torch nozzle at a rate of approximately 1/16” of the filler rod as it is added to 6.
the puddle until the end of the joint is achieved.
Since the angle of the nozzle flame is preheating the metals ahead of the weld, the last 1/2” 7.
of the weld is critical. Increase the addition of the filler rod to ensure a full smooth weld. Refer
to Figure 16, page 38 for the visual characteristics of a good and bad weld joint.
WELDING ROD
WELDING NOZZLE
BEAD
CONVEX BEAD
GOOD PENETRATION
AVERAGE PER
OVAL ABOUT 1/16"
ABOUT 5/16"
START
DIRECTION OF WELD
FLAME ROTATION
TORCH ANGLE
ABOUT 1/4"
30˚ to 45˚
PUDDLE
BUTT JOINT
BASE METAL
dwg-00388
Figure 15: Starting and Finishing a Weld
Welding Procedures


 To Next Page
 Loading...