SET-UP AND SAFE OPERATING PROCEDURES
6-45
0056-0114
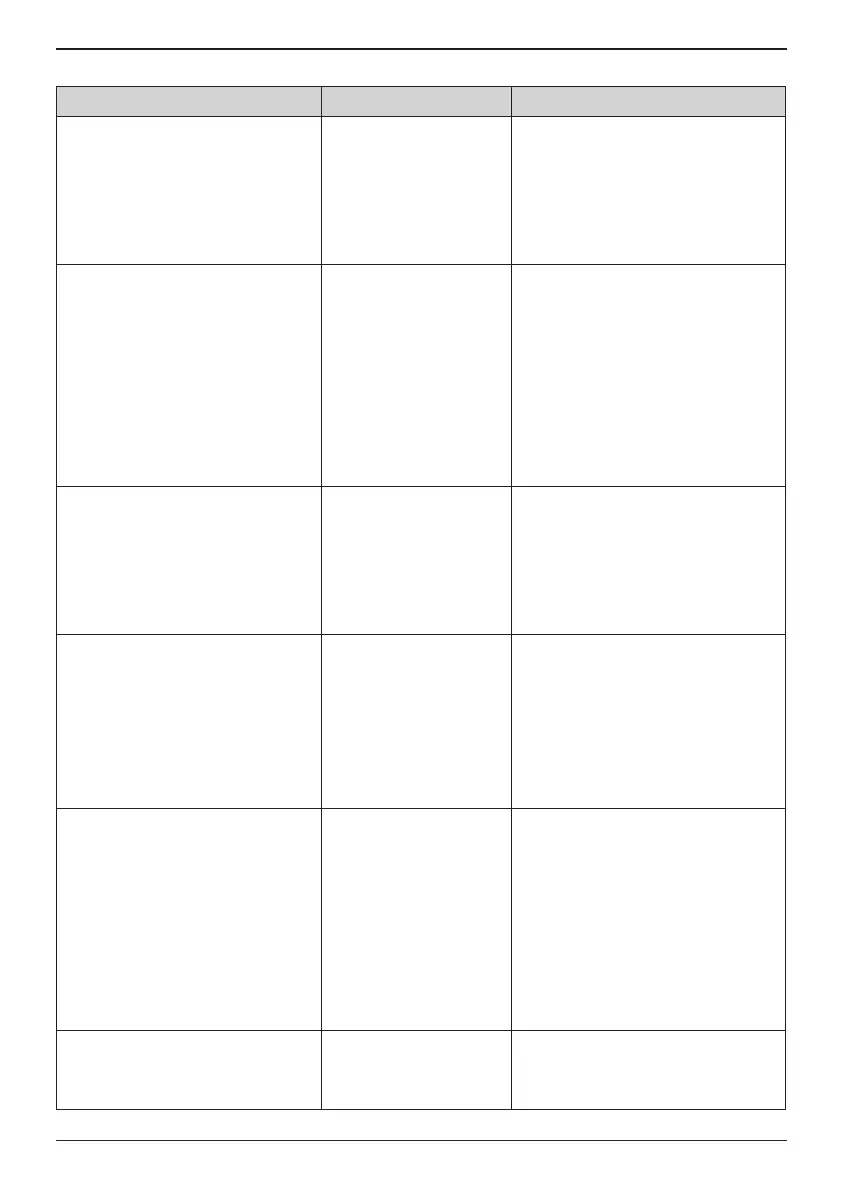
FLUXES
Flux and Use Application Removal
CAST IRON: Fusion welding of
cast iron.
Dip heated rod into flux
and apply to job.
1. Grinding wheel or wire brush
and water.
2. Sandblast.
3. Diluted hydrochloric or nitric
acid dip.*
COPPER AND BRASS: Fusion
of cast iron. Welding of copper,
brass and bronze. Braze welding
and brazing of copper
Dip heated rod into flux
and apply to job. For
brazing application mix
with water to form a
paste and apply to job
and rod.
1. Grinding wheel or wire brush
and water.
2. Sandblast.
3. Diluted hydrochloric or and
and steel. job and rod.
STAINLESS STEEL: Fusion
welding of all corrosion-resistant
steels of the chromium nickel
series.
Mix with alcohol or
water to form a paste.
Apply to job and rod.
1. Grinding wheel or wire brush
and water.
2. Sandblast.
3. Diluted hydrochloric or nitric
acid dip.*
SILVER BRAZING FLUX NO. 2:
Used with silver brazing alloys
235, 242, 245 and 250 on carbon
and stainless steels, nickel alloys,
copper and brass. Dissimilar
metals in the above groups can
be brazed.
Apply paste to job
and rod before
commencing to braze.
1. Hot dilute caustic soda dip.
2. Wire brush and hot water.
3. Wire brush and steam.
SILVER BRAZING FLUX
GENERAL PURPOSE:
Recommended to be used with
SBAs 102, 105, 115, 230, 234,
235, 350, 2503 and 3402. It is
excellent flux for medium to high
temperature brazing and has
been specially formulated to be
used for inductive brazing.
Apply paste to job
and rod before
commencing to braze.
(Adequate flux is
essential for proper
action.)
1. Hot dilute caustic soda dip.
2. Wire brush and hot water.
3. Wire brush and steam.
VERAFLUX: An efficient flux
applied as vapor in the flame for
braze welding steel.
Delivered to the torch
by means of a Vapaflux
Dispenser.
1. Usually not required; if
necessary, wipe with cloth.
* See note.
Welding Procedures


 To Next Page
 Loading...