6-44
SET-UP AND SAFE OPERATING PROCEDURES
0056-0114
TIPS TO IMPROVE WELD QUALITY
Problem Features Corrective Action
3. Metallurgical effect of welding. 3. When welding 18/8 austenitic stainless
steel, be sure the analysis of the steel
and the welding procedure are correct,
so that welding does not cause carbide
precipitations. This condition can be
corrected by annealing at 1900°F -
2100°F.
4. Improper cleaning of a weld 4. Certain materials such as aluminium
require careful cleaning of all slag to
prevent corrosion.
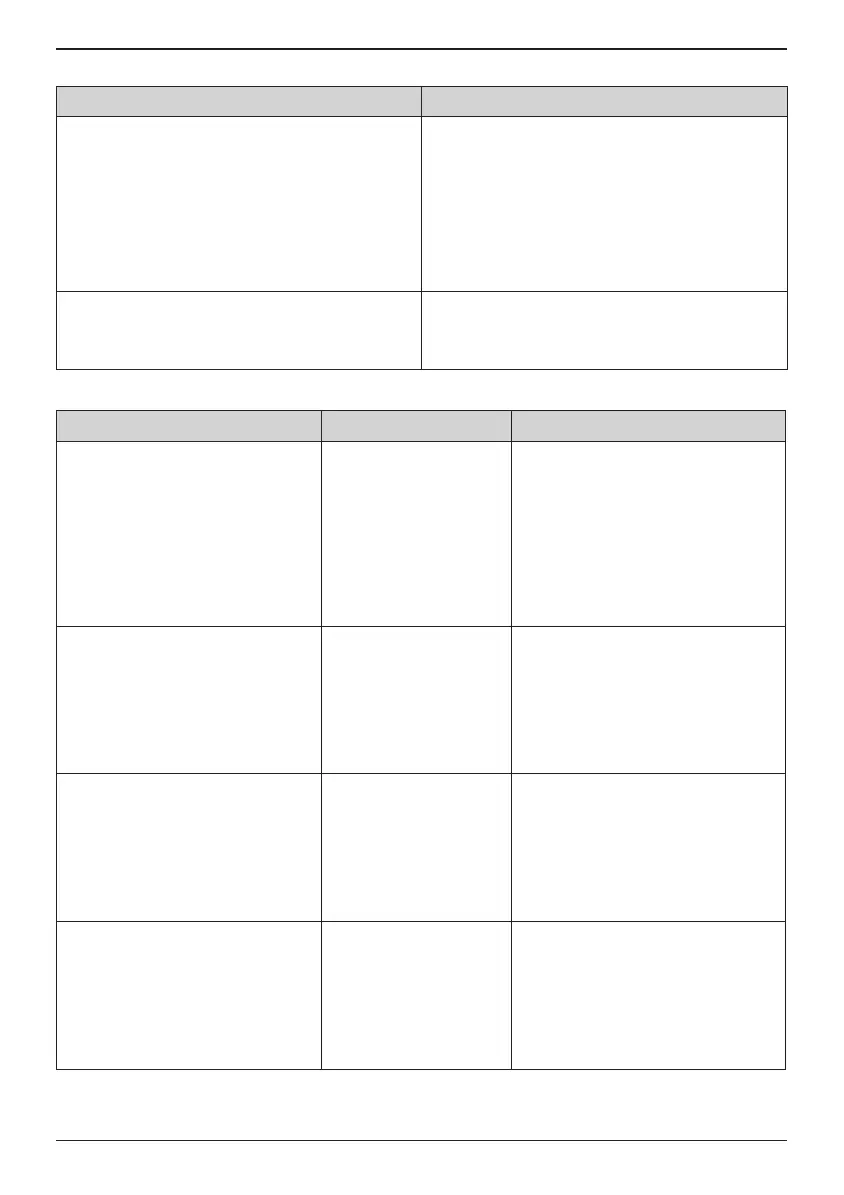
FLUXES
Flux and Use Application Removal
ALUMINIUM: Fusion welding
of sheet and cast aluminium,
weldable aluminium, and
weldable aluminium alloys.
Dip heated rod into flux
and apply to job.
1. Dilute nitric acid dip,
Followed by:
a.) Cold rinse and then a hot
rinse.
b.) Wire brush and hot water or
steam.
ALUMINIUM BRAZING: Brazing
sheet tube, plate and structural
shapes in aluminium and
aluminium alloys.
Apply paste to job and
rod.
1. Grinding wheel or wire brush
and water.
2. Sandblast.
3. Diluted hydrochloric or nitric
acid dip.*
BRONZE: Braze welding and Re-
surfacing of cast iron.
Dip heated rod into flux
and apply to job.
1. Grinding wheel or wire brush
and water.
2. Sandblast.
3. Diluted hydrochloric or nitric
acid dip.*
BRONZE TINNING: Used in
association with bronze flux for
tinning dirty cast iron.
Dip heated rod into flux
and apply to job.
1. Grinding wheel or wire brush
and water.
2. Sandblast.
3. Diluted hydrochloric or nitric
acid dip.*
Welding Procedures


 To Next Page
 Loading...