APPENDIX C: SYSTEM TIMING
IS-300CA INVERTER POWER SUPPLY
C-2 990-418
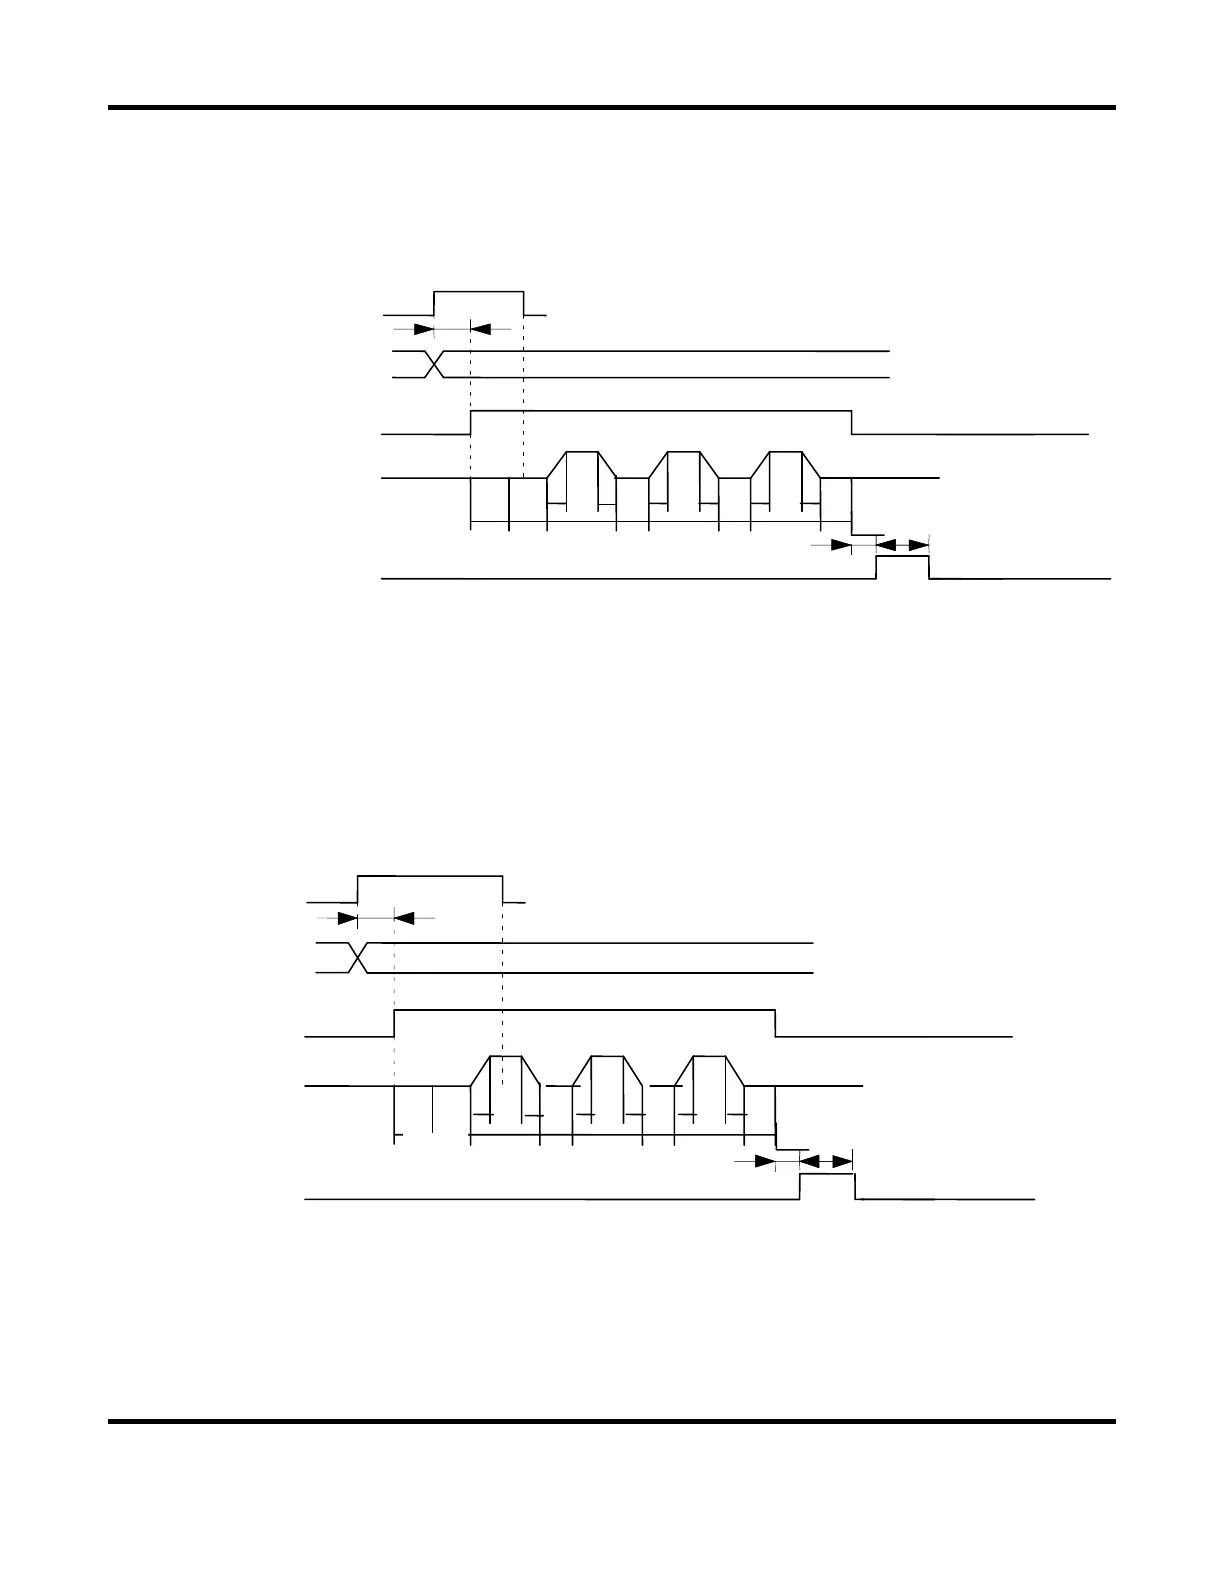
Pulsed Mode
When the 2ND STAGE signal is input for more than the time set through DELAY START SET and then
stops, the welding sequence will proceed to completion.
A
(1,2,4,8,16
32,64,128,P)
B
C
Schedule
selection
Weldin
sequence
B: Monitored value
ud
ment
time
C: END si
nal output
time
END si
nal output
Valve output
(SOL1 or SOL2)
2ND STAGE
A: DELAY START SET
SQD SQZ
UU
D
D
WE1 WE2
U
D
HOCO1
CO2
WE3
Start Signal Input in Pulsed Mode
Latched Mode
The welding sequence halts if the 2ND STAGE signal stops during squeeze time (SQZ).
The welding sequence proceeds to completion when the 2ND STAGE signal stops during Weld
1 time (WE1) or later.
A
2ND STAGE
A: DELAY START SET
Schedule
selection
(1,2,4,8,16
32,64,128,P)
SQD
Welding sequence
SQZ
U U
D
D
WE1 WE2
U
D
HOCO1
CO2
WE3
B: Monitored value judgment
time
B
C
C: END signal output
time
END signal output
Valve output
(SOL1 or SOL2)
Start Signal Input in Latched Mode


 To Next Page
 Loading...
