Page 30
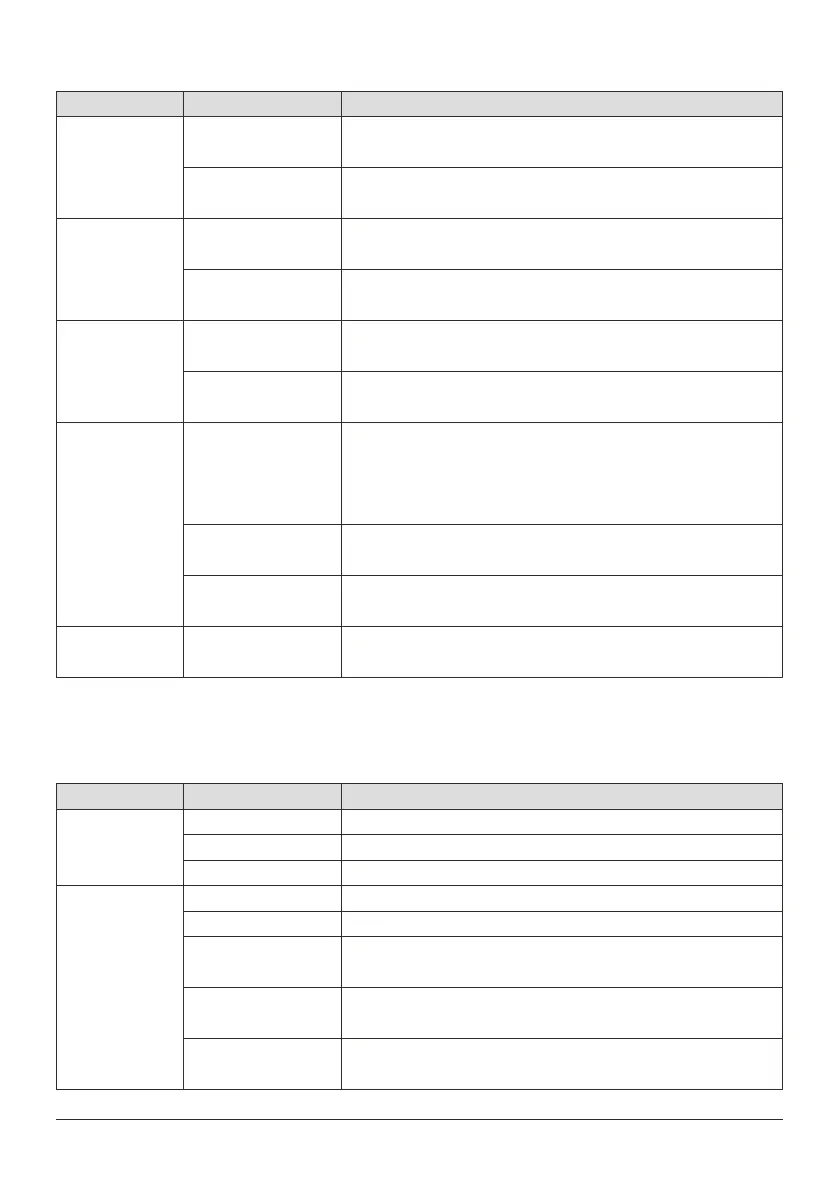
STICK WELD TROUBLESHOOTING
Electrode
Sticking
PROBLEM CAUSE CORRECTION
Arc Too Short
Current Too Low
Holes in
Weld Bead
(Porosity)
Arc Too Long
While welding, keep the ignited end of the electrode closer
to the weld joint.
While welding, keep the ignited end of the electrode further
from the weld joint.
Adjust the current on the front of the Welder to a higher
current setting.
Replace electrode with a new one.
Moisture in
Electrode
Clean the weld joint of any dirt, grease, paint of other
possible contaminates. If the pieces being Welder are of a
heavy gauge it may be necessary to bevel the edges of the
pieces.
Slow down the travel speed of the electrode while welding.
Allow the Welder to cool for a minimum of 15 minutes
before attempting to use again.
Poor Joint
Preparation
Travel Speed
Too Fast
Duty Cycle
Exceeded
Poor
Penetration
Arc Too Long
While welding, keep the ignited end of the electrode closer
to the weld joint.
Current Too Low
Adjust the current on the front of the welder to a higher
current setting.
Current Too High
Adjust the current on the front of the welder to a lower
current setting.
Excessive
Spatter
Overload Light
On
MIG WELD TROUBLESHOOTING
Burn Through
Lack of Tack Welds
PROBLEM CAUSE CORRECTION
High Voltage
Slow Gun Travel
Adjust voltage output to lower setting.
Adjust wire speed to slower setting.
Increase your travel speed with the Welding Gun.
Lack of
Penetration
Slow Wire Speed
Low Voltage
Fast Gun Travel
Adjust voltage output to higher setting.
Adjust wire speed to faster setting.
Slow your travel speed of the Welding Gun making sure to
pull or drag the molten metal puddle.
Move the Contact Tip on the Welding Gun closer to the
work piece to shorten the length of exposed wire.
The MIG-2500 is rated for a maximum thickness of 3/8'',
exceeding this will result in poor penetration.
Excessive Wire
Protruding
Material Too Thick


 To Next Page