Page 31
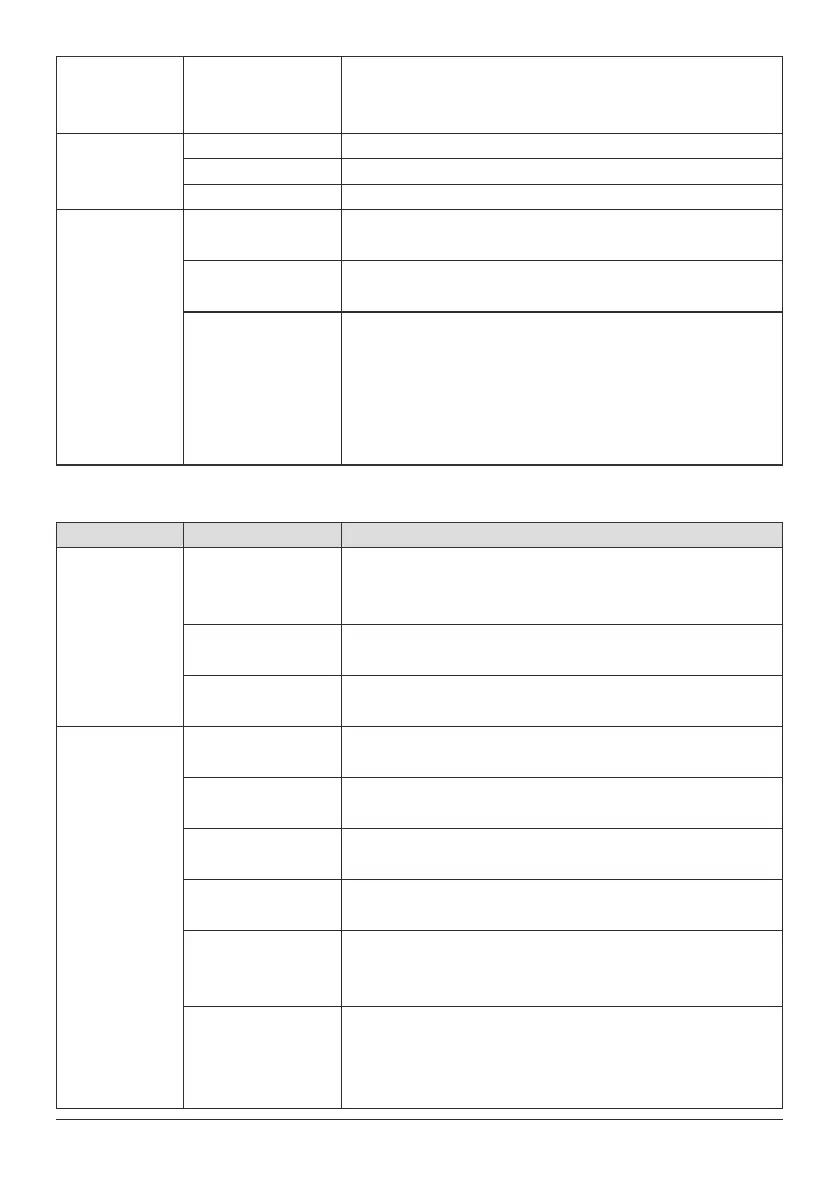
If welding heavy gauge metals, it is necessary to increase
the welding gap between the two pieces and also bevel the
edges on the weld side of the pieces.
Adjust voltage output to lower setting.
Adjust wire speed to slower setting.
Increase your travel speed with the Welding Gun.
Tack weld the pieces in multiple areas to keep the pieces
from pulling apart.
Use welding clamps to secure the pieces in the proper
shape.
To prevent warping, allow the workpiece to cool after
welding small sections at a time. Move your welding areas
around by not completing all the welding in one section all
at once, rather, welding a small amount in one area and
then move to another section area to spread out the heat
in the piece.
Poor Material Prep
High Voltage
Fast Wire Speed
Slow Gun Travel
Lack of Tack Welds
No Clamping
Poor Technique
Excessive
Penetration
Warping
TIG WELDING TROUBLESHOOTING
Arc is
Triggered but
Will Not Start
PROBLEM CAUSE CORRECTION
Incomplete Circuit
Incorrect Tungsten
No Shielding Gas
Make sure the shielding gas cylinder is turned all the way
open and set at the correct flow rate.
Adjust the flow rate of the shielding gas (refer to settings
chart). Check for loose fittings where gas could be leaking.
Poor Gas Flow
Check Ground connection. Make sure that the ground is on
a freshly cleaned surface and close to the welding area. It
is suggested to weld towards the ground connection.
Consult chart for proper Tungsten for the base metal being
welded. In most cases Thoriated will be used for all steels.
Follow guidelines for prepping Tungsten.
Poorly Prepped
Tungsten
Remove Tungsten from Torch, break off contaminated
section, and resharpen.
Contaminated
Tungsten
Make sure the Tungsten is held 1/8 to 1/4 inch off the work
piece.
Incorrect Arc Length
Incomplete Circuit
Check Ground connection. Make sure that the ground is on
a freshly cleaned surface and close to the welding area. It
is suggested to weld towards the ground connection.
Contaminated
Base Metal
Clean base metal making sure to remove any oil, debris,
coatings, or moisture. If base metal is aluminum make sure
all of the oxide is removed using either a dedicated
stainless brush or flap wheel.
Arc wanders
and it is Hard
to Concentrate
Heat in a
Specific Area


 To Next Page