Page 32
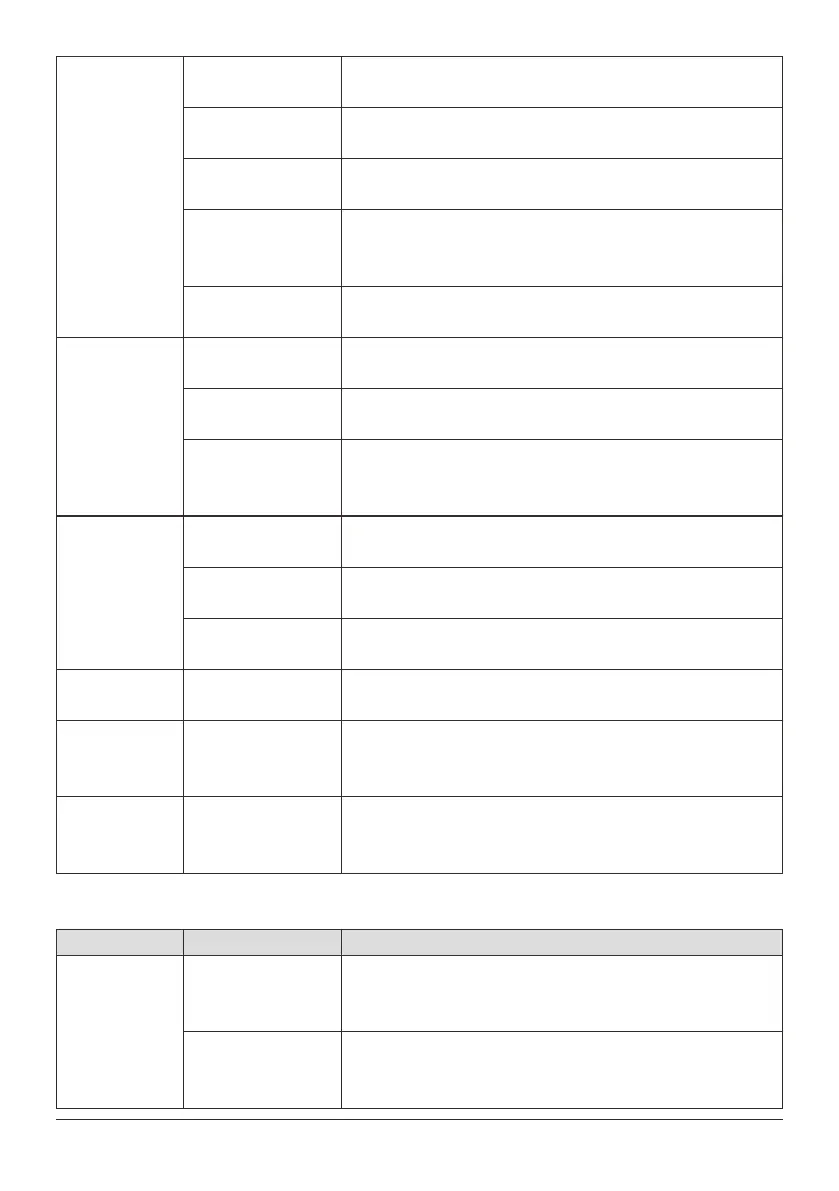
Adjust the flow rate of the shielding gas. Check for loose
fittings where gas could be leaking.
Poor Gas Flow
Clean filler metal making sure to remove any oil, debris, or
moisture.
Contaminated
Filler Metal
Contaminated
Base Metal
Make sure to be in an area with no wind and with any fans
turned off. Wind or fans will blow the shielding gas away
from the weld causing porosity.
Adjust the Tungsten so that 1/8" to ¼" inch protrudes from
the Collet.
Poor Shielding
Remove Tungsten from Torch and break off contaminated
section and resharpen.
Clean filler metal making sure to remove any oil, debris, or
moisture.
Contamination
Tungsten
Contaminated
Filler Metal
Clean base metal making sure to remove any oil, debris,
coatings, or moisture. If base metal is cold rolled steel,
make sure to remove any mill scale.
Adjust the flow rate of the shielding gas. Check for loose
fittings where gas could be leaking.
Contaminated
Base Metal
Increase Tungsten diameter. Refer to chart for proper
sizing.
Poor Gas Flow
Only use 100% Argon when TIG Welding.
Wrong Size
Tungsten
Voltage setting is too low for material/thickness. Increase
as needed.
Incorrect
Shielding Gas
Low Voltage
Keep Tungsten 1/8 to 1/4 inch from the base metal. If
Tungsten comes in contact break off end and resharpen
immediately.
Contact of Tungsten
with Base Metal
The angle between the filler metal and the Torch must be
less than 90 degrees otherwise the filler metal will
prematurely melt and glob off causing poor weld
Clean base metal making sure to remove any oil, debris,
coatings, or moisture.
Contaminated
Filler Metal
Incorrect
Positioning
Porosity in
Weld Bead
Contamination
in Weld Bead
Melting
Tungsten
Poor
Penetration
Tungsten
Contaminated
Poor Weld
Appearance
TIG WELDING TROUBLESHOOTING
Crater in the
End of the
Weld Bead
PROBLEM CAUSE CORRECTION
Insufficient
Shielding
Keep the Torch on the base metal while the post flow
shielding gas flows to protect and cool the metal and
Tungsten.
Not Enough
Filler Material
Reduce current and add more filler at end of weld. It may
also be beneficial to back step to ensure no crater will
form.


 To Next Page