Oper ions
L IWARNING
-
•
Follow
all
the
information
in
the
your
Mark
V
and
Lathe
Duplicator
instruction
manuals
when
you
!.!!~e
the
Steady
Rest
•
Do
not
mount
the
Steady
Rest
to
the
chanooluntil
after
the
spindle
stock
has
already
been
rounded.
•
The
lathe
turning
speed
must
be
set
at
"Slow"
before
po-
sitioning
th~
Steady
Rest
bearings
against
the
stock.
•
When
turning
thin
spindle
stock,
do
not
place
the
Steady
Rest
00
that
the
support
bearings
press
against
and
bend
the
stock.
!f
the
stock
is
bent,
it
could
snap
and
be
thrown
from
the
lathe.
Also,
if
the
stock
is
bent,
the
final
profile
of
the
spindle
will
be
reduced
in
diameter.
•
Remove
the
Steady
Rest
form
the
channel
before
you
start
to
tum
additional
spindles.
•
Before
sanding
the
spindle
on
the
lathe,
remove
from
the
Mark
V
the
Lathe
Duplicator
with
the
Steady
Rest
channel
attached.
o
Maximum
diameter
of
a
spindle
used
with
the
Steady
Rest
-
is
3-1/2".
Follow
these instructions each time
you
use the Steady Rest with the Lathe Du-
plicate";
1. Prepare the
spindle
stock
according
to the
lathe
Duplicator instruction manual.
Round
the
stock into a cylinder. Shape the largest diameter pro-
file nearest the center of the stock. The largest diam-
eter profile
must
be
as
smooth
as possible because
this is
where
the bearings will contact the spindle.
Any
rough
spots
will
cause
the
stock
to
vibrate
against
the
Steady Rest
and
will affect the quality
of
the
cut.
2.
Turn
the
Mark V speed
to
"Slow."
Then
tum
off
and
unplug
the
Mark
V.
3.
Install
the
Steady Rest on its channel (1). Po-
sition
the
Steady Rest's bearings
at
the
turned pro-
file
on
the stock, then
use
a 5/16" Allen wrenc'1 to
tighten
down
the bracket
(8)
in
the
Chan.llel,
as illus-
trated
in
Fig.
8.
-
Fig. 8
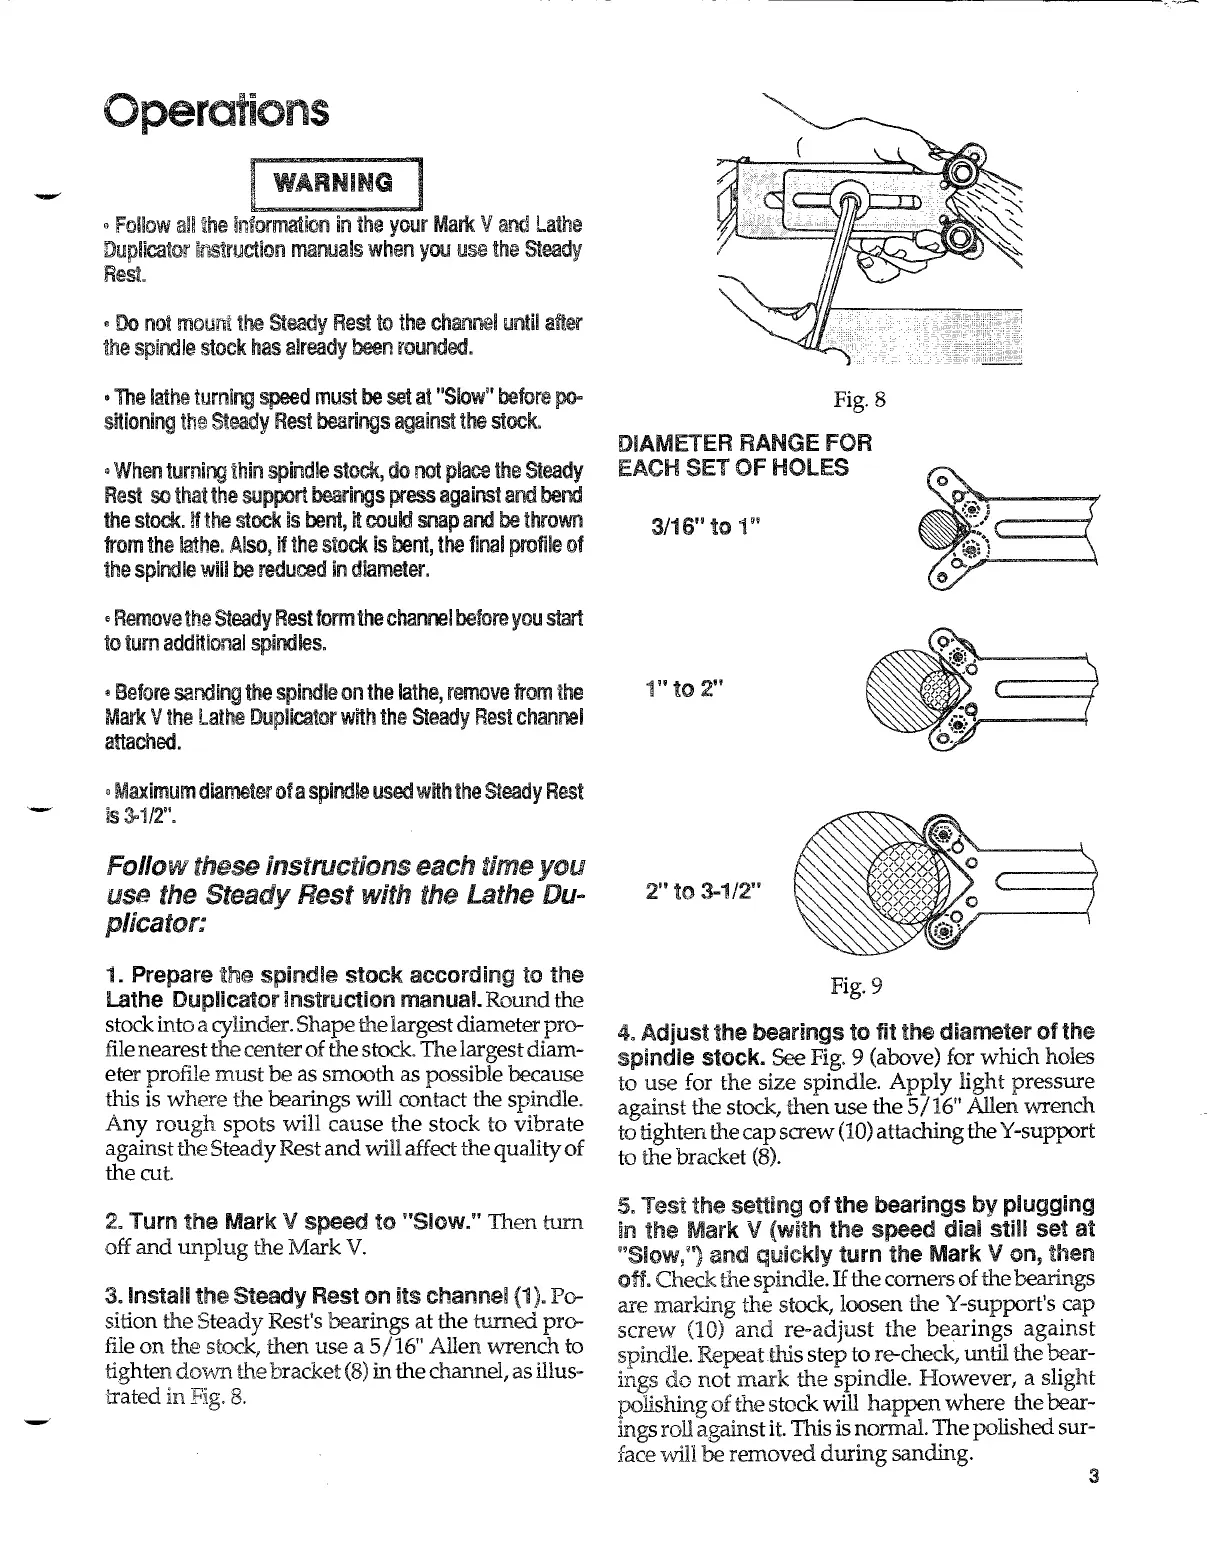
DIAMETER RANGE FOR
EACH SET
OF
HOLES
3/16"
to
1"
1"
to
2"
2" to 3-1/2"
Fig. 9
4.
Adjust the bearings
to
fit
the diameter
of
the
spindle stock. See Fig.
9 (above) for which holes
to
use
for
the
size spindle.
Apply
light
pressure
against the stock,
then
use
the
5/16" Allen wrench
to tighten the cap screw
(10) attaching the Y-support
to the bracket
(8).
5.
Test the setting
of
the
bearings
by
plugging
in the Mark V (with the speed dial still set at
"Slow,") and
quickly
turn the Mark V on,
t~en
off. Check the spindle.
If
the
comers of the
beanngs
are marking
the
stock, loosen
the
Y-~upport's
.cap
screw
(0)
and
re-adjust
the
bearmgs
agamst
spindle.
RepeatfrJs
step
t?
re-check, until the
~ar
ings
do
not
mark
the
spmdle.
However,
a slIght
polishing
of
the stock
will
happen
where.
the
bear-
ings roll against
it. This is normal. The polished sur-
face will
be
removed
during
sanding.
3


 To Next Page
 Loading...