®
Specialty Systems - Melt-Disk
Not under documentation control if printed. May be revised without notice. ©05-2014
Electronic version is available at www.moldmasters.com
Hot Runner User Manual Revision 18
14-7
WARNING
When the mold is open never inject mate-
rial through hot runner system under high
pressure. Failure to do so can result in
serious injury or death.
Shut Down
NOTE
For horizontal tips, refer to the controller
operating manual.
1. Maximize decompression stroke prior to shut
down. This will minimize drool at start up when
there is limited gate cooling.
2. Reduce nozzle temperatures to 150°C (300°F).
3. Reduce Melt-Disk temperatures to 150°C (300°F).
4. Turn off all zones.
NOTE
Thermally sensitive materials should be
purged from the hot runner system prior to
shut down using a thermally stable mate-
rial with a similar processing temperature.
For example, a system running PVC
should be initially started and subsequent-
ly shut down on LDPE.
Melt-Disk System Start Up &
Shut Down
Also refer to Section 8 System Start Up & Shut
Down and the controller manual.
Start Up
NOTE
When running thermally sensitive materi-
als, use a thermally stable material as
recomended by the material supplier for
the initial start up.
1. Turn on the machine barrel and mold cooling
system.
2. Prior to start up, ensure the:
• Machine barrel is up to processing tempera-
ture.
• Mold cooling is on and at cooling temperature.
3. Heat manifold zones and Inlet to processing tem-
perature.
4. Heat Melt-Disks to processing temperature.
5. Heat nozzles to processing temperature. A small
amount of material may weep at this stage.
6. Allow to heat soak at least 10 minutes.
7. Fill system under low pressure extrude (using
screw rotation).
8. Set Melt-Disk temperature at least 6°C (10°F)
lower than nozzles.
NOTE
For hot runner systems using heater
plates, allow 10 minutes of soak time after
the system reaches processing tempera-
ture.
CAUTION
Failure to follow the above procedure may
result in leakage/damage occurring in the
hot runner.
CAUTION
Disassembly for Maintenance
NOTE
Before shutting down the molding machine
and mold, use maximum screw decom-
pression to remove as much molten plastic
from the hot runner system as possible.
1. Disassemble mold to expose the Melt-Disk. Plate/
insert removal to be done with all components in
the cold condition.
2. Melt-Disks should be heated to 120 - 138°C (250
- 280ºF) before removal. The Melt-Disk should
be removed as soon as it reaches set-point. The
EXTOOLAS01 can be used to assist with the
Melt-Disk removal.
Melt-Disk Reassembly after
Maintenance
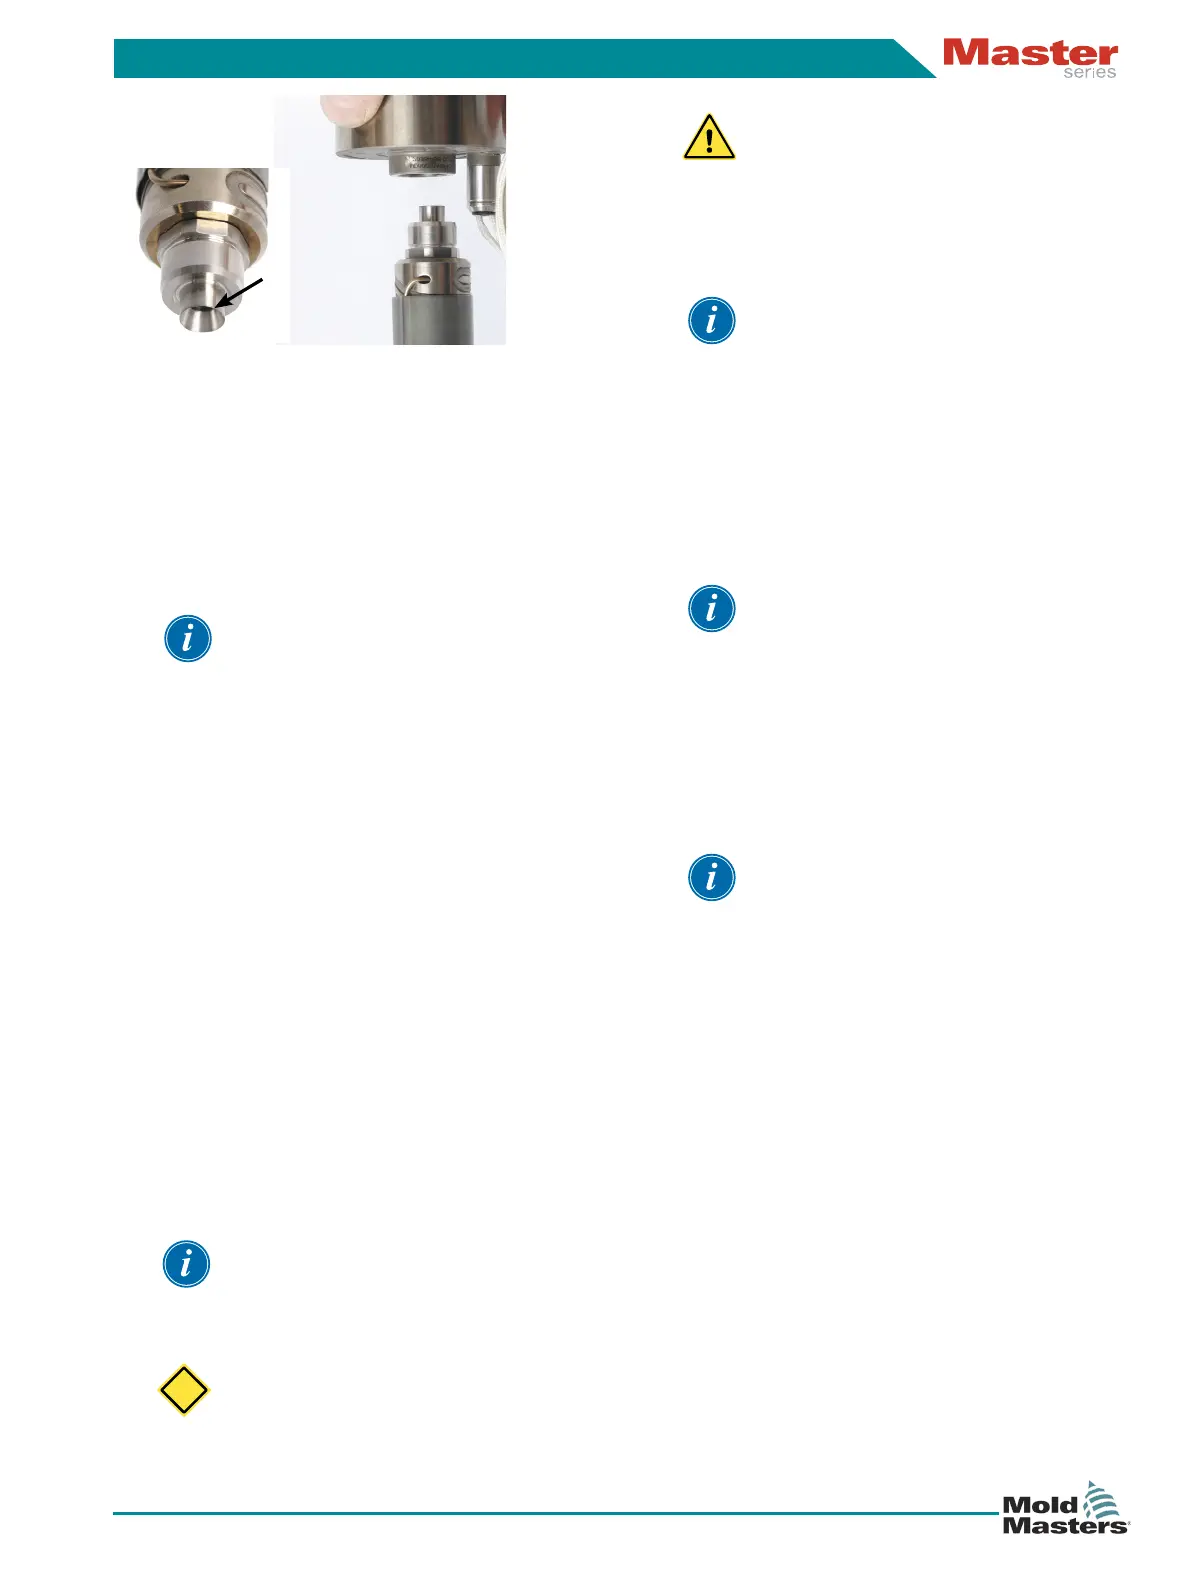
1. All sealing surfaces are to be clean and inspected
for defects.
2. The inside bore of the Melt-Disk is to be free of
material so that when it is installed to the Melt link,
there is no interference.
3. The Melt-Disk is to be installed cold onto a cold
Melt link.
Figure 14-20
Do not
damage
sharp edge


 To Next Page