EasyManua.ls Logo

Okuma OSP-U100M - NC Optional Parameter (Long Word)

Okuma OSP-U100M
511 pages
Print Icon
To Next Page IconTo Next Page
To Previous Page IconTo Previous Page
Loading...
4203-E
P-371
SECTION
3
DESCRIPTION
OF
PARAMETER
AND
SETTING
PROCEDURE
5.
NC
Optional
Parameter
(Long
Word)
For
optional
parameter
(long
word),
those
listed
below
are
available.
The
parameter
numbers
given
in
the
following
table
are
keyed
to
the
numbers
displayed
on
the
OPTIONAL
PARAMETER
(LONG
WORD)
screen.
Parameter
Initial
Setting
Value
Setting
Range
Item
Contents
No.
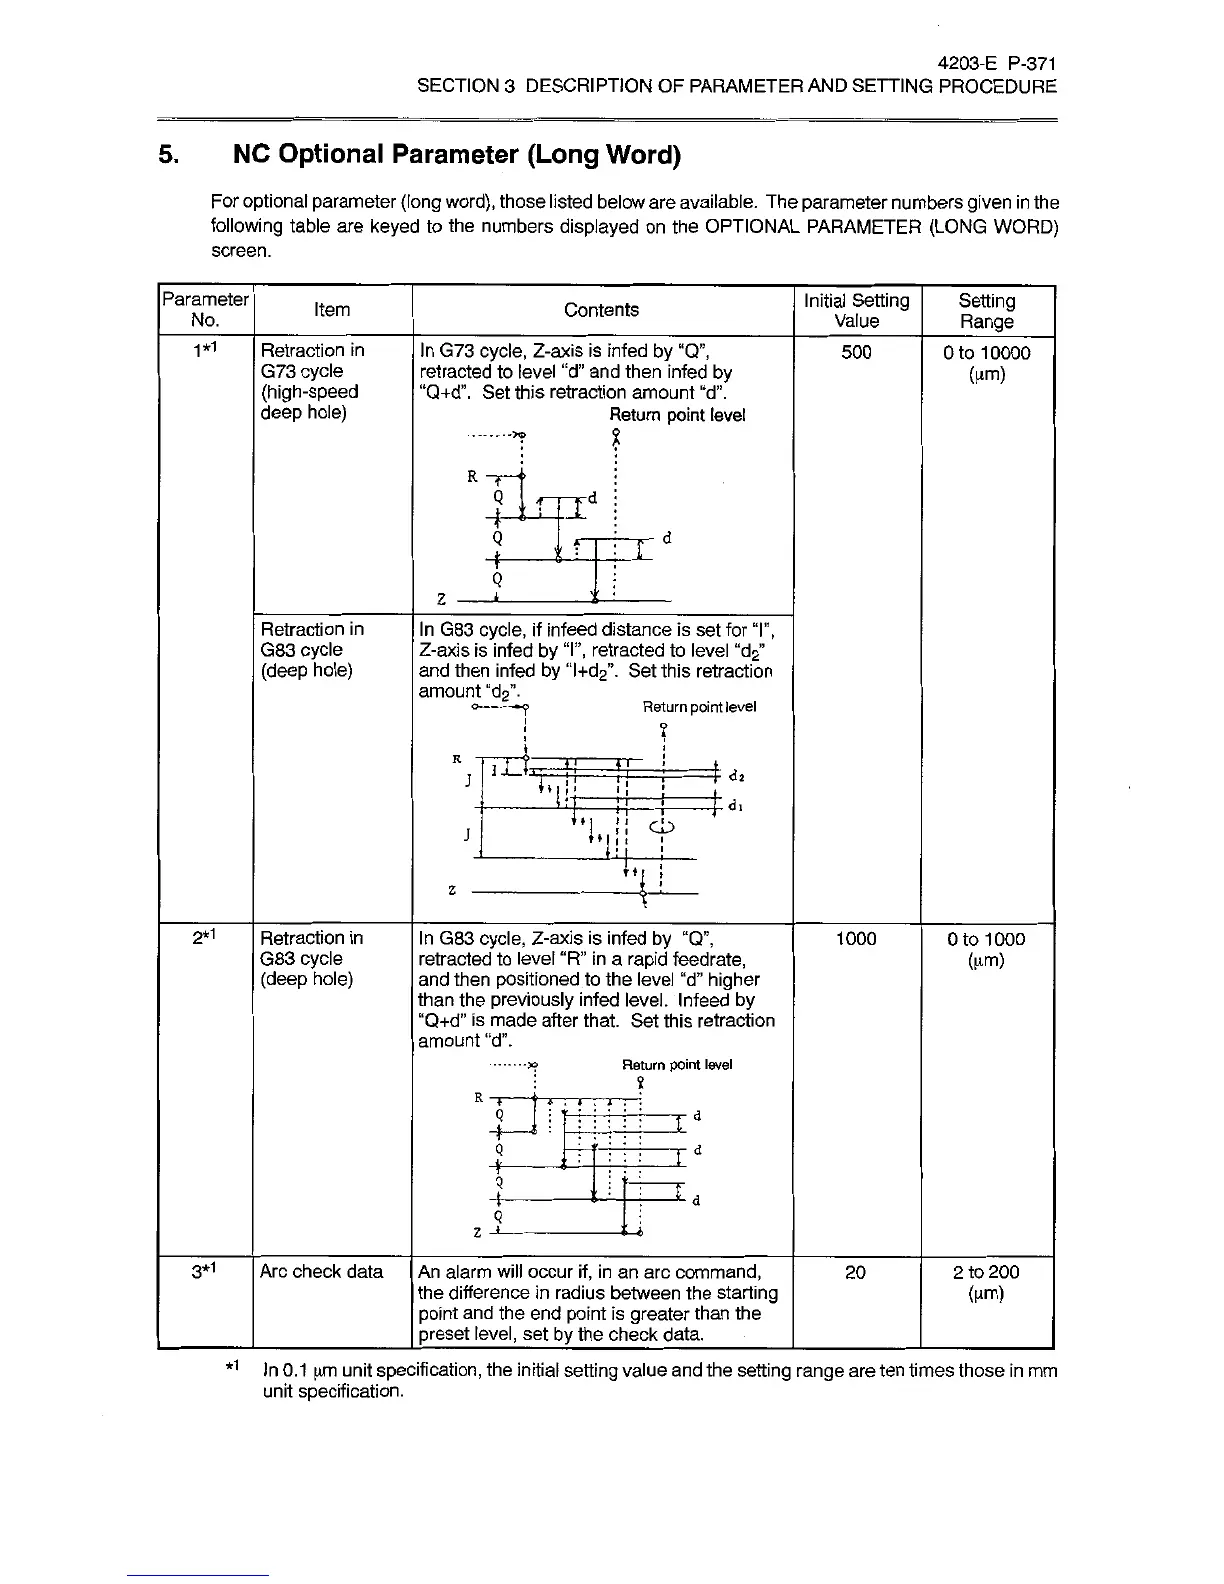
1*1
Retraction
in
G73
cycle
(high-speed
deep
hole)
In
G73
cycle,
Z-axis
is
infed
by
“Q”,
retracted
to
level
“d”
and
then
infed
by
“Q+d”.
Set
this
retraction
amount
“d”.
Return
point
level
500
Oto
10000
(ixm)
%
:
'Jh
•d
Q
r
d
f
f
Q
z
Retraction
in
G83
cycle
(deep
hole)
In
G83
cycle,
if
infeed
distance
is
set
for
“I”,
Z-axis
is
infed
by
“I”,
retracted
to
level
“d2”
and
then
infed
by
“l+d2”.
Set
this
retraction
amount
“d2”.
o.
—
Return
point
level
?
i
R
TO
£
di
m
"ii
J
di
M
c
'o
J
z
T
2*1
Retraction
in
G83
cycle
(deep
hole)
In
G83
cycle,
Z-axis
is
infed
by
“Q”,
retracted
to
level
“R”
in
a
rapid
feedrate,
and
then
positioned
to
the
level
“d”
higher
than
the
previously
infed
level.
Infeed
by
“Q+d”
is
made
after
that.
Set
this
retraction
amount
“d”.
1000
Oto
1000
(|UTl)
Return
point
level
1
?
r
T
Id
Id
Q
Id
1
z
-i
3*1
Arc
check
data
An
alarm
will
occur
if,
in
an
arc
command,
the
difference
in
radius
between
the
starting
point
and
the
end
point
is
greater
than
the
preset
level,
set
by
the
check
data.
_
20
2
to
200
(pm)
*1
In
0.1
pm
unit
specification,
the
initial
setting
value
and
the
setting
range
are
ten
times
those
in
mm
unit
specification.