E - Manual MIG Welding(Free Setting on Voltage and Wire feed Speed(Welding Amp will
automatically fitting with Wire Feed Speed)
Note: Gasless Flux Mig is only available for .035'' Wire Diameter, can weld with no Gas.
M MI G- Ma n ua l s et t in g V ol t ag e /W ire F e ed Sp e ed o n C arb on St e el / St ai n le s s
Steel(.023/.030/.035'')(Recommend .030/.035'') And Aluminum Steel(.035/.045'')
(Available for Professional Welder Only)
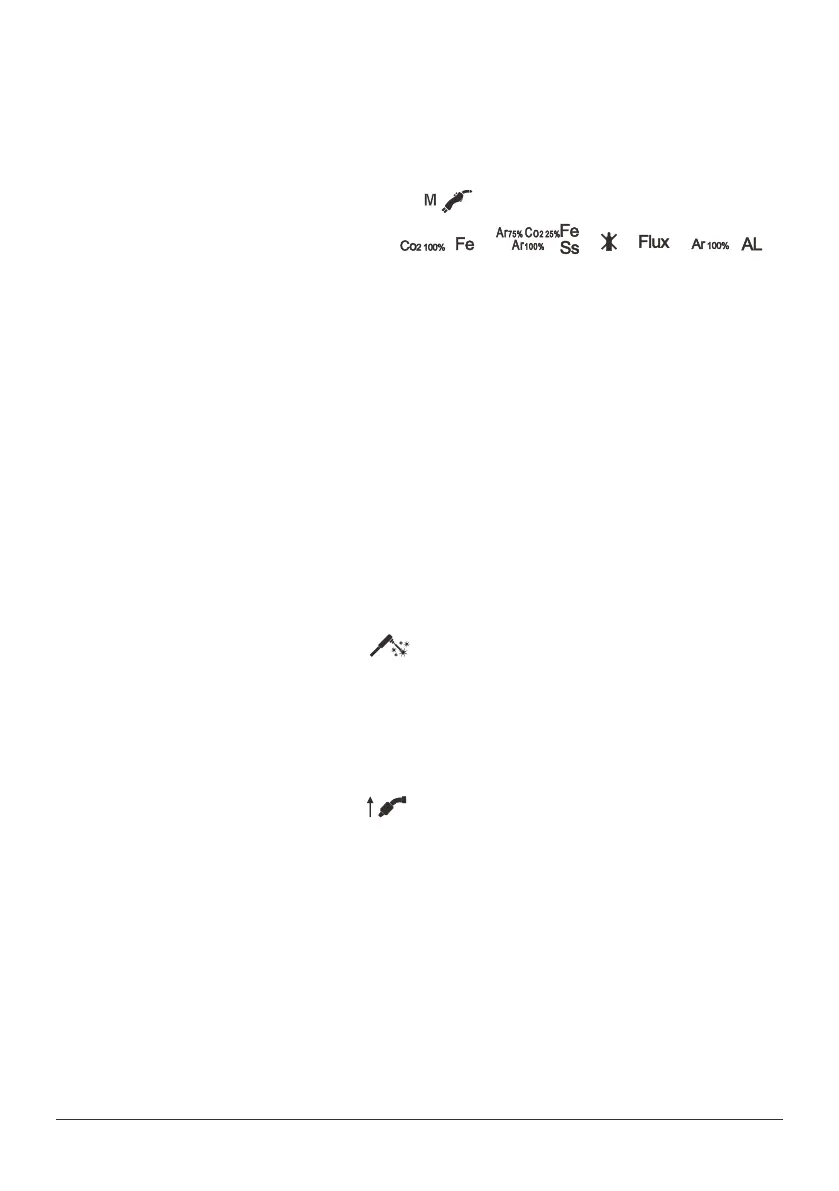
Set the MODE button on front panel to M MIG( ),(user set the welding ampere, the voltage
and wire feed speed seperately
Set the MATERIAL button on front panel to / / /
Set the WIRE button on front panel to .023,.030 or .035''-Carbon Or Stainless Steel;
.035 or .045''-Aluminum and Steel refer to the wire used in machine.
Make sure the V type roller used and Steel liner of torch used for Carbon or Stainless Steel
Welding.
the U type roller used and Teflon liner of torch used for Aluminum and Steel welding.
Adjust MENU knob, set the welding ampere according to welding chart.
Set the V button on front panel, change the value of Voltage(12.5-30V) and Wire feed speed(2-15
m/Min).
Press the MENU button enter specifications of MIG, 2T/4T(2steps or 4steps of welding)
Set the value of IND(inductance),HS(Hot start) and BBT (Burn Back Time).(Recommended to use
Default Value)
Remove the tips, press and hold INCHING button, till the wire come out of torch neck.
Fasten the tips according to correct wire diameter(.023 0.6mm/.030 0.8mm/.035 0.9mm) and
Nozzle.(Carbon Steel and Stainless Steel Weld)
Fasten the Marked ‘A’(Aluminum)tips according to correct wire diameter(.035'' 0.9mm/.045''
1.2mm) and Nozzle.(Aluminum and Steel Weld)
F - Stick Welding
Set the MODE button on front panel to , and adjust MENU knob to set the welding ampere
according to welding chart.
Press the MENU button to enter specifications of MMA, DIG(Arc Force Current ,easier for arc
starting on thick work piece), HS(Hot Start Time-easier for start arc on cellulose electrode), VRD
ON/OFF(Voltage Reduce Function for avoid leakage of voltage in humid environment), ANT
ON/OFF(Anti-stick function on/off)
G - Lift Tig Welding
Set the MODE button on front panel to , Setup the Lift tig torch(Not included).
Page 07


 To Next Page