EasyManua.ls Logo

Okuma OSP-U100M - Page 197

Okuma OSP-U100M
511 pages
Print Icon
To Next Page IconTo Next Page
To Previous Page IconTo Previous Page
Loading...
4203-E
P-176
SECTION
1
DATA
SETTING
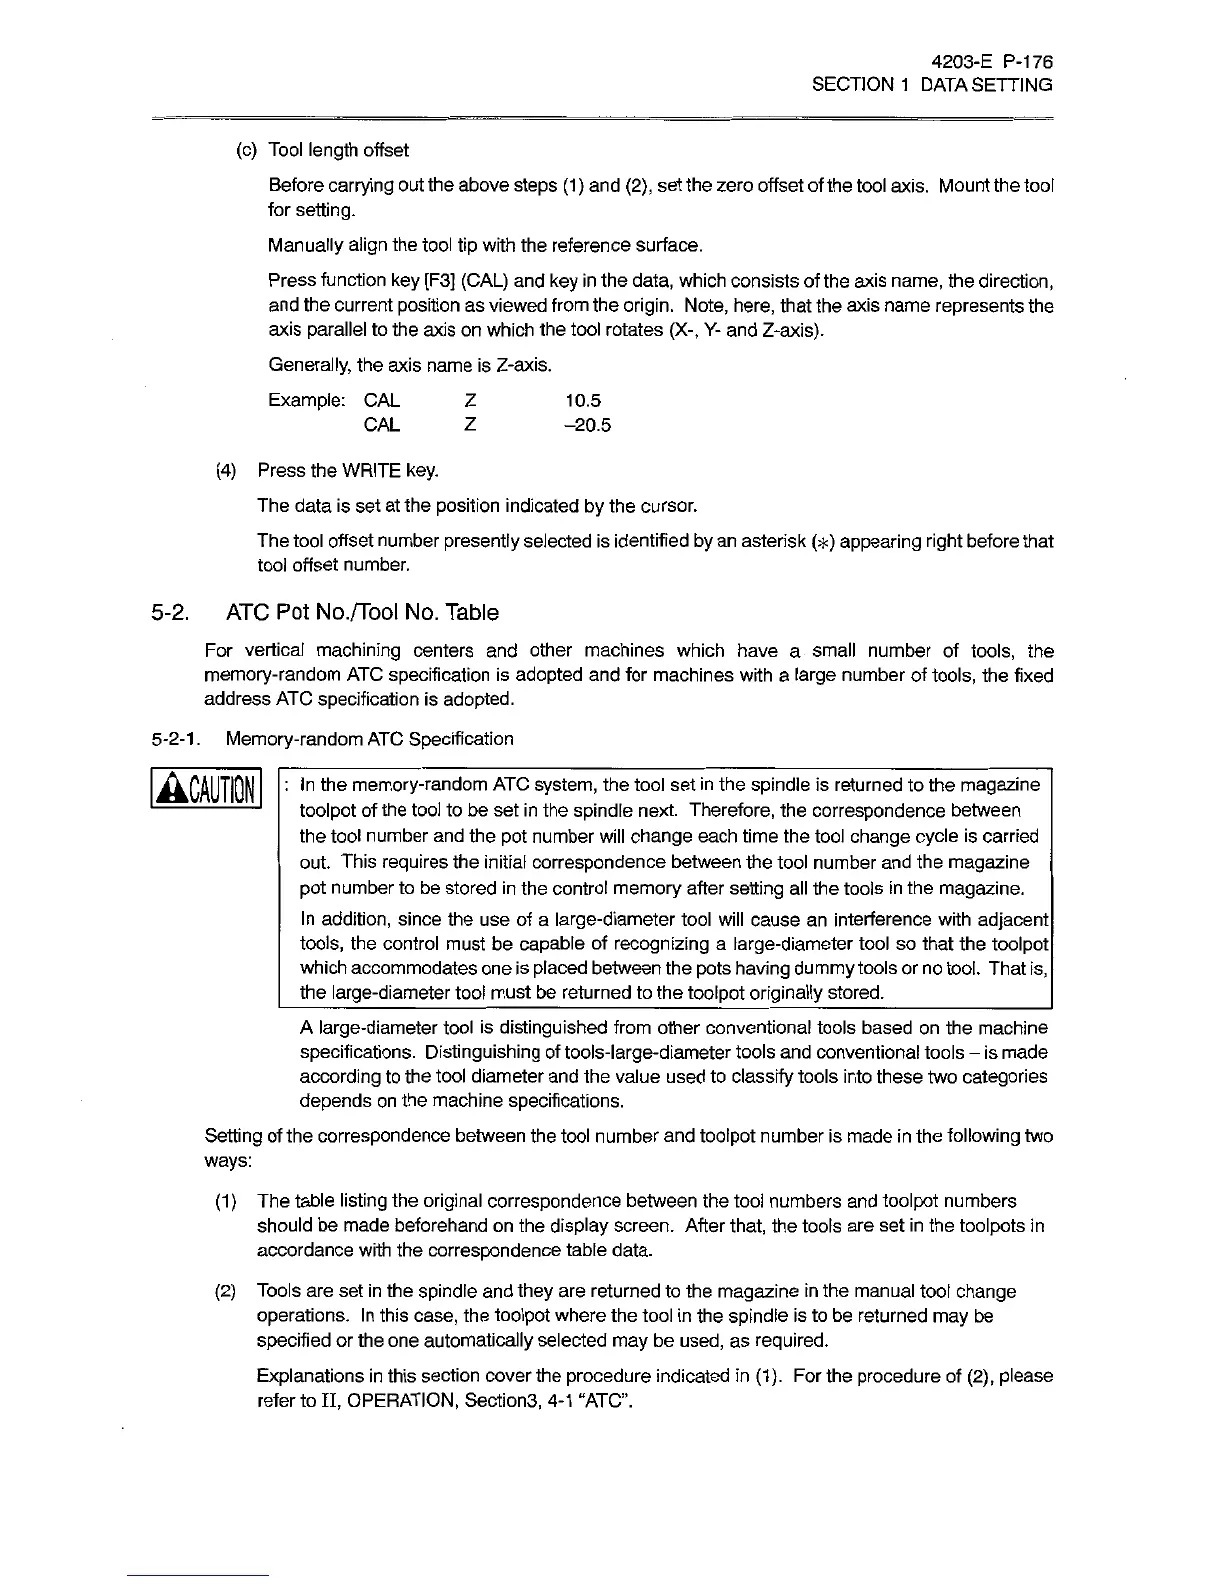
(c)
Tool
length
offset
Before
carrying
out
the
above
steps
(1)
and
(2),
set
the
zero
offset
of
the
tool
axis.
Mount
the
tool
for
setting.
Manually
align
the
tool
tip
with
the
reference
surface.
Press
function
key
[F3]
(CAL)
and
key
in
the
data,
which
consists
of
the
axis
name,
the
direction,
and
the
current
position
as
viewed
from
the
origin.
Note,
here,
that
the
axis
name
represents
the
axis
parallel
to
the
axis
on
which
the
tool
rotates
(X-,
Y-
and
Z-axis).
Generally,
the
axis
name
is
Z-axis.
Example:
CAL
Z
10.5
CAL
Z
-20.5
(4)
Press
the
WRITE
key.
The
data
is
set
at
the
position
indicated
by
the
cursor.
The
tool
offset
number
presently
selected
is
identified
by
an
asterisk
(*)
appearing
right
before
that
tool
offset
number.
5-2.
ATC
Pot
No./Tool
No.
Table
For
vertical
machining
centers
and
other
machines
which
have
a
small
number
of
tools,
the
memory-random
ATC
specification
is
adopted
and
for
machines
with
a
large
number
of
tools,
the
fixed
address
ATC
specification
is
adopted.
5-2-1
.
Memory-random
ATC
Specification
;
In
the
memory-random
ATC
system,
the
tool
set
in
the
spindle
is
returned
to
the
magazine
toolpot
of
the
tool
to
be
set
in
the
spindle
next.
Therefore,
the
correspondence
between
the
tool
number
and
the
pot
number
will
change
each
time
the
tool
change
cycle
is
carried
out.
This
requires
the
initial
correspondence
between
the
tool
number
and
the
magazine
pot
number
to
be
stored
in
the
control
memory
after
setting
all
the
tools
in
the
magazine.
In
addition,
since
the
use
of
a
large-diameter
tool
will
cause
an
interference
with
adjacent
tools,
the
control
must
be
capable
of
recognizing
a
large-diameter
tool
so
that
the
toolpot
which
accommodates
one
is
placed
between
the
pots
having
dummy
tools
or
no
tool.
That
is,
the
large-diameter
tool
must
be
returned
to
the
toolpot
originally
stored.
A
large-diameter
tool
is
distinguished
from
other
conventional
tools
based
on
the
machine
specifications.
Distinguishing
of
tools-large-diameter
tools
and
conventional
tools
-
is
made
according
to
the
tool
diameter
and
the
value
used
to
classify
tools
into
these
two
categories
depends
on
the
machine
specifications.
Setting
of
the
correspondence
between
the
tool
number
and
toolpot
number
is
made
in
the
following
two
ways:
(1)
The
table
listing
the
original
correspondence
between
the
tool
numbers
and
toolpot
numbers
should
be
made
beforehand
on
the
display
screen.
After
that,
the
tools
are
set
in
the
toolpots
in
accordance
with
the
correspondence
table
data.
(2)
Tools
are
set
in
the
spindle
and
they
are
returned
to
the
magazine
in
the
manual
tool
change
operations.
In
this
case,
the
toolpot
where
the
tool
in
the
spindle
is
to
be
returned
may
be
specified
or
the
one
automatically
selected
may
be
used,
as
required.
Explanations
in
this
section
cover
the
procedure
indicated
in
(1).
For
the
procedure
of
(2),
please
refer
to
II,
OPERATION,
Section3,
4-1
“ATC”.