B626
B626 Page 4 840D/828D SINUMERIK Operate
Notes
Section 2
2.2 Programming example: Bevel
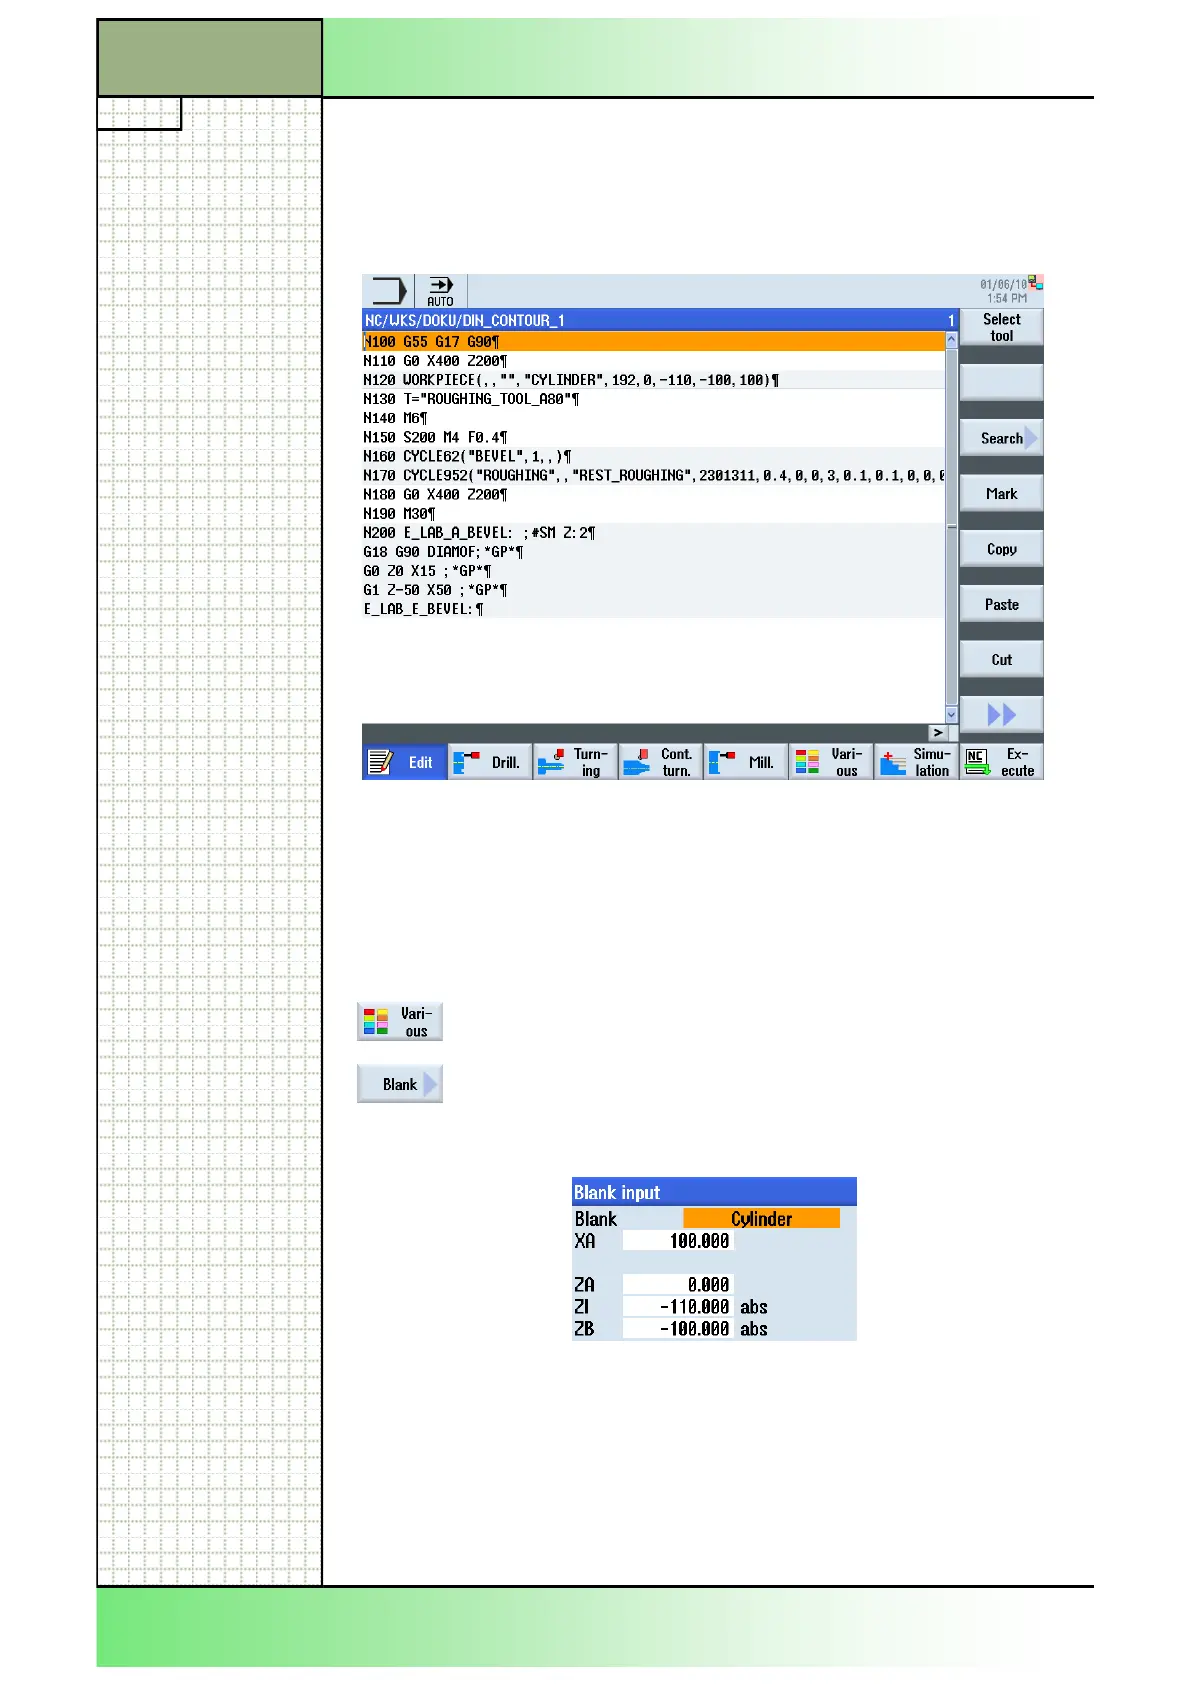
The following program with the call up of a simple stock removal cycle is to
be programmed:
1. Program now the first lines of the program:
N100 G55 G17 G90
N110 G0 X400 Z200
2. Insert a blank for the simulation into the program.
Press the HSK 1.6 “Various” to open the working
area “Various”.
Here, press the VSK 1 “Blank” to open the parame-
ter window for the blank.
3. Enter the following parameters for the blank:
Confirm your inputs by pressing the VSK 8 “Accept”.
The following program line will be inserted into the
program:
N120 WORKPIECE(,,"","CYLINDER",192,0,-110,
-100,100)
Simple programming example




 To Next Page