B626
B626 Page 10 840D/828D SINUMERIK Operate
Notes
Complex programming example
Section 3
Description:
A more complex G code program (spigot) is to be programmed using dif-
ferent turning cycles (contour, stock removal and residual cutting).
Aim:
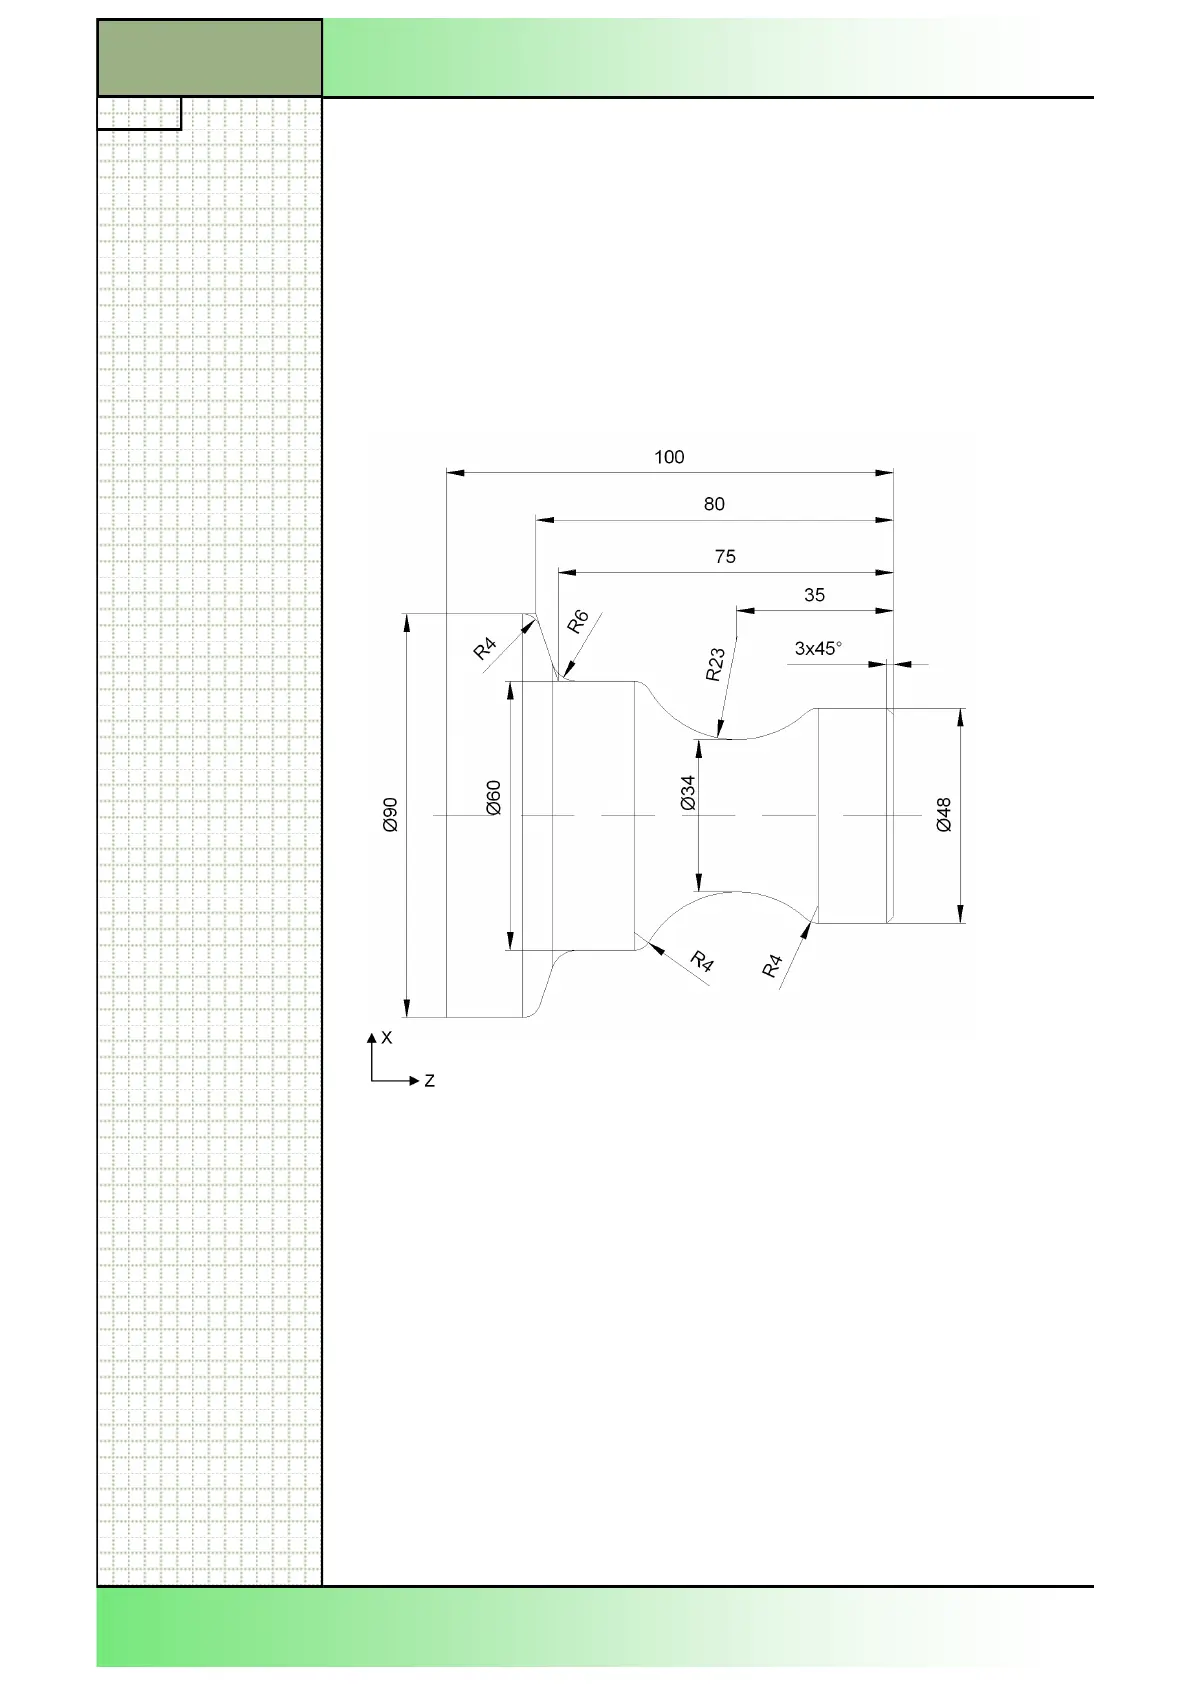
The workpiece shown below is to be programmed.
Then the program is to be simulated.
.
The following tool- and technology data are to be used:
Tool data:
Technology data:
ROUGHING_TOOL_A80
(F 0,3 mm/U, V 260 m/min)
BUTON_TOOL_8
(F 0,25 mm/U, V 240 m/min)
FINISHING_TOOL_35
(F 0,12 mm/U, 280 m/min)
Starting-up technol-
ogy:
The following position is programmed as the
contours starting point:
X 0
Z 0
This point is approached in the cycle automatically
with rapid traverse.




 To Next Page