MAINTENANCE
Regular maintenance reduces downtime
• Each time the wire bobbin is changed, the welding hose should be removed
from the Gas cylinder and machine and blown clean with compressed air.
• The wire end must not have sharp edges when it is being inserted in the Wire
Liner, especially PTFE Liner.
TIPS AND NOZZLES
• Remove the gas nozzle, spatter protector, tip adaptor and contact tip.
• Clean any spatter from the gas nozzle, tip adaptor and contact tip so that the
shielding gas can flow freely, thus eliminating the risk of a short-circuit.
• Check and replace if necessary any worn out tips and nozzles.
• Spatter protector must be replaced once its front end has worn thin.
• Select contact tip to suit wire diameter.
• Mount the fittings.
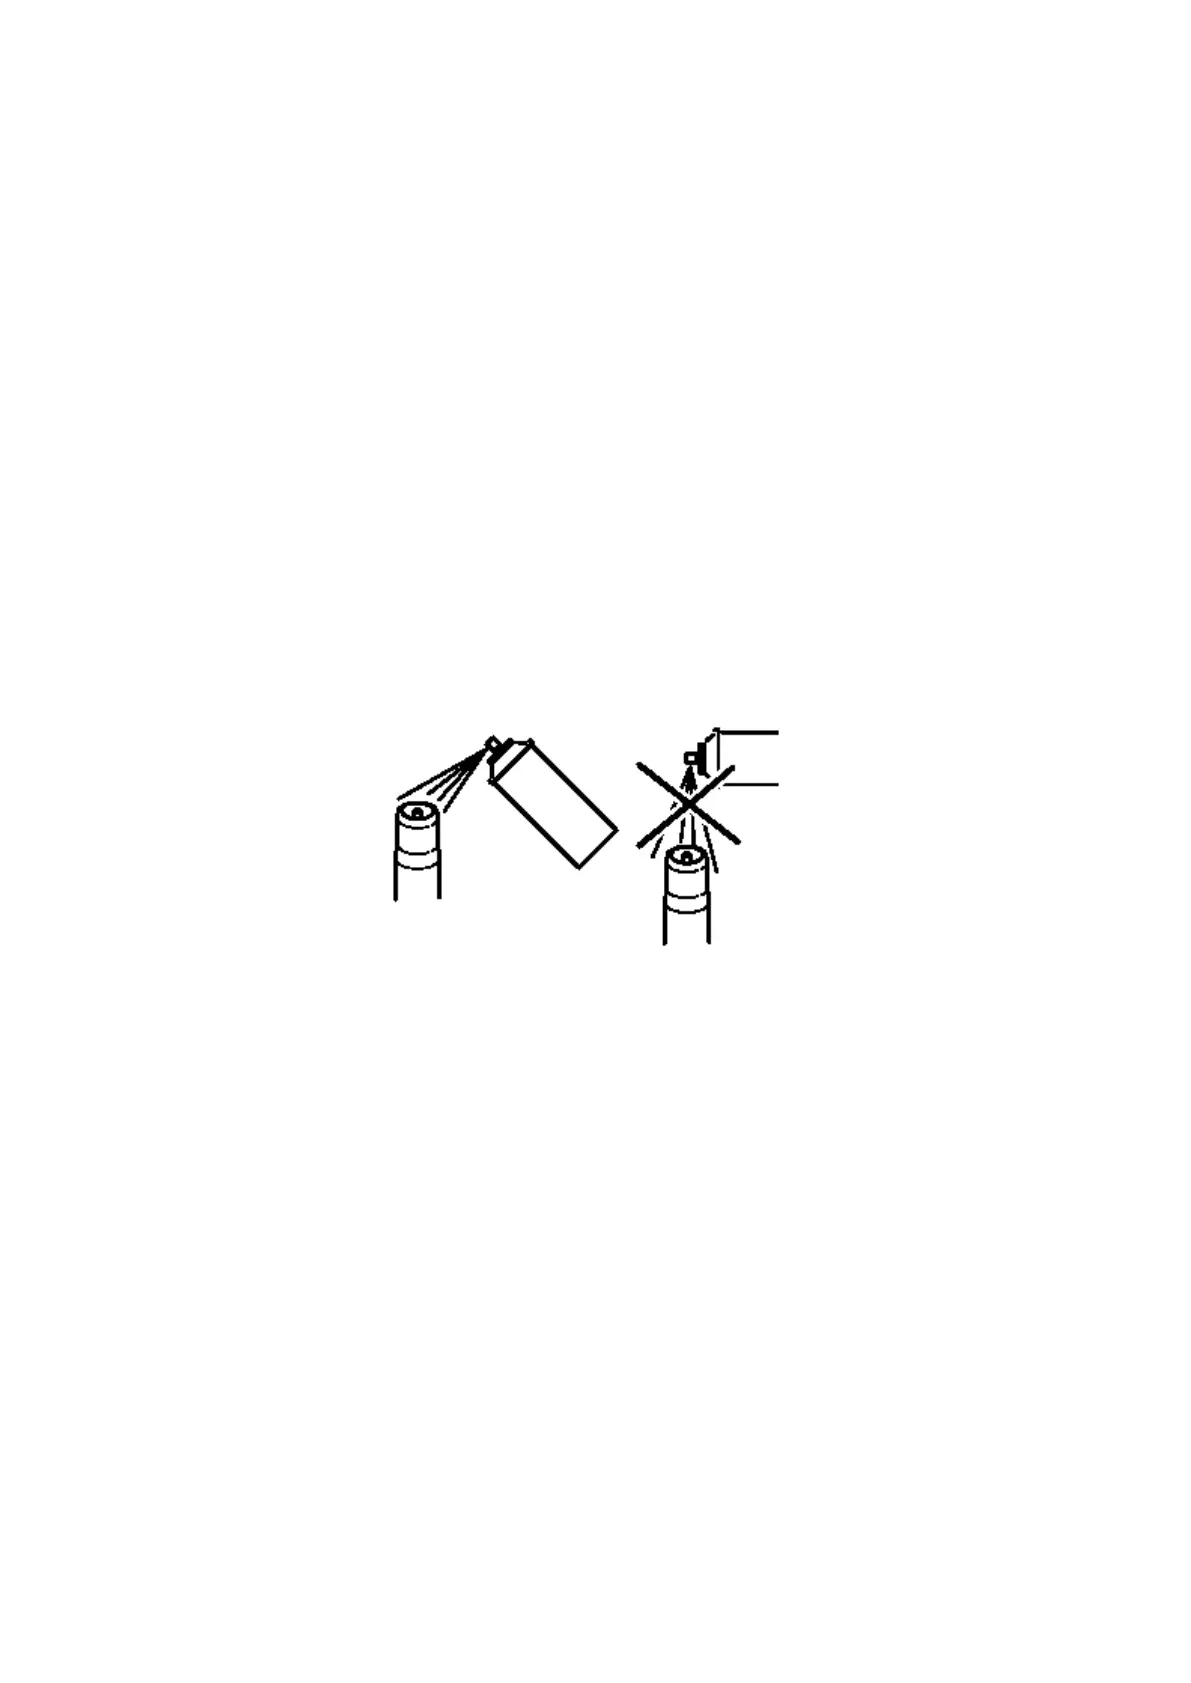
• Anti-spatter spray should be used with caution, as increased presence of the
spray in nozzle diminishes gas protection and increases danger of spark-over.
• The gas nozzle and front parts of torch must be kept free of weld spatter.
Spray anti-spatter agent at an angle into the gas nozzle from two directions.
Use ESAB Anti spatter agent to prevent spatter sticking.
• The contact tip has to be replaced when the hole has become more than twice
the wire diameter. The new tip must be screwed on properly to its base.
20



 To Next Page