840D/828D SINUMERIK Operate
Notes
Work offset
Section 4
Display area Description
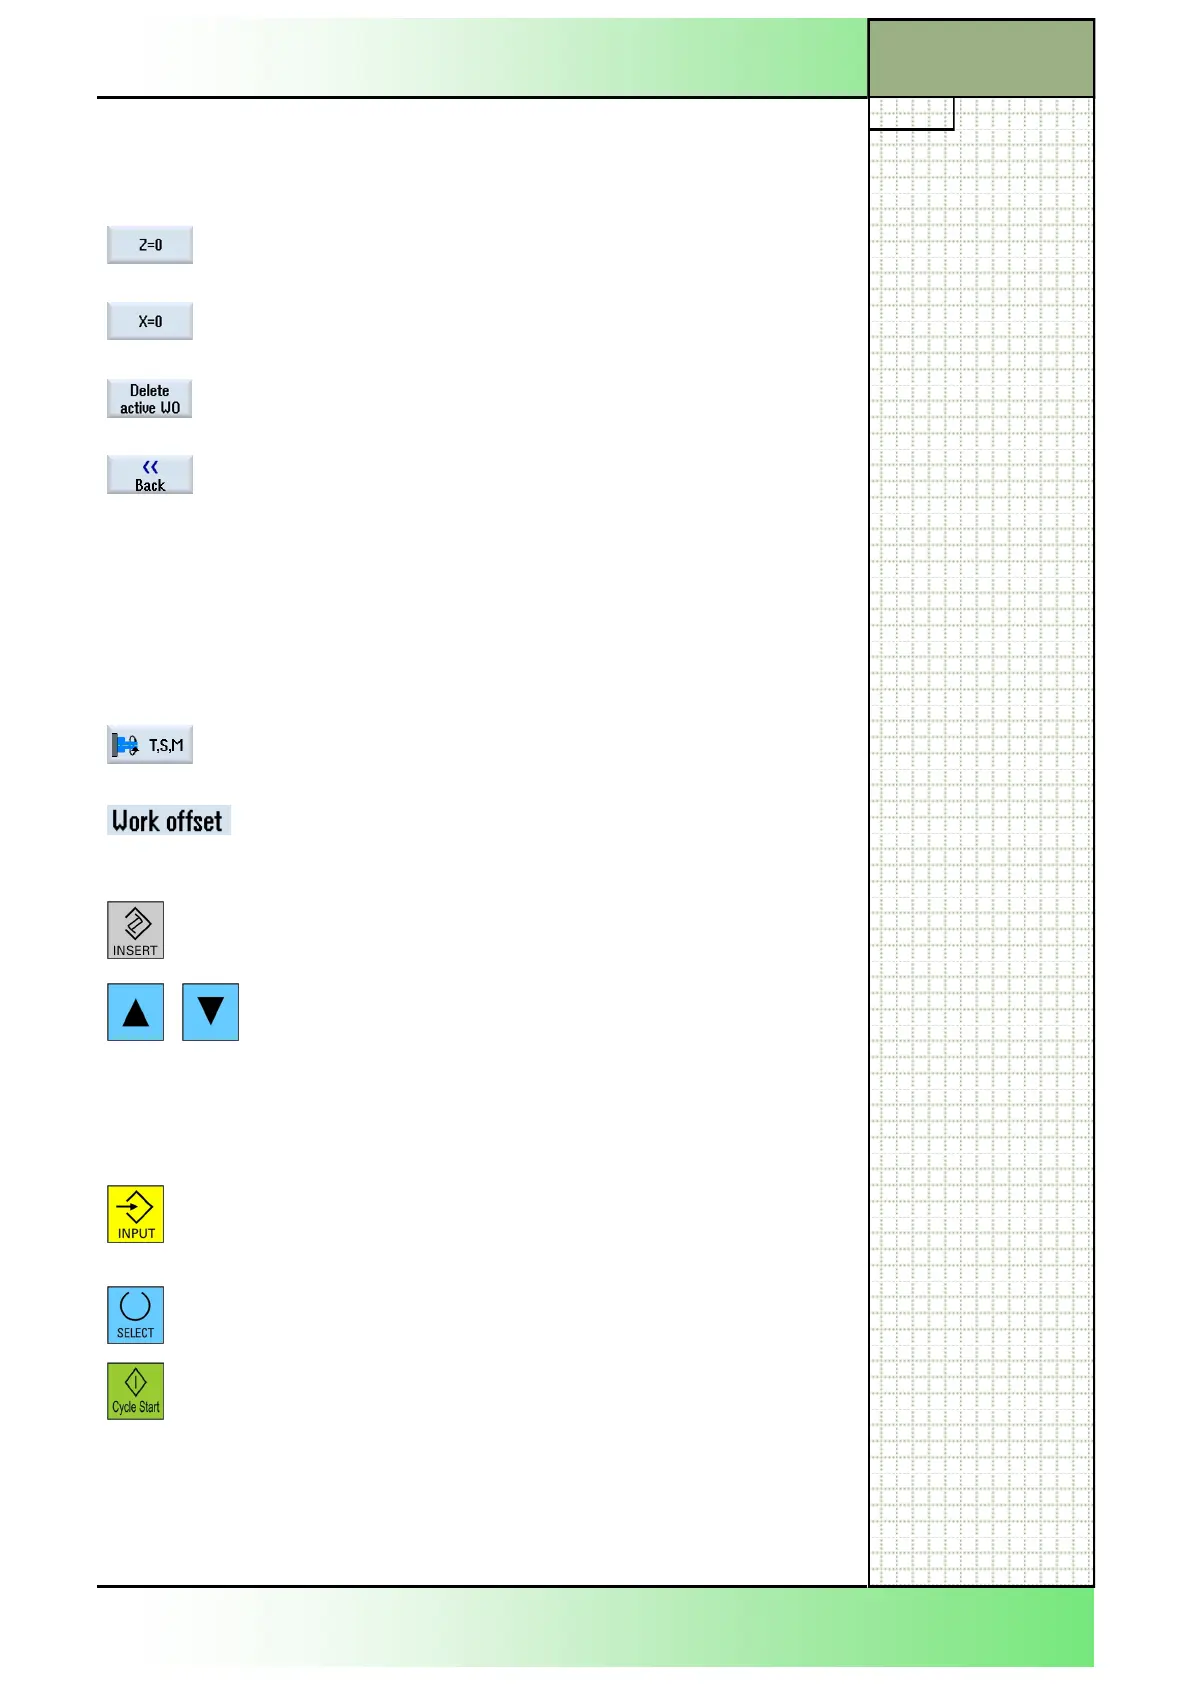
By pressing the VSK 1 "Z=0" the position of the Z-
axes will be reset to zero.
By pressing the VSK 2 "X=0" the position of the X-
axis will be reset to zero.
By pressing the VSK 5 "Delete active WO" the zero
point offset of all axes is set back to zero.
By pressing the VSK 8 "Back" you switch back to
the main screen of the Sinumerik Operate.
Note: After setting a position or deleting a zero point off-
set you switch back automatically to the main
screen of the Sinumerik Operate.
4.2 Vertical softkey bar
4.3 Parameters for the "Work offset"
Press the HSK 1 "T,S,M" to activate the T,S,M
(Tool-, spindle- and machine) -mode.
In the input mask navigate to the input field "Work
offset".
By pressing the "INSERT"-key on the keyboard, an
option menu opens where you can make the de-
sired selection of possible zero point offsets.
You can navigate through this menu by means of
-- --keys on
the keyboard.
Hint:
Navigating in the long lists can be easier by press-
ing the initial letter or number of the parameter to
suitably filter the selection.
When the desired zero point offset is marked or-
ange, you can accept this value by pressing the yel-
-key on the keyboard.
Alternatively you can toggle through all possible
options by pressing the "SELECT"-key repeatedly.
By pressing the button "CYCLE START" on the ma-
chine control panel the chosen zero point offset is
activated.



 To Next Page