32
in the
overhead
position
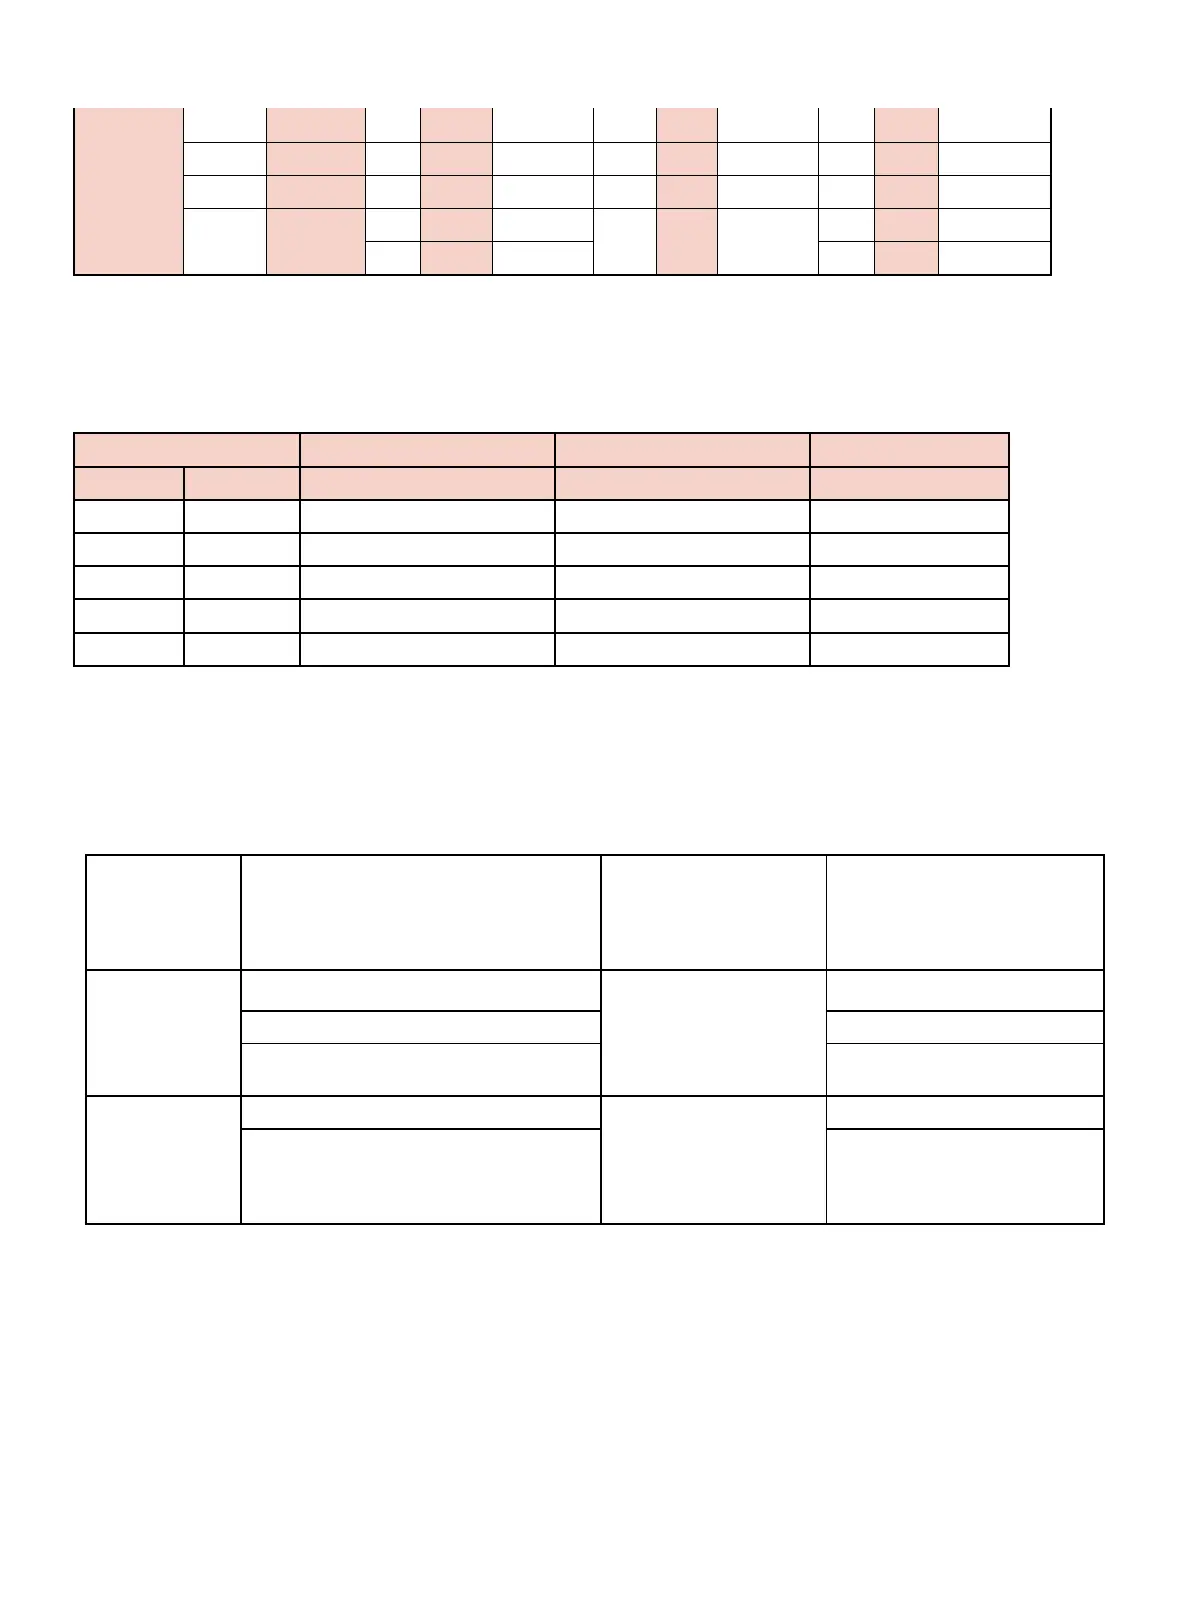
3~4 0.12-0.16 3.2 0.12 90~120 ~ ~ ~
5~6 0.2-0.24 4 0.16 120~160 ~ ~ ~
≥7
≥0.28
4 0.16 140~160 4 0.16 140~160
~ ~
3.2 0.12 90~120
4 0.16 140~160
3.2 0.12 90~120
4 0.16 140~160 4 0.16 140~160
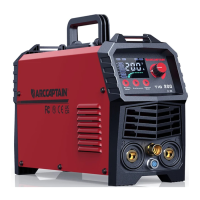
Current range of thorium (cerium) tungsten electrode of various diameters
Tungsten diameter DC positive polarity DC negative polarity AC
mm inch A A A
1 0.04 15~80 — 20~60
1.6 0.06 70~150 10~20 60~120
2.4 0.09 150~250 15~30 100~180
3.2 0.12 250~400 25~40 160~250
4 0.16 400~500 40~55 200~320
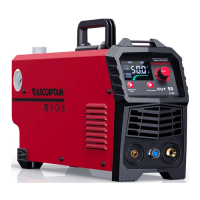
When the welding conditions do not meet the requirements, the phenomenon described in the following table
will occur.
Common welding problems
Unsuitable
Welding
Conditions
Influence
Unsuitable Welding
Conditions
Influence
The welding
gun is far
away from the
workpiece
The arc becomes long
The welding gun is
too close to the
workpiece
The arc becomes shorter
The welding bead becomes narrow Welding spatter will occur
The gas protection effect is reduced
The welding
current is too
large
The welding bead becomes narrow
The welding speed is
too fast
The bead becomes short
The depth of penetration and excess
weld metal becomes greater
The depth of penetration
and excess weld metal
becomes smaller
Digital Welding Expert, Know You More
https://www.arccaptain.com


 To Previous Page