5
3.1 Technical Parameters
SN Project Name Unit Value
1 Power voltage VAC AC110V±15% AC220V±15%
2 Input frequency Hz 50
3 Rated input current A 33@TIG 35@MMA
4 Capacity of power supply KVA
6.0@TIG 7.5@MMA
5 Output current range (TIG) A 10~120 10~200
6 Output current range (MMA) A 10~110 10~160
7 Arc force range A 0~40
8 Hot start current range A
0~80
9 No-load voltage V
60
10 Rated working voltage V
18@TIG 26.4@MMA
11 AC output frequency Hz 20~250
12 AC balance % 20~60
13 Background level A 10~200
14 Pulse frequency
Hz
0.5~200 (DC) 0.5~25(AC)
15 Pulse duty factor
%
5~95
16 Pre-flow time S 0~5
17 Post-flow time S 0~15
18 Rising time S 0~15
19 Fall time S 0~15
20 Remote control -
Yes
21 Arc start mode
- HF arc starter
22 Efficiency (%) %
80
23 Duty cycle (%) % TIG: 200@25% - MMA: 160@25%
24 Power factor - 0.70
25 Type of cooling - Air cooled
26 Working temperature range °C —10~+40
27 Storage temperature range °C —25~+55
28 Protection class - IP21S
29 Insulation class - B
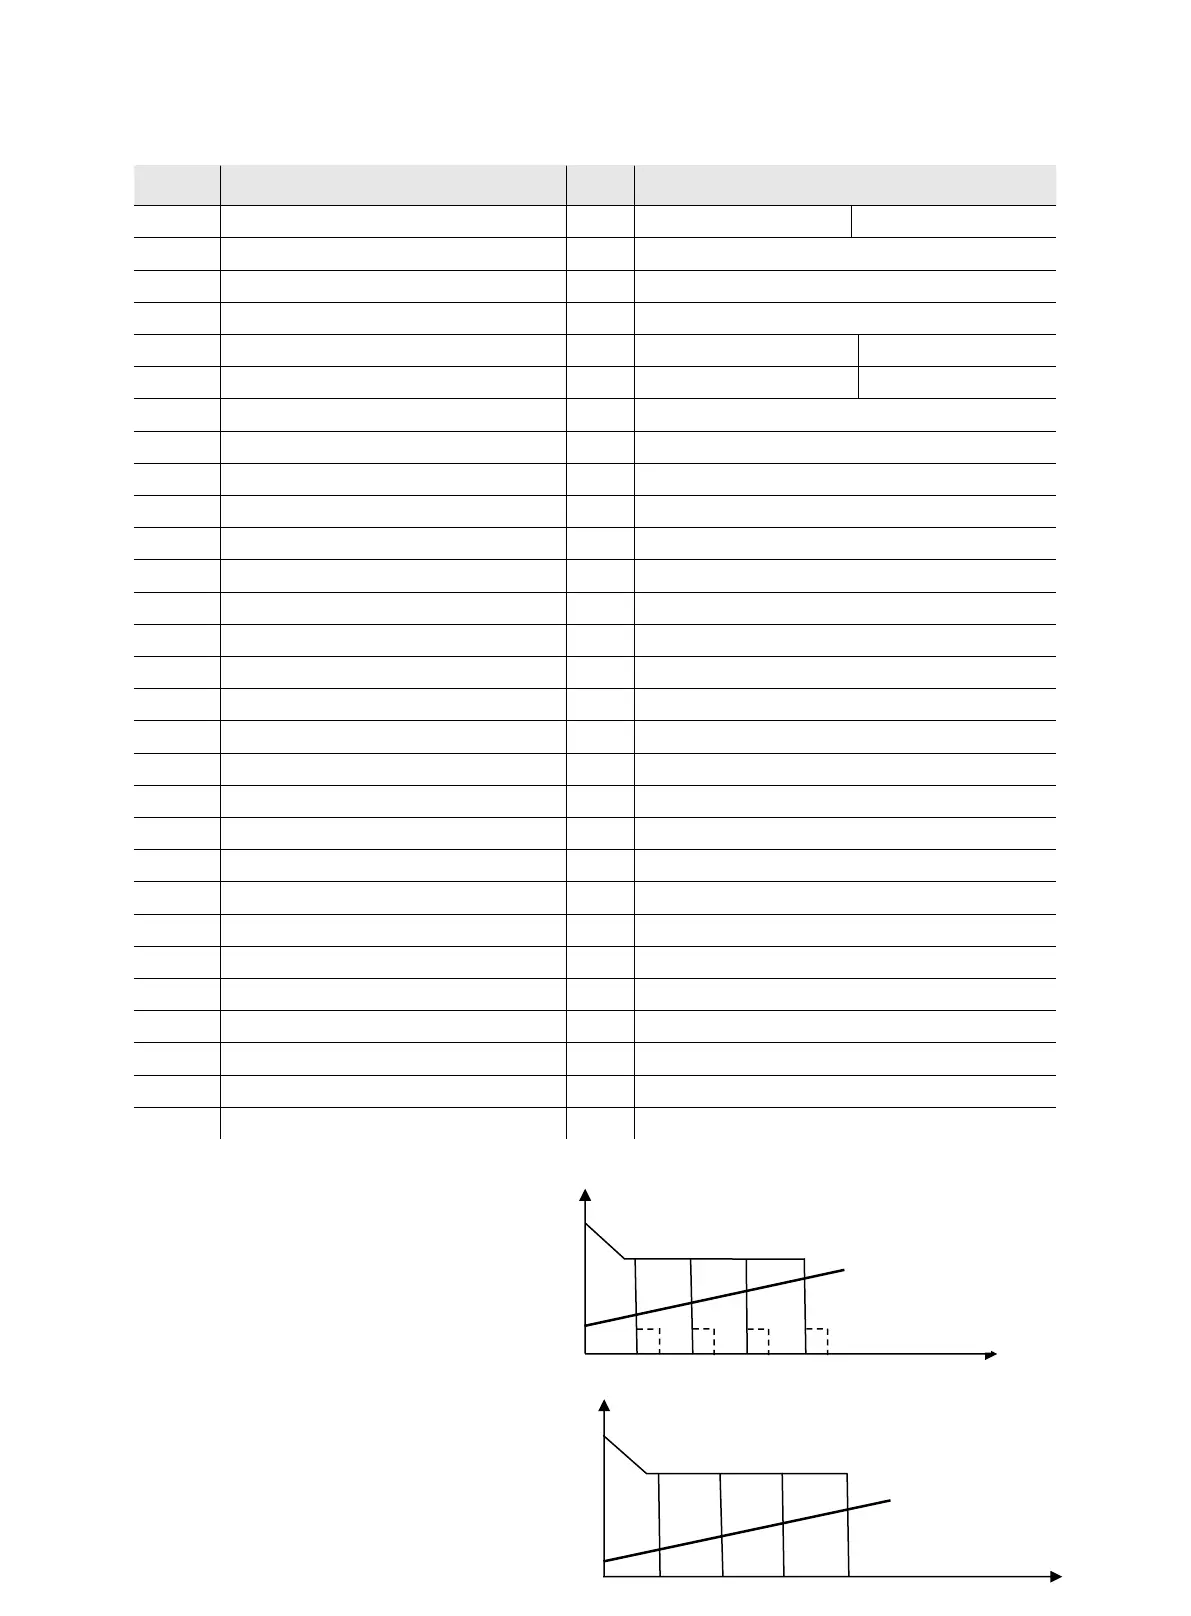
3.2 External (Static) Characteristic Curve
MMA electrode welding
has drop characteristic, and outputs
the external (static) characteristic
curve as shown in the right figure:
Simple TIG has drop characteristic,
and outputs the external (static)
characteristic curve as shown in the right figure:
MMA: U
2
=20+0.04I
2
(≦44V
TIG: U
2
=10+0.04I
2
(≦34V
U
0
I(
U(V)
U
0
I(A)
Digital Welding Expert, Know You More
https://www.arccaptain.com


 To Next Page