12
13.2
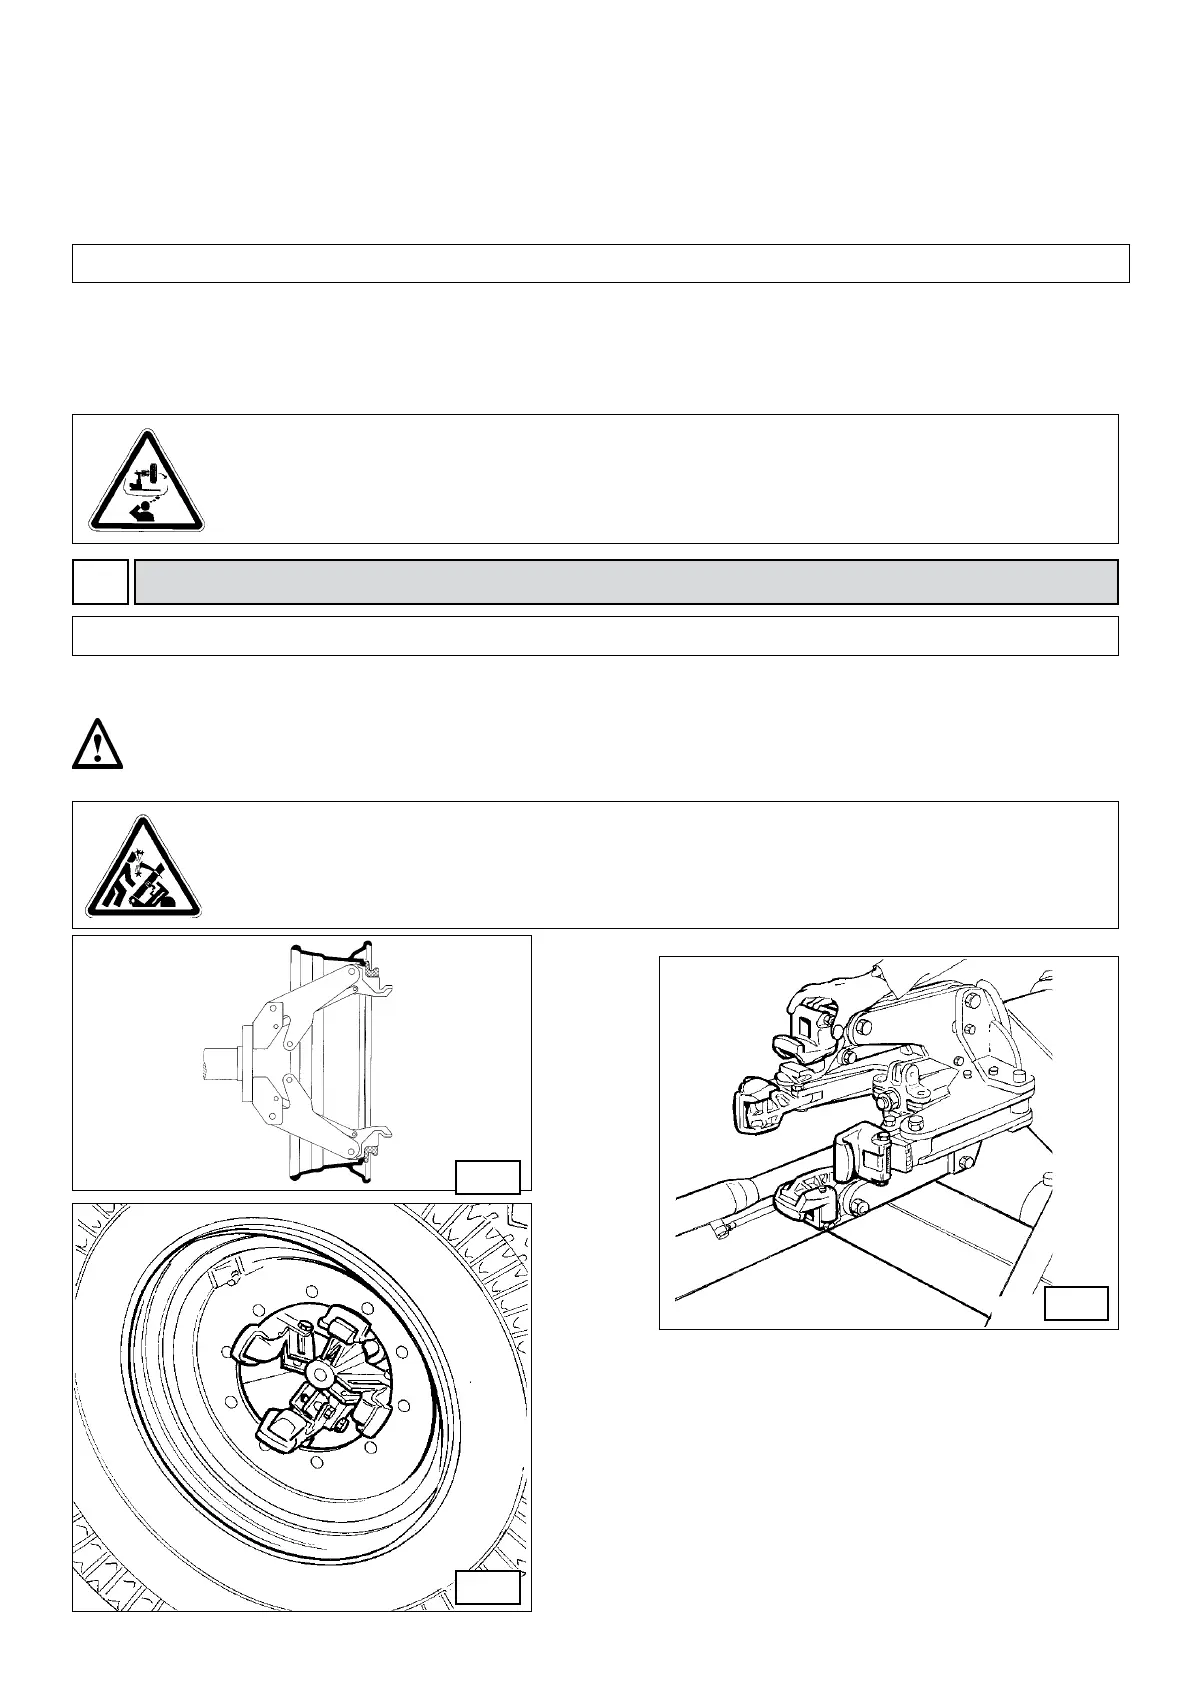
The most convenient clamping position on the rim may be selected according to gs E/1 - E/2 - E/3 - E/4 - E/5 and E/6.
Always remember that the safest clamping is on the central ange.
For rims with a drop center clamping, clamp the wheel so that the drop center is near the outside of the rim (g. E/1).
For rims exceeding a diameter of 46" and without a ange with center hole, the rim can be clamped with the 4 clamping extensions
provided on demand (# 9299270)
(# 9299272) LIGHT-ALLOY RIM CLAMPING
A set of specialclamps - especially designed for operating on light alloy rims without damaging them - is available upon request.
These clamps are to be inserted (bayonet-like mounting) into the jaw support of the self-centering chuck (see g. E/7).
Thanks to a wing screw the clamp can be locked on the support.
Clamp the rim as illustrated in g. E/8. The specially-made alloy-rim pliers are also available (#9299272).
DANGER!
Do not walk across the work area with a wheel clamped on the tire changer and lifted up from the
oor.
TUBELESS AND SUPERSINGLE TIRES
BEAD LOSENING
1) Clamp the assembly wheel on the self-centering chuck, as previously described, and ensure that the tyre is deated.
3) Lower the tool-holder arm (14, g. F) into working position and allow it to lock.
2) Take the mobile control unit to work position C.
DANGER!
Always check to be certain that the arm is correctly hooked to the carriage.
E/6
E/7
E/8


 To Next Page