6 CONTROL PANEL
0463 641 001
- 26 -
© ESAB AB 2018
within the short arc region (150–200A). To do thicker than 6mm plate you need to switch the
power source into Manual MIG mode.
NOTE!
The weld chart indicates up to 6mm material thickness but does not list the maximum
material thickness capability of all wires in Manual MIG mode. Mild Steel Solid wires
for example may achieve good weld results on up to 12mm material.
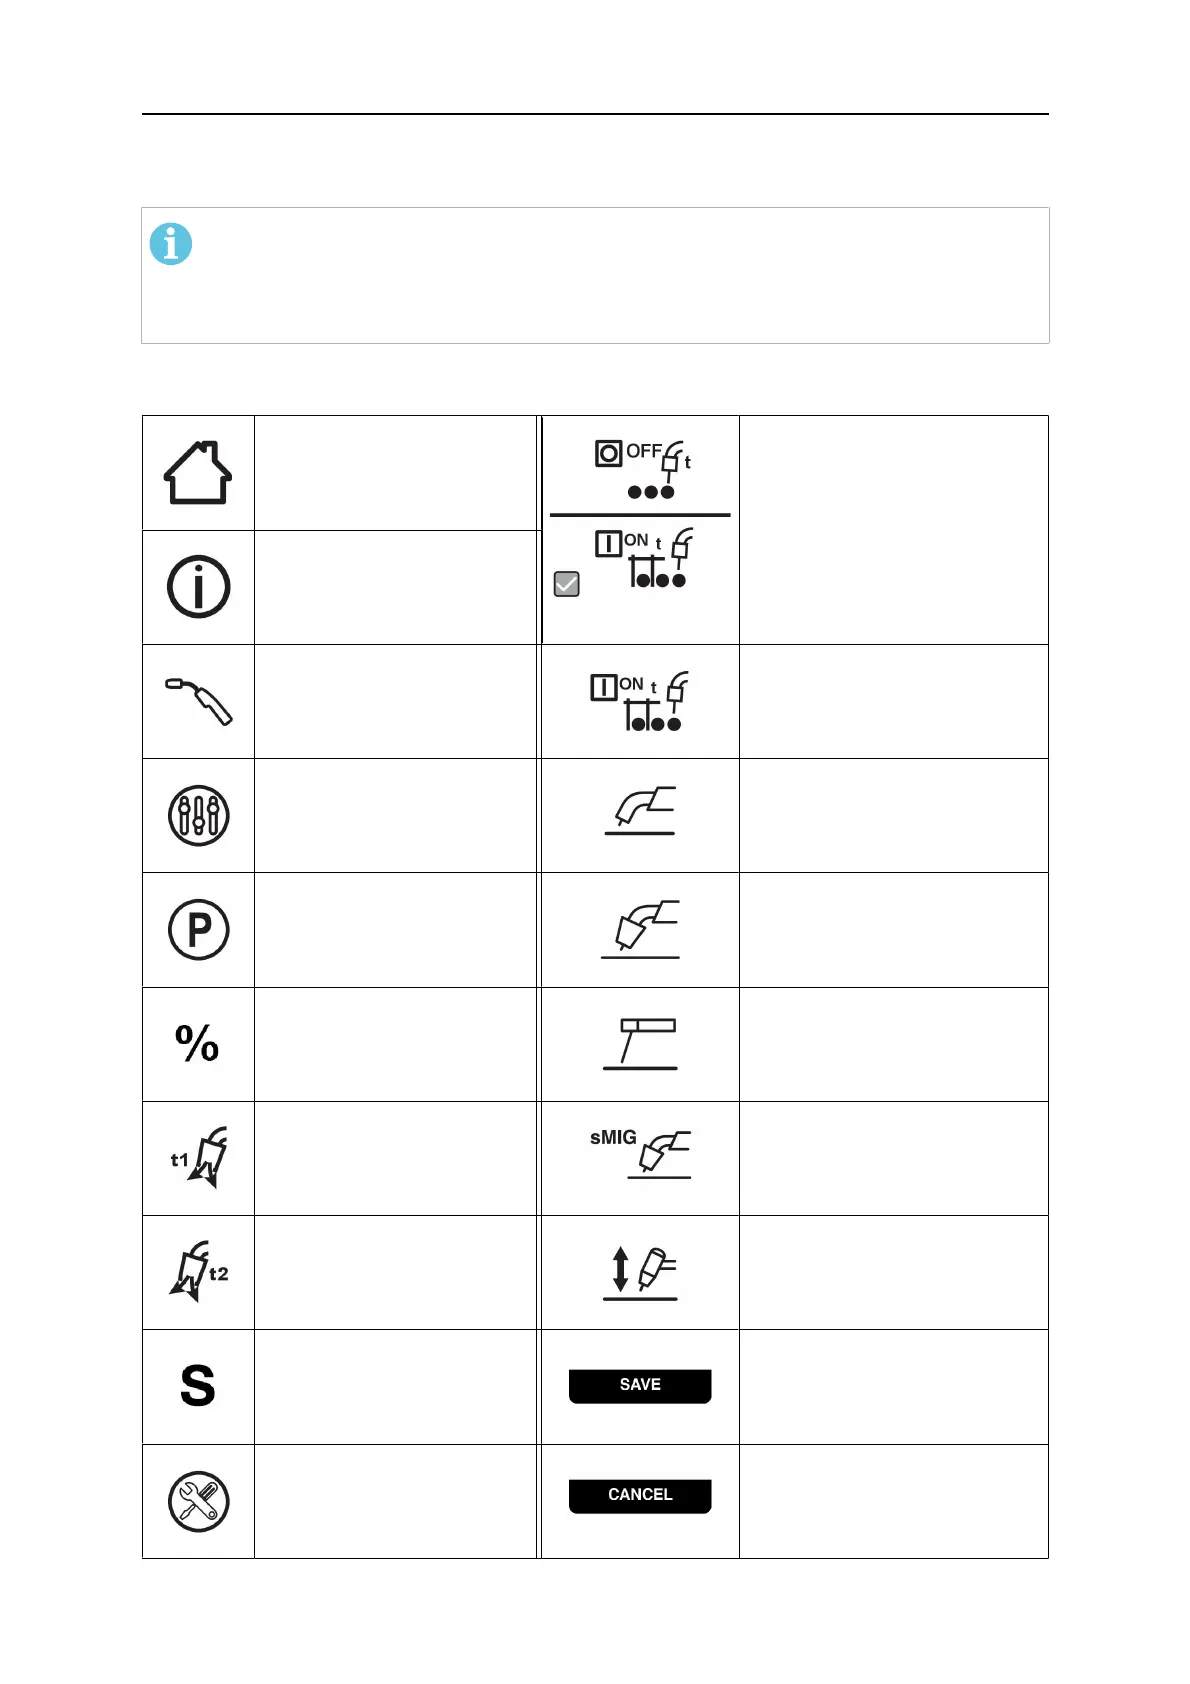
6.1.11 Icon reference guide
Home
Spot time on/off selection
Information
MIG Torch Spot time on adjustment
Parameters Flux cored
Parameters Manual MIG
Percent MMA
Preflow The time the
shielding gas stays on
before the welding arc is
started
Smart MIG
Postflow The time the
shielding gas stays on after
the welding arc is stopped
Lift-TIG
For more information, see
section "Lift TIG operation"
Seconds
Saving welding programs for
a specific application when in
the Memory Mode
Settings on user manual
menu
Cancel


 To Next Page