24
GYSPOT ARCPULL 350
EN
PRODUCT OPERATION
When it is switched on, the product starts up again in the last operating mode using the last welding parameters set.
Changing the mode (Manual or Synergic) is done via the Main Menu.
WELDING IN MANUAL MODE
In Synergic Mode, the arc height, times and currents for the dierent phases are selected automatically by the machine.
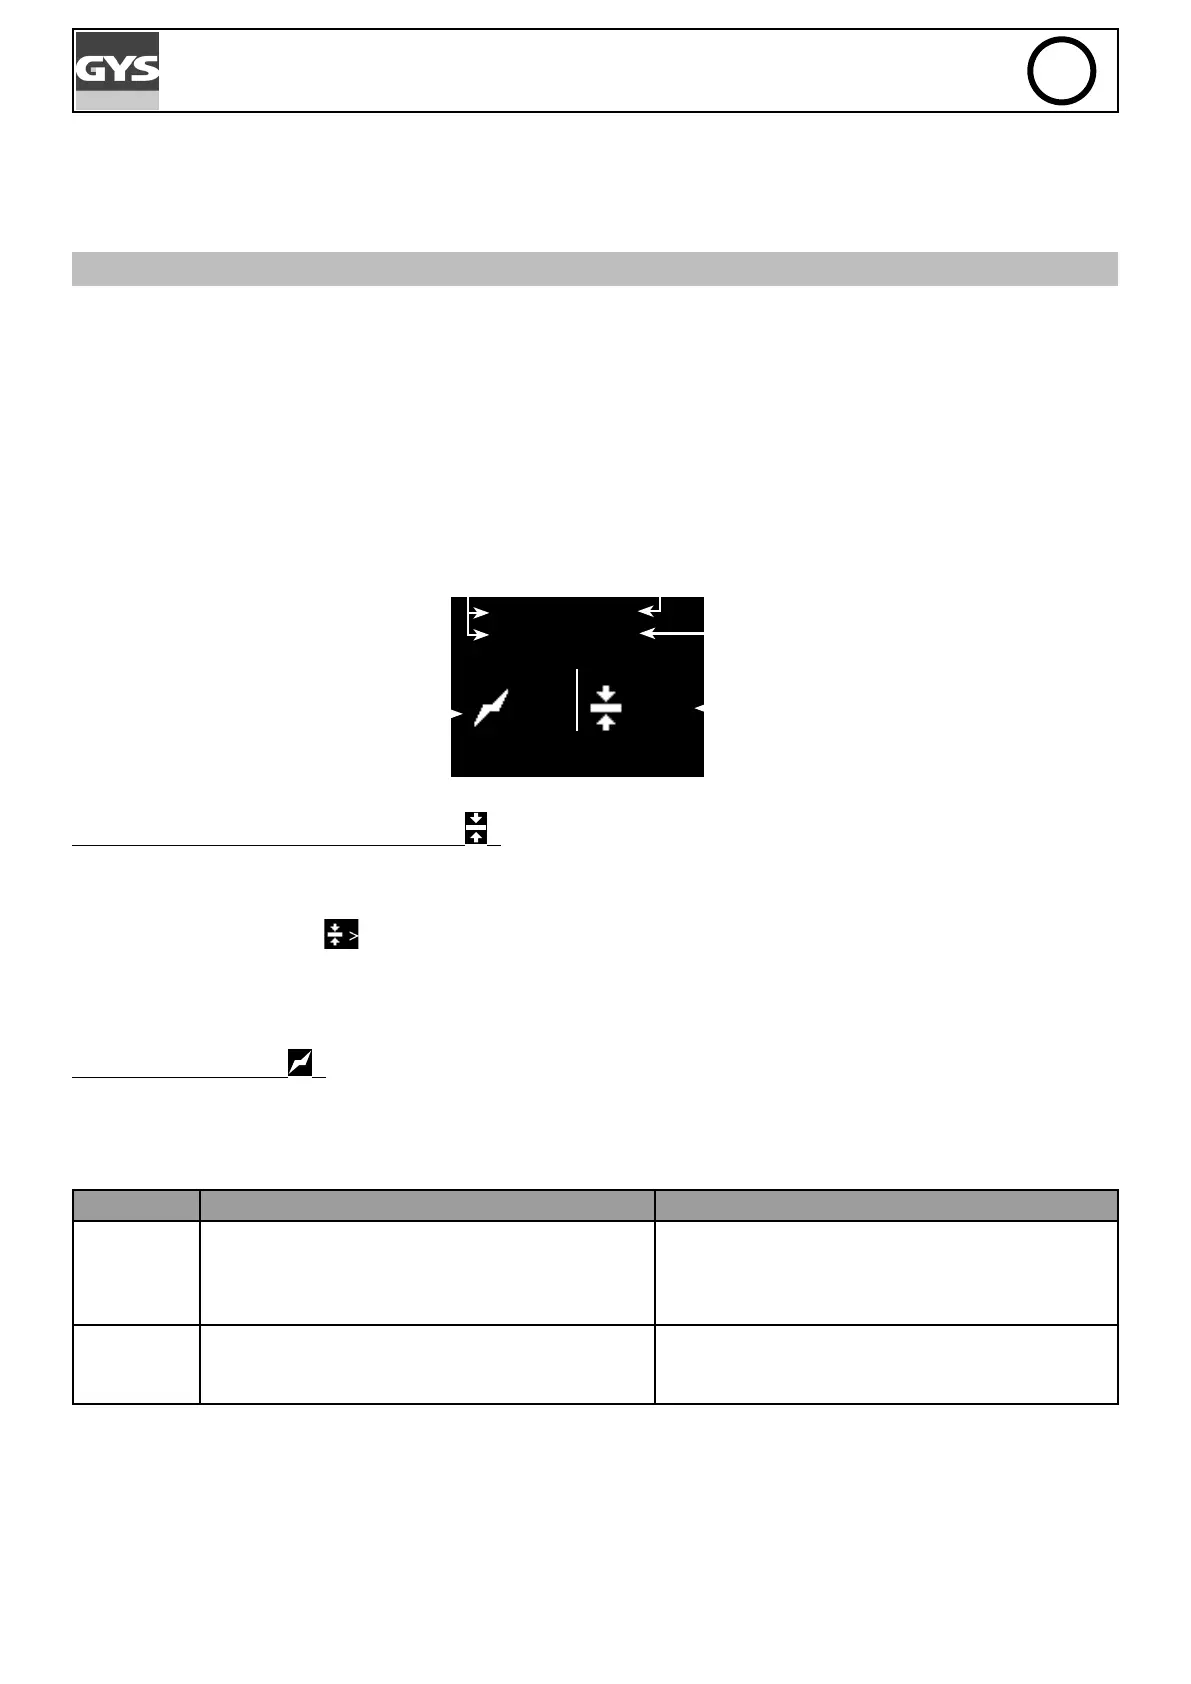
The type of gas to be used is displayed on the screen. If the polarity of the gun is wrong, a message appears on the
display and the fault LED (red) of the gun ashes.
The dierent welding parameters are established for the inserts sold by GYS.
These synergies remain valid for longer inserts (≤45mm) as long as they are of the same type and material as those
sold by GYS.
It is recommended to make some preliminary welding tests if other consumables are used.
zone de
message
Ri ng 1. 5mm
Fe Gas
+1
2. 0
message
area
Type, material and size of
insert
Gas to use
Sheet metal thickness
Coecient Power
Thickness of the support sheet metal (value )
To increase or decrease the sheet metal thickness to which the insert will be welded use keys D+ and D-.
If the thickness of the sheet metal is less than that shown on the display, a marking on the rear of the weld may appear.
When the station displays « », the sheet thickness is high enough so that it is not marked on the back while having
an optimal weld.
If this pictogram does not appear, then the maximum sheet metal thickness has been reached. Beyond this thickness,
the welding of the insert is no longer guaranteed.
Power coecient (value
)
The Power coecient is used to adjust the ignition current, the arc energy (current, time) and the attachment current.
Power can be adjusted between -10 and +10. To increase or decrease this coecient press keys G+ and G-.
Note: Weld synergies are optimized with a default Power coecient value of 0.
Power Action on the product Inuence on the weld
+1 point
• Increase the ignition current
• 2% increase in arc current up to 350A, then
3% increase in arc time up to 800ms.
• Increase the attachment current.
• Better arc ignition on poorly degreased sheet
metal..
• Better ignition in cold weather (<5°C).
• 2% increase of arc energy.
-1point
• Decrease the ignition current
• 2% reduction of the arc current.
• Decrease of the attachment current."
• Reduced risk of sticking during ignition.
• Suitable ignition in hot weather (>35°C).
• 2% decrease of arc energy.
To change the other synergistic welding parameters (materials, type and size of insert, gas) refer to the chapter «Syner-
gistic Settings».



 To Next Page