840D/828D SINUMERIK Operate
Notes
Description:
By using different drilling cycles (Centering, Drilling, Thread drilling) and a
position pattern, a more complex programGUIDE-program (drill pattern) is
to be created in ShopTurn.
Aim:
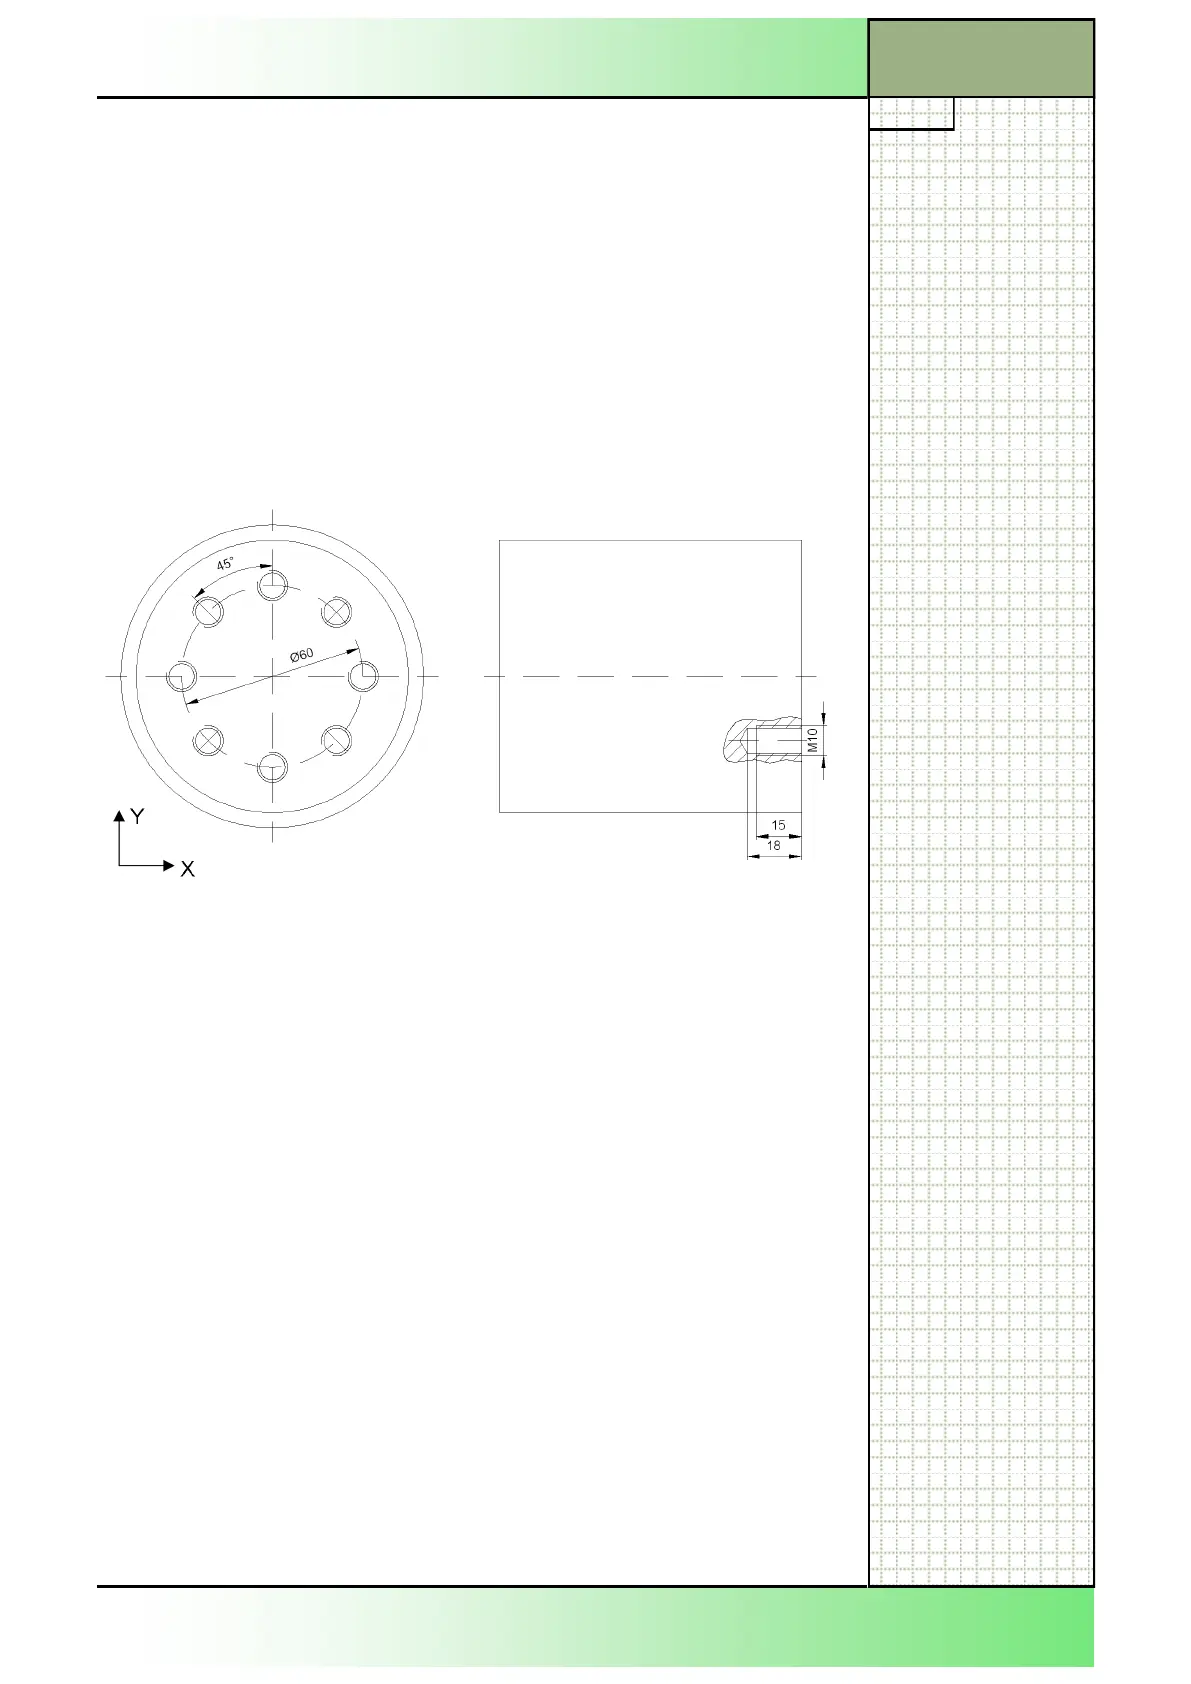
The workpiece shown below is to be programmed.
Afterwards, the program is to be simulated.
The following tools and technology data are to be used.
Tool data:
Center drill 12 mm (CENTERDRILL_D12)
Drill Ø 8,5 mm (DRILL_D8.5)
Tap M10 (TAP_M10)
Technology data: F 150 mm/min
S 500 rpm
Starting-up strategy As a start position for the machining, the first pro-
grammed drill hole is to be used.
This position is approached in rapid traverse.
Section 3
Complex programming example




 To Next Page