B611
B611 Page 8 840D/828D SINUMERIK Operate
Notes
3.1 Example: Drill pattern
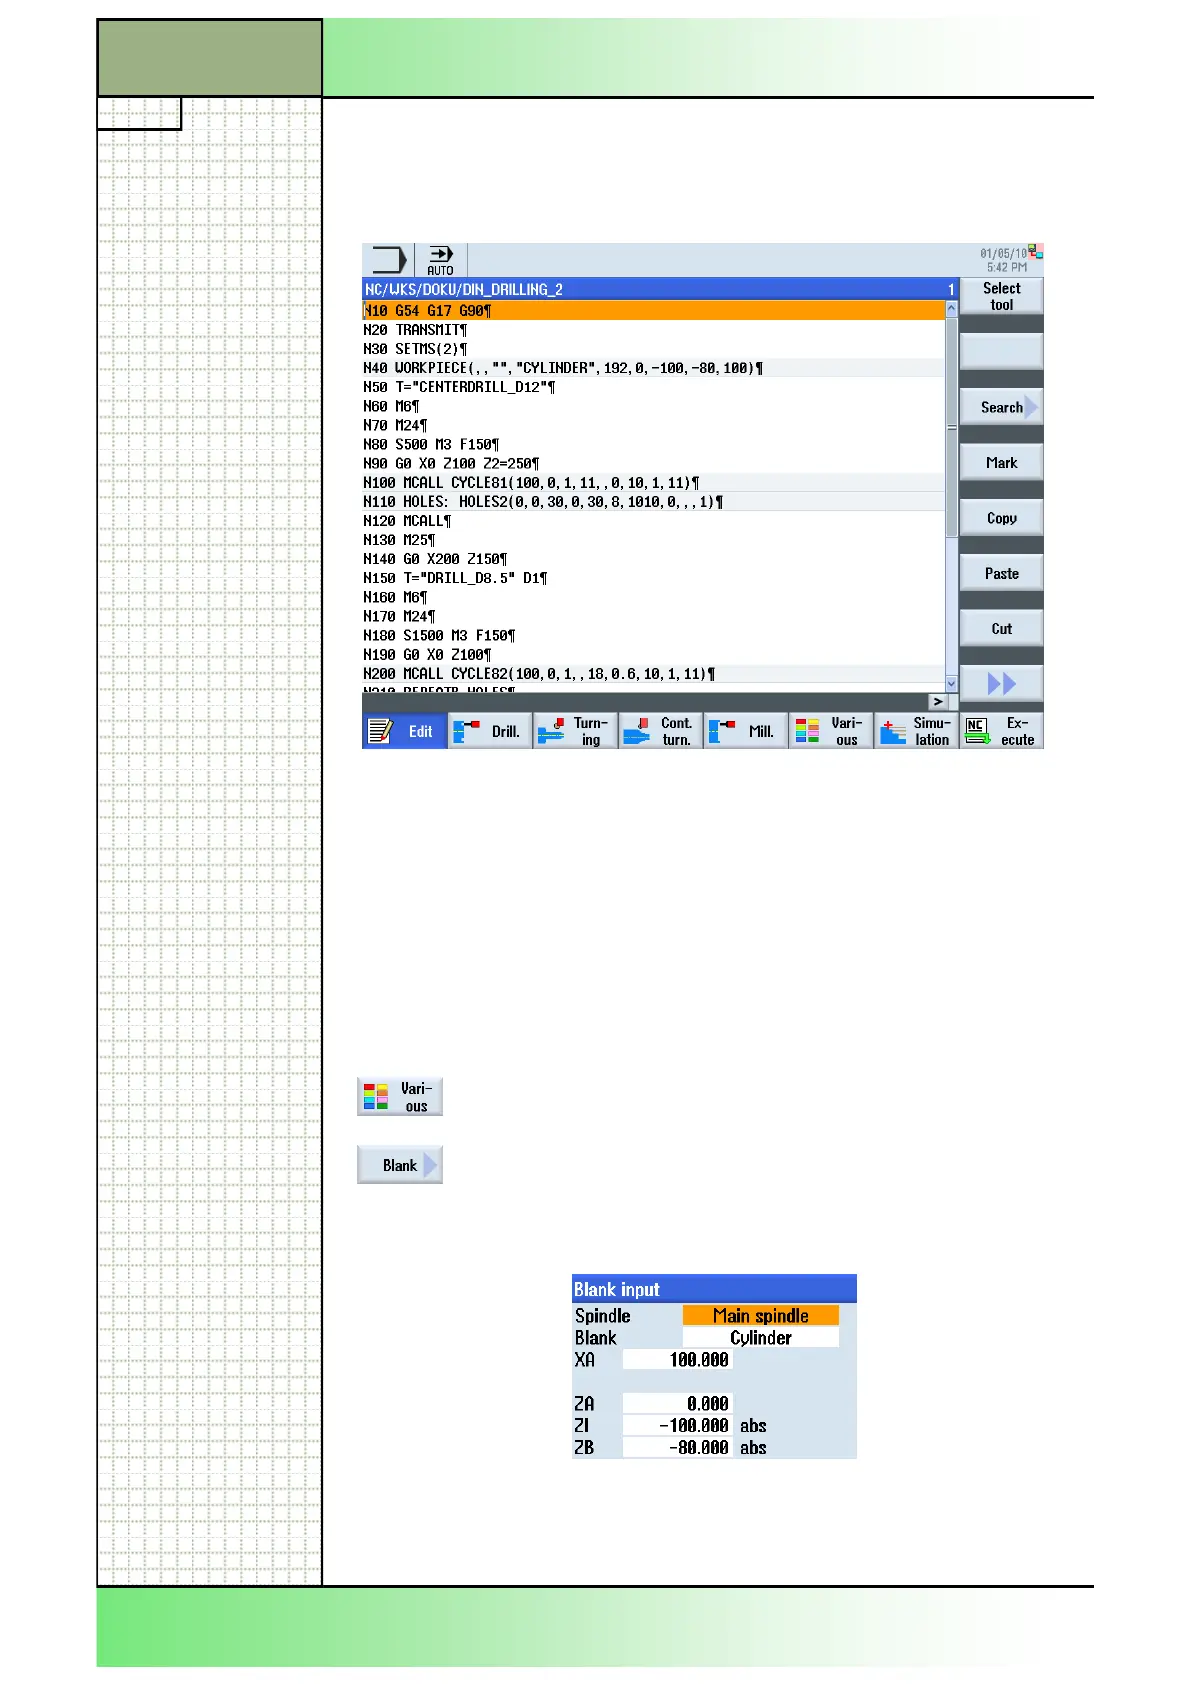
The following program, with the call up of a drilling-, center drilling- and
thread drilling-cycle, is to be programmed:
Create a new G code programGUIDE-program in ShopTurn, like described
in section 2.1 in this module.
Give the program a name, for example “DIN_DRILLING_2”.
1. Program the first G code line of the program:
N10 G54 G17 G90
2. Program the following G code commands:
N20 TRANSMIT
N30 SETMS(2)
3. Now insert a blank for the simulation.
For this, press the HSK 1.6 “Various” to open the
operating area “Various”.
Press the VSK 1 “Blank” to open the parameter
mask for the blank.
4. Insert the values into the parameter mask like dis-
played below:
Confirm your inputs by pressing the VSK 8 “Accept”.
The following line will be inserted into the program:
N40 WORKPIECE(,,"","CYLINDER",192,0,-100,
-80,100)
Complex programming example
Section 3




 To Next Page