840D/828D SINUMERIK Operate
Notes
5. Insert now a center drill tool into the program.
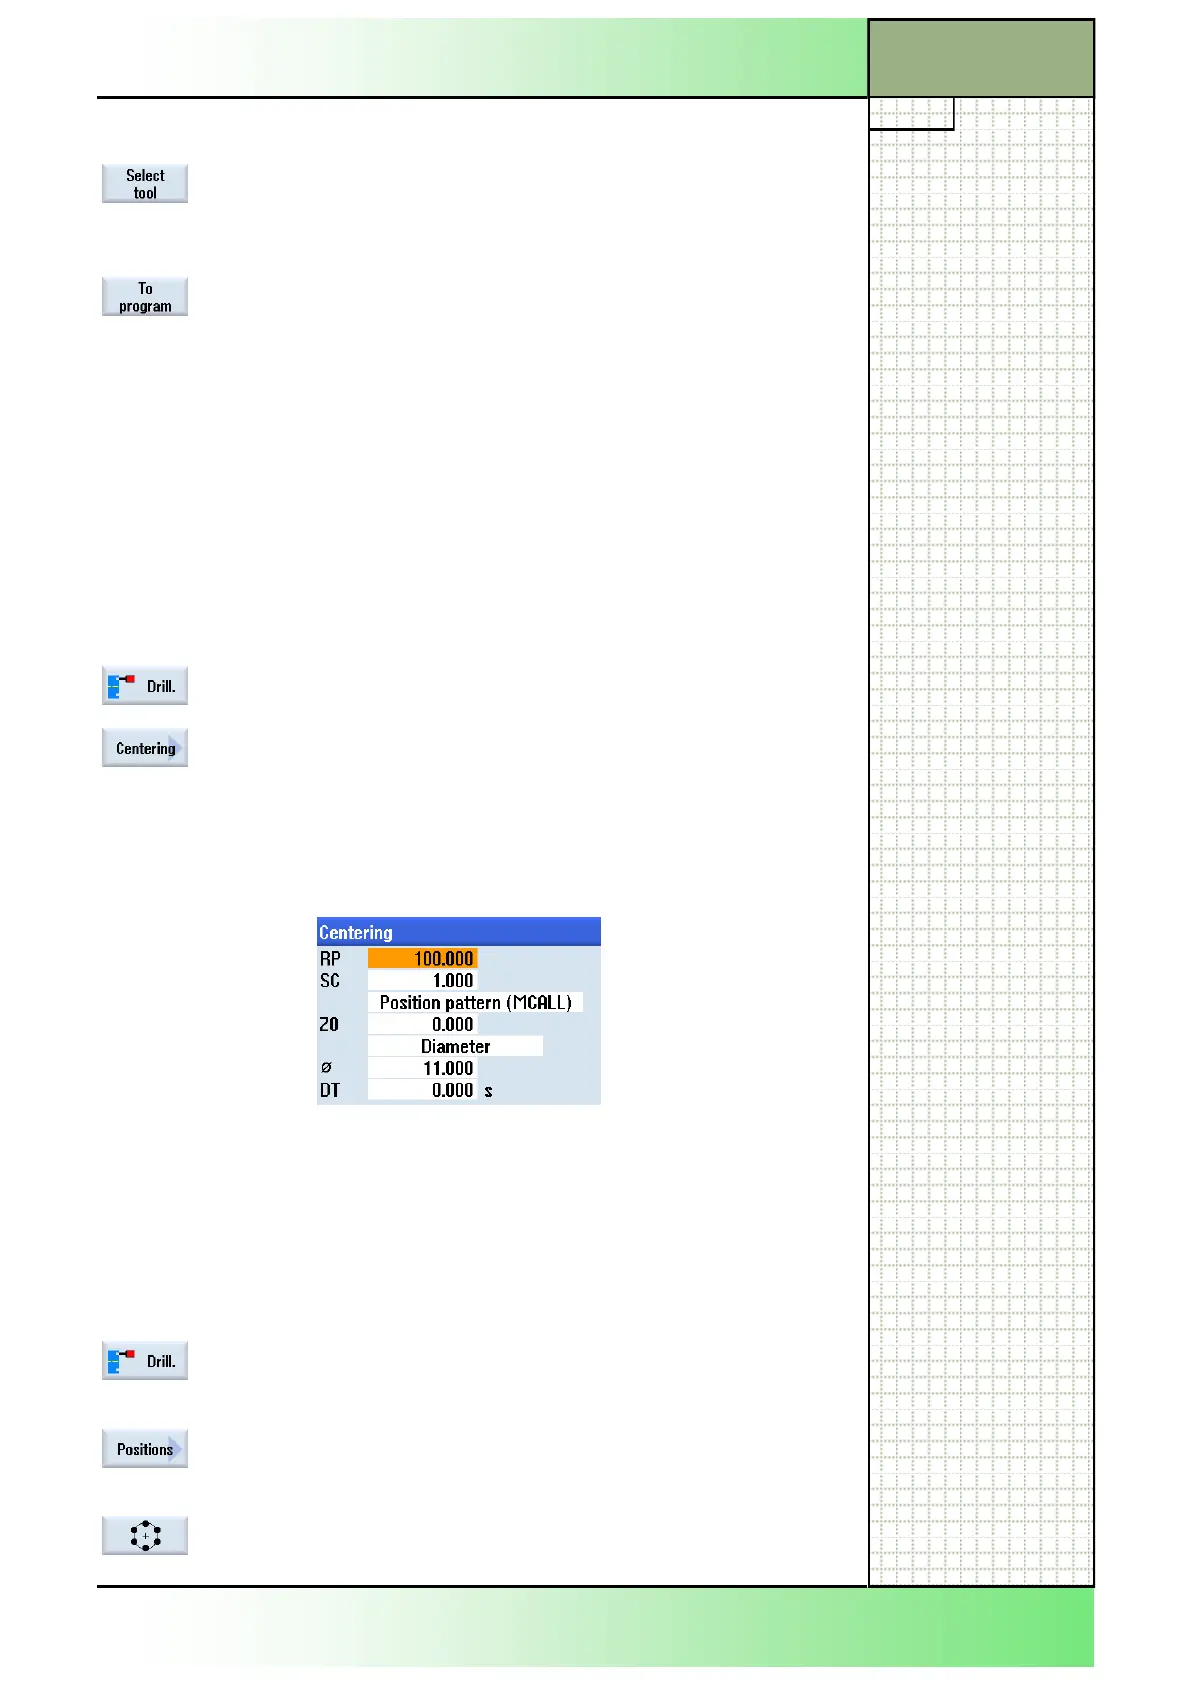
Press the VSK 1.1 “Select tool”.
The tool list window opens.
Use the blue cursor keys to select the tool
“CENTERDRILL_D12”.
Press the VSK 1.1 “To program”.
The program line N50 T="CENTERDRILL_D12" is
inserted into the program.
Optional you can program the line by hand.
6. Program the following G code commands:
N60 M6
N70 M24
N80 S500 M3 F150
N90 G0 X0 Z100 Z2=250
7.
Program the center drill cycle “CYCLE81”.
Press the HSK 1.2 “Drill.”, to open the technology
“Drilling”.
Press the VSK 1 “Centering”.
The input mask for the centering cycle “CYCLE81”
opens.
8. Insert the values into the parameter mask like dis-
played below:
Confirm your inputs by pressing the VSK 8 “Accept”.
The following line will be inserted into the program:
N100 MCALL CYCLE81(100,0,1,11,,0,10,1,11)
9. Program now a position pattern (Position circle) for
the following drillings.
Press the HSK 1.2 “Drill.” to open the technology
“Drilling”.
Press the VSK 7 “Positions” for selecting a position
pattern.
Press the VSK 3 “Position circle” to program the drill
hole positions for the following drilling cycles.
Section 3
Complex programming example




 To Next Page