840D/828D SINUMERIK Operate
Notes
Press the VSK 1.1 “To program”.
The following program line is inserted into the pro-
gram:
N120 T="CUTTER_D8"
5. Program the following G code commands:
N130 M6
N140 G0 X0 Z100
N150 TRANSMIT
N160 SETMS(2)
N170 M24
N180 S1000 M3 F2000
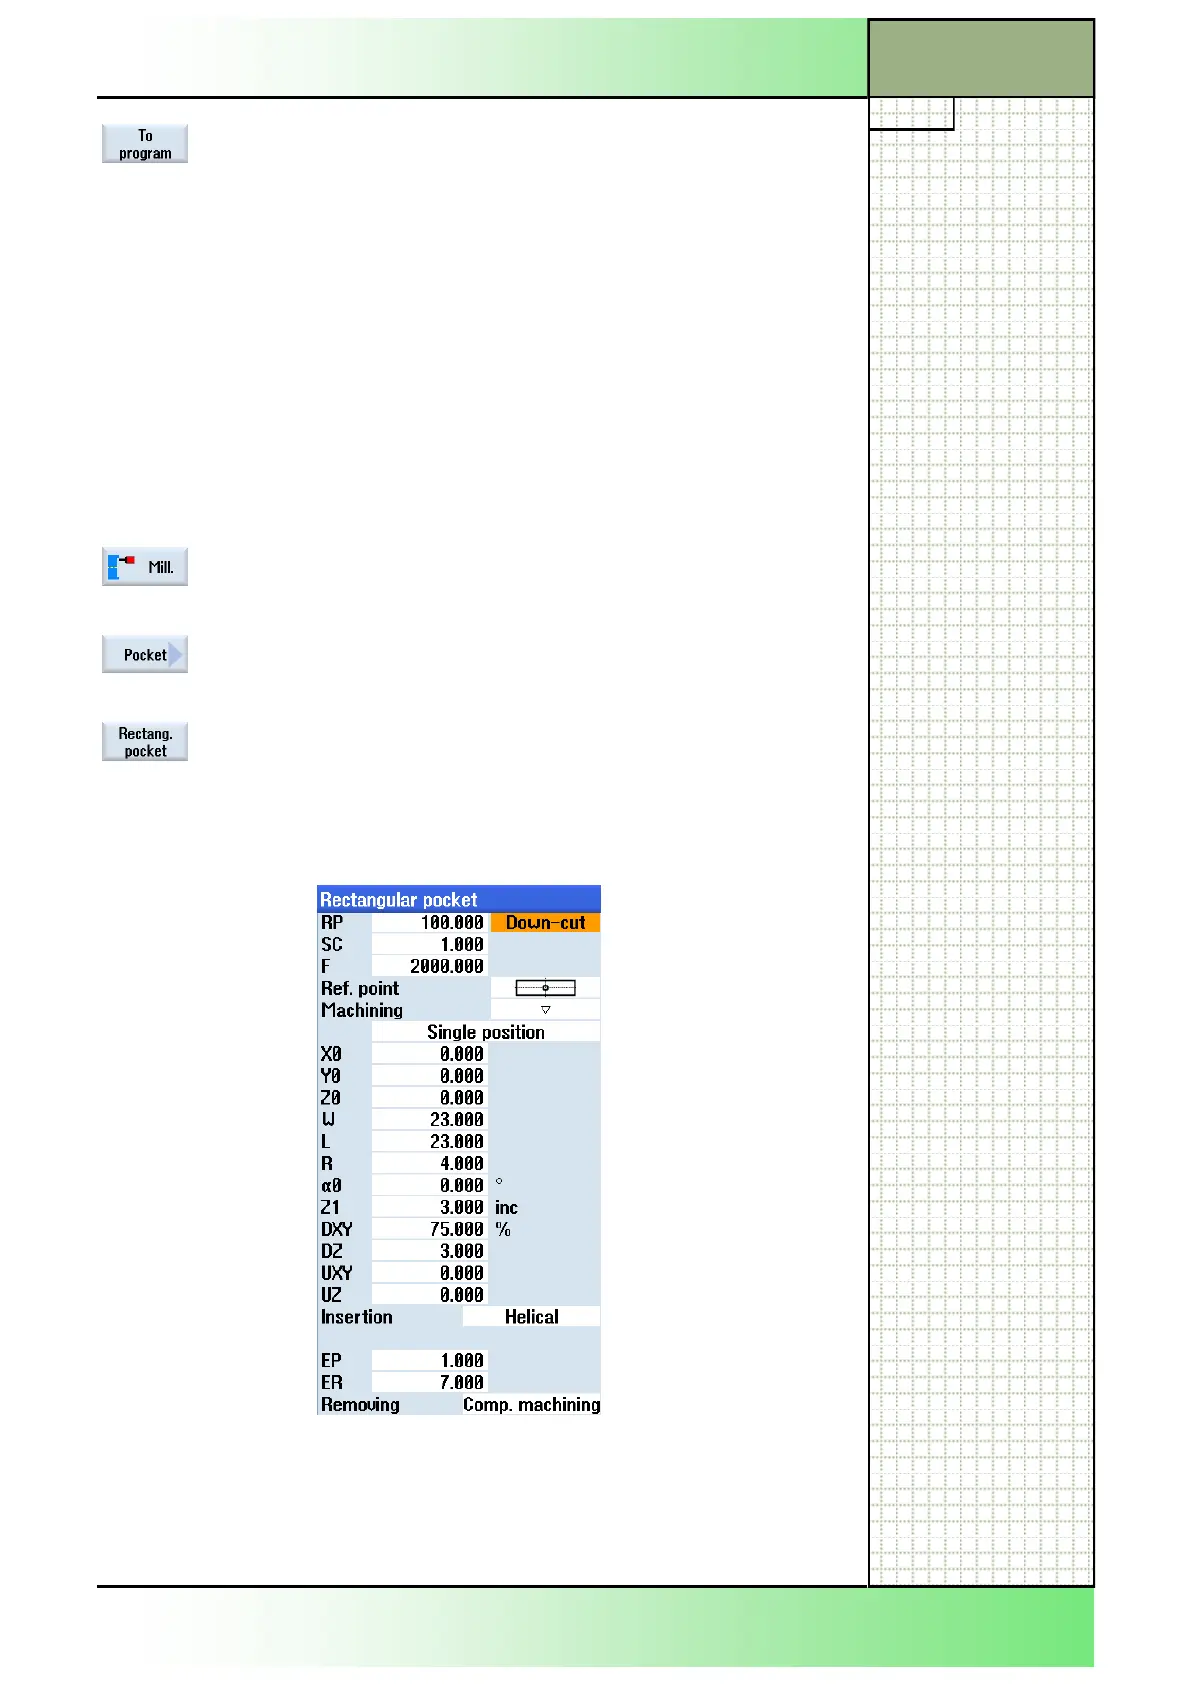
6. Insert a rectangular pocket cycle into the program.
For this, press the HSK 1.5 “Mill.” to open the func-
tion “Milling”.
Press the VSK 2 “Pocket”, to open the work area for
the “Pocket”.
Press the VSK 3 “Rectang. pocket” to open the pa-
rameter mask for the rectangular pocket cycle.
The following parameter window opens:
7. Fill out the parameter mask as follows.
Confirm your inputs by pressing the VSK 8 “Accept”.
The following G code line is inserted into the pro-
gram:
N190 POCKET3(100,0,1,3,23,23,4,0,0,0,3,0,0,
2000,0.1,0,21,75,8,3,15,7,1,0,1,2,11100,1,111)
Complex programming example
Section 3




 To Next Page