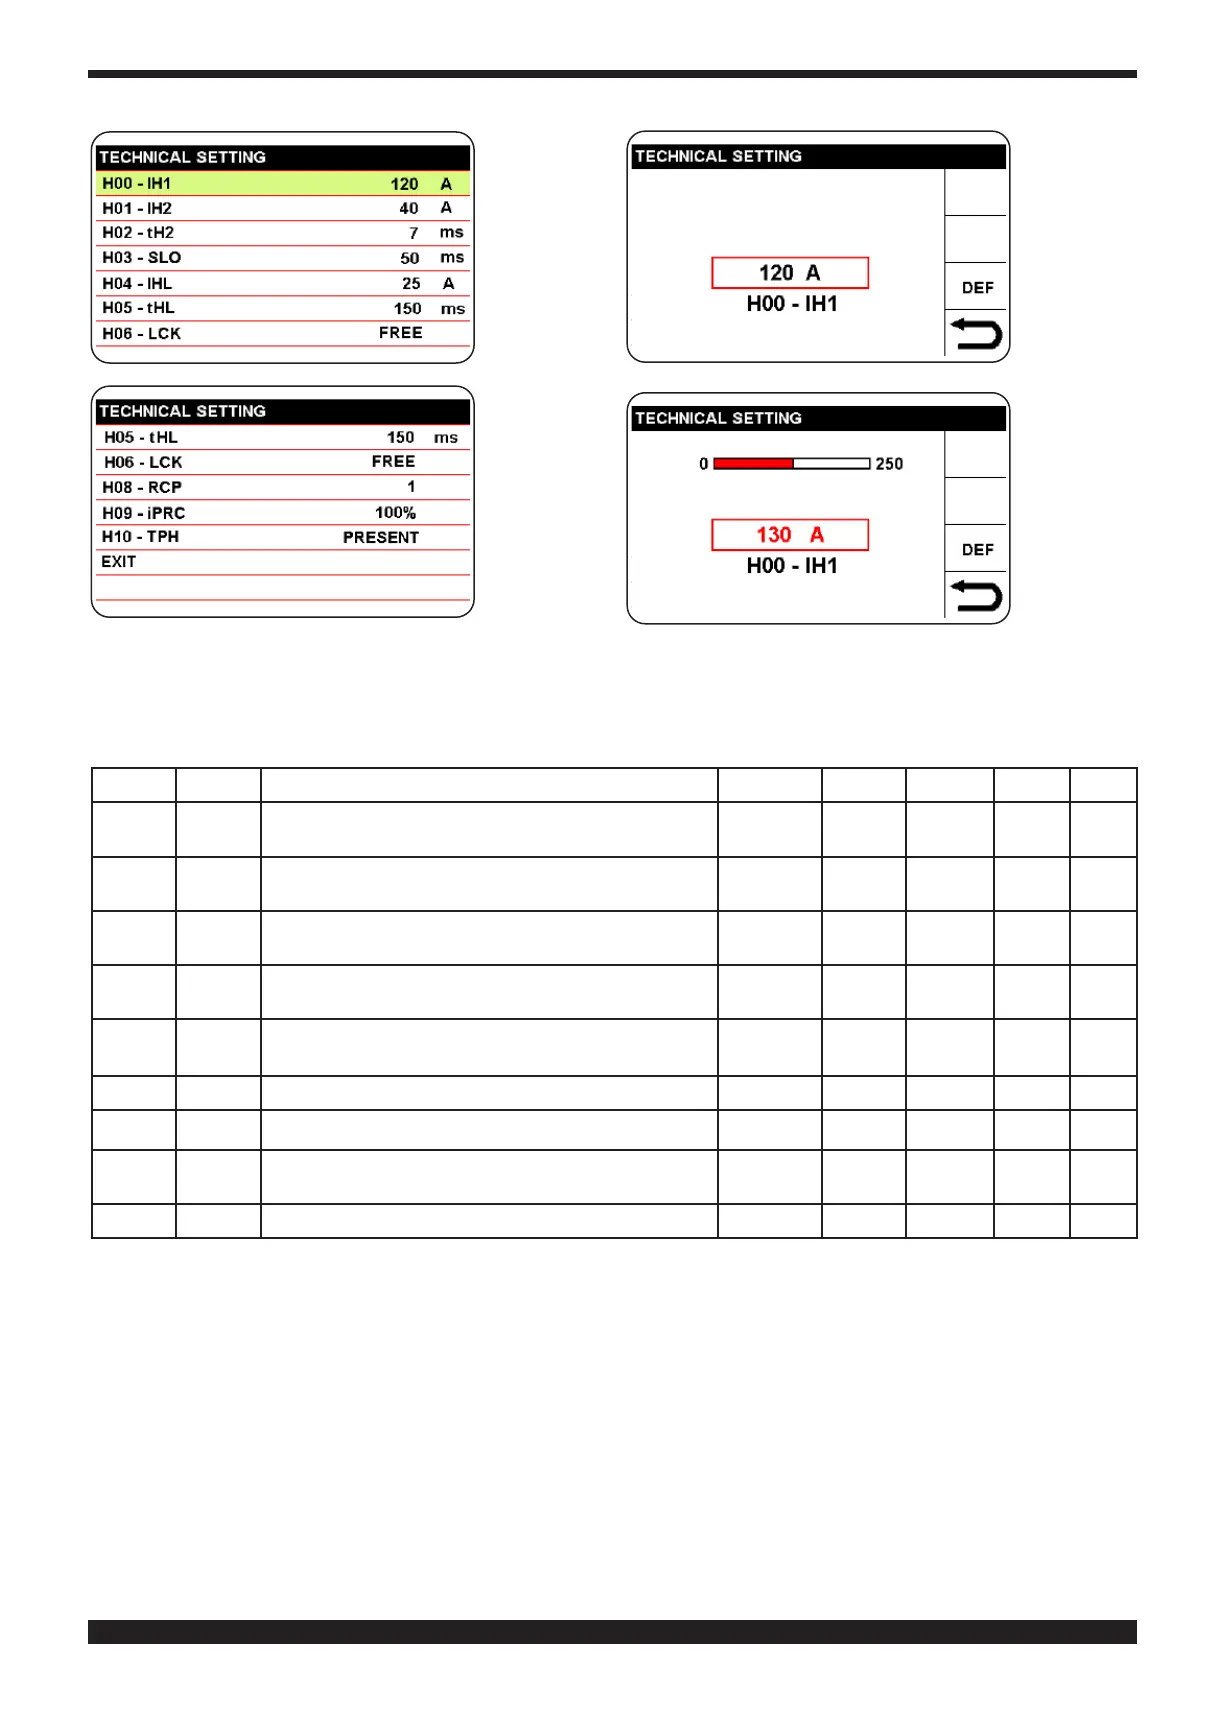
27
Select and
conrm the
par ameter
to modify.
The param-
eter is acti-
vated in red;
then press
knob B.
Turn knob
B to set the
selected
parameter;
then press
to conrm
the setting.
By adopting this method, it is possible to select, modi-
fyandconrmalltheweldingparameterswhichpresent
one after the other, and summarised in the following ta-
ble.
Description Min DEF Max U.M.
Sol.
H00
IH1 Amplitudeofhot-startrstcurrent (ignition with
HF)
0 120 220 A 1
H01
IH2 Amplitude of hot-start second current (ignition
with HF)
5 40 220 A 1
H02
tH2 Duration of hot-start second current (ignition with
HF)
0 7 250 ms 1
H03
SLO Gradientofhot-startttingwithrstweldingcur-
rent
1 50 100 ms 1
H04
IL1 Amplitude of hot-start current (ignition striking/
lift)
5 25 100 A 1
H05
tL1 Duration of hot-start current (ignition striking/lift) 0 150 200 ms 1
H06
LOC Panel setting lock down (free, total, partial) PARTIAL FREE TOTAL - -
H08
UDJ UP/DOWN handling during JOBS (OFF=not acti-
vated, 1=without roll, 2=with roll)
1 OFF 2 - 1
H09
LIM Current level range extension up to 400% 100 100 400 % -



 To Next Page