30
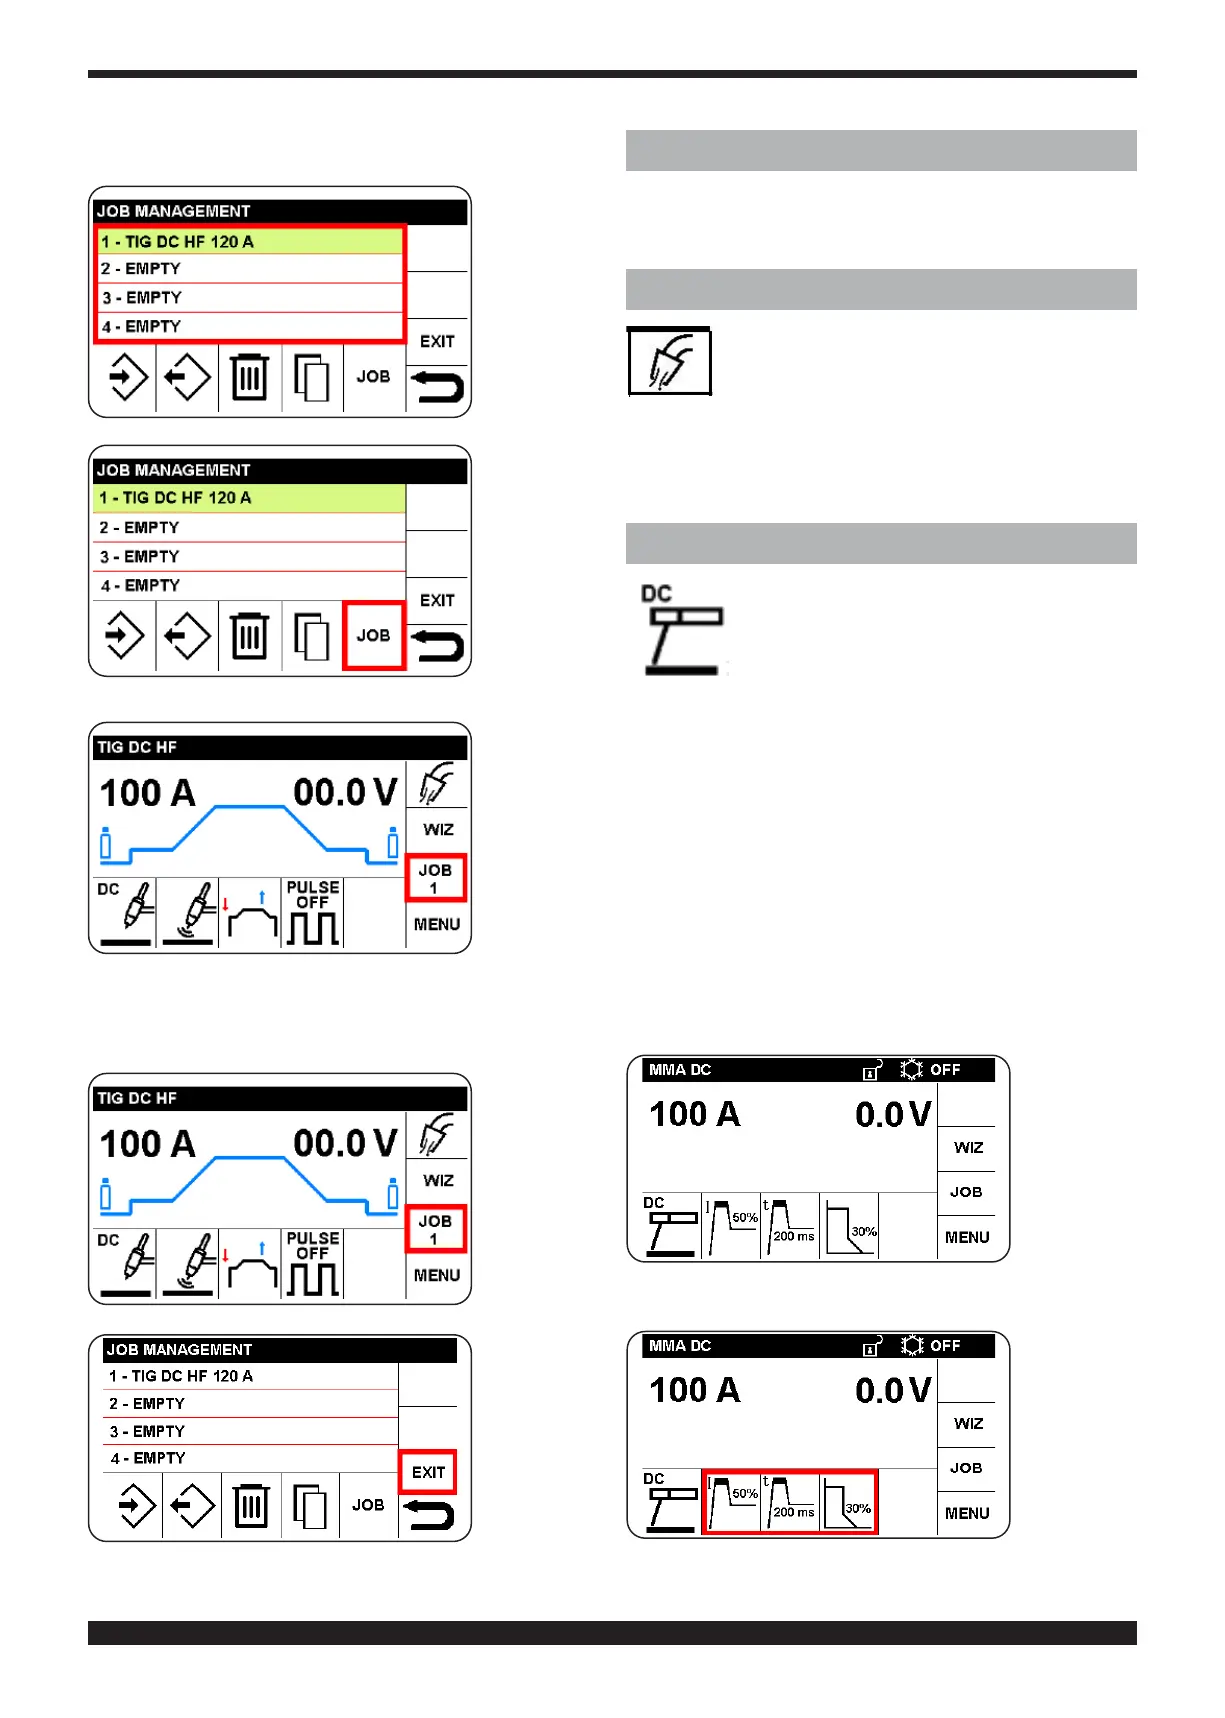
10.5 WELDING WITH A JOB
Access the JOB menu as described in 10.1
Select and
c o n f i r m
the desired
number.
Select and
conrm the
JOB sector.
The program
is available
for welding,
and no pa-
rameter can
bemodied.
To return to the main screen, press knob B (do not re-
lease immediately) (> 0.7 sec.)
10.6 LOGGING OFF FROM A JOB
Select and
conrm the
JOB1 sec-
tor.
Select and
conrm the
EXIT sector.
To return to the main screen, press knob B (do not re-
lease immediately) (> 0.7 sec.)
11 (SECTOR S)
This sector is positioned on the upper part of the display.
It provides in summary form the welding and cooling unit
settings, block and other functions.
12 TEST GAS (SECTOR T )
The function enables adjustment of the gas
ow . With the function activated, the elec-
tronically controlled valve opens. For 30 sec-
onds, the symbol glows, changing colour
every second; when the time ends, the electronically
controlled valve closes automatically; on pressing the
knob of the encoder during this time, the electronically
controlled valve closes.
13 WELDING WITH COVERED ELECTRODES (MMA)
This welding machine is suitable for welding
all types of electrodes, with the exception of
cellulosic (AWS 6010).
• Make sure that the G switch is in position
0, then connect the welding cables, observ-
ing the polarity required by the manufacturer of the elec-
trodes you will be using; also connect the clamp of the
ground cable to the workpiece, as close to the weld as
possible, making sure that there is good electrical con-
tact.
• Do not touch the welding torch or electrode clamp and
the ground clamp.
• Turn on the machine using the G switch.
• Select MMA Process
• Adjust the current based on the electrode diameter,
welding position and type of joint to be made.
• Always remember to shut off the machine and remove
the electrode from the clamp after welding.
To select this process, see chapter 5.
Adjust the
welding cur-
rent using
the knob B..
To modify the welding parameters, proceed as follows:
Select and
conrm the
sector rela-
tive to weld-
ing parame-
ters.



 To Next Page