Chapter 7 Introduction of Motion Flow
1-6
M-Series PLC Motion User Manual
7-6 Origin Return
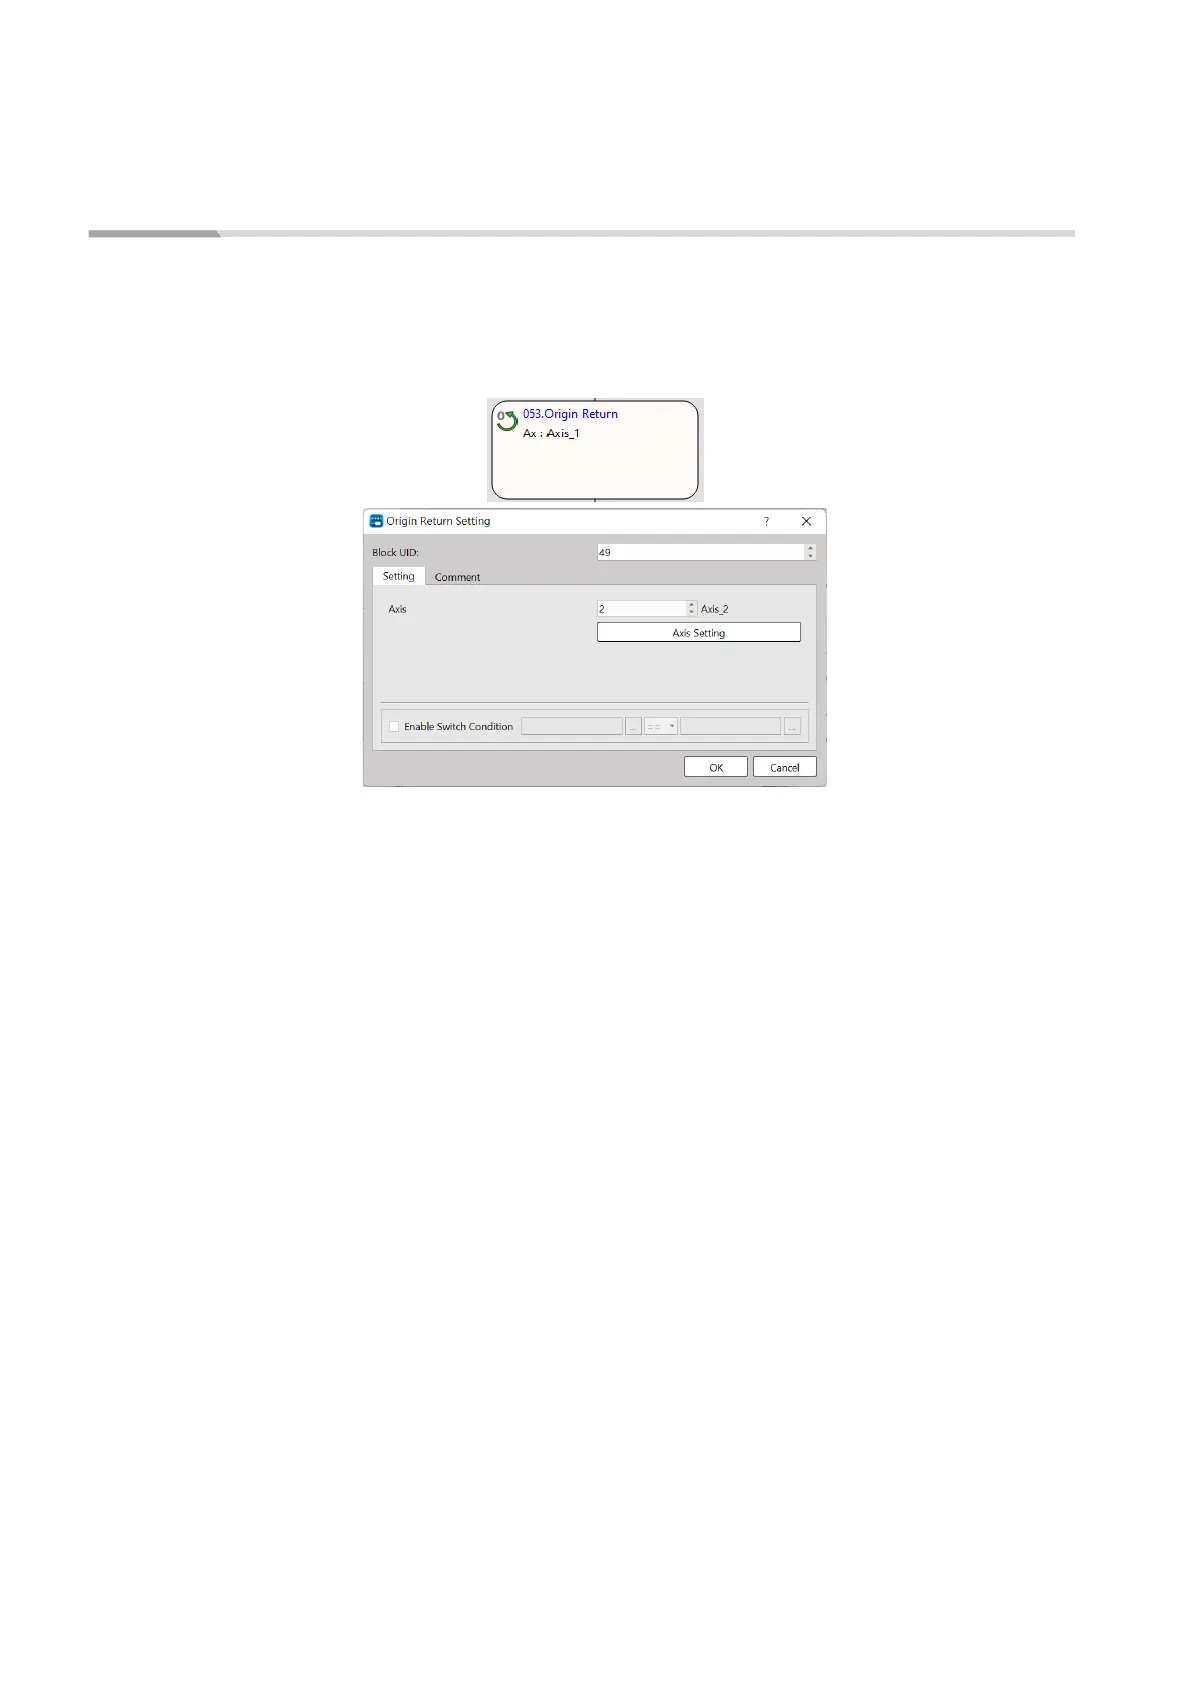
The function block is required for executing the Origin Return of the designated axis. As per the figure
below, reset the Origin for Axis_1. If the Origin is duly set, the axis will jump to next flow as soon as
M300=1 jumping condition is established.



 To Next Page