EasyManua.ls Logo

Jeep UNIVERSAL CJ-2A - Page 38

Jeep UNIVERSAL CJ-2A
281 pages
Print Icon
To Next Page IconTo Next Page
To Previous Page IconTo Previous Page
Loading...
'Jeep'
UNIVERSAL
and
'Jeep'
DISPATCHER
D
D-41.
Crankshaft
Main
Bearings
The
crankshaft
rotates
on
three
main
bearings
with
a
running
clearance
of
.0003"
to
.0029"
[.0008
a .0074 tnm.].
These
bearings
are
positioned
and
prevented
from
rotating
in
their
supports
in
the
cylinder
block
by
dowel
pins.
Dowel
pins
are
used
in
both
the
center
and
the
rear
bearing
caps.
No
dowel
pins
are
used
in
the
front
bearing
cap
be-
cause
the
bearing
has
a flange.
The
front
main
bear-
ing
takes
the
end
thrust
of
the
crankshaft.
The
main
bearings
are
of
premium
type
which
provides
long
bearing
life.
They
are
replaceable
and
when
correctly
installed,
provide
proper
clearance
with-
out
filing,
boring,
scraping,
or
shimming.
Crank-
shaft
bearings
can
be
removed
from
this
engine
only
with
the
engine
out
of
the
vehicle.
Crankshaft
bear-
ings
must
be
replaced
as
a
complete
set
of
three
bearings,
each
bearing
consisting
of
two
halves.
Main
bearings
are
available
in
the
standard
size
and
the
following
undersizes:
.001" [0,025
mm.]
.012"
[0,304
mm.]
.002" [0,050 mm.]
.020"
[0,508
mm.]
.010" [0,254
mm.]
.030"
[0,762
mm.]
The
.001"
and
.002"
undersize
main
bearings
are
for
use
with
standard
size
crankshafts
having
slightly
worn
journals.
The
.010", .020",
and
.030"
undersize
bearings
are
for
use
with
undersize
crankshafts
in
those
sizes.
The
.012"
undersize
bearings
are
for
use
with
.010"
undersize
crank-
shafts
having
slightly
worn
journals.
Bearing
sizes
are
rubber
stamped
on
the
reverse
side
of
each
bearing
half.
D-42.
Crankshaft
Main
Bearing Inspection
The
crankshaft
journals
must
be
carefully
inspected
as
detailed
previously
in
Par.
D-38.
Worn
journals
will
require
undersize
bearings.
Scored,
flaked,
or
worn
bearings
must
be
replaced.
Measure
the
main
bearing
bores
in
the
cylinder
block
using
a
telescope
gauge
and
micrometer.
Measure
the
bores
at
right
angles
to
the
split
line
and
at
45°
to
the
split
line.
The
bores
should
not
be
over
.001"
[0,025 mm.]
out-of-round
or
.001"
in
taper
from
end
to
end.
Also,
the
bores
should
not
be
more
then
.001"
oversize,
considering
the
average
diameter
of
the
bore.
D-43.
Fitting
Crankshaft
Main
Bearings
Fit
the
crankshaft
main
bearings
using
either
"Plastigage"
or
shim
stock.
Refer
to
the
instruc-
tions
in
Section
E
for
"Plastigage"
(Par.
E-46)
or
shim
stock
(Par.
E-47).
I
D-44.
Connecting
Rod Bearings
The
connecting
rod
bearings,
like
the
crankshaft
main
bearings,
are
of
the
replaceable
type.
When
correctly
installed,
the
bearings
provide
proper
clearance
without
filing,
boring,
scraping,
or
shimming.
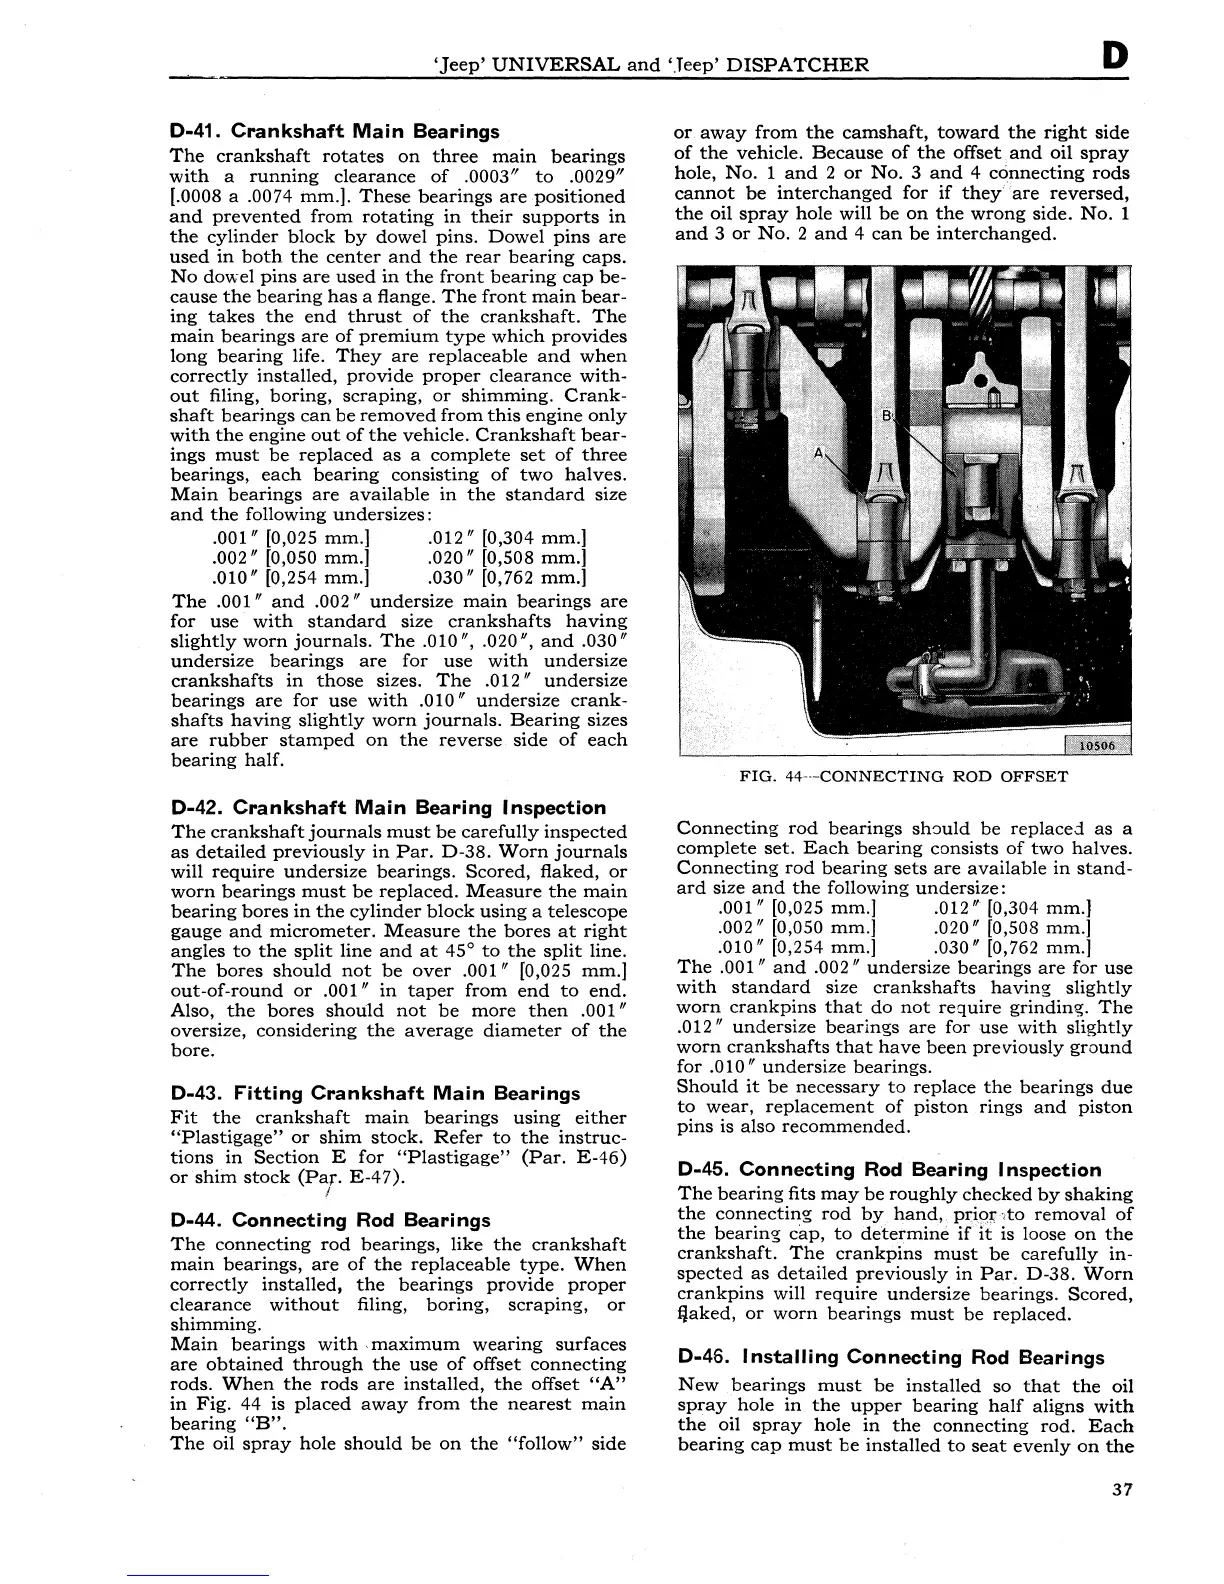
Main
bearings
with
.maximum
wearing
surfaces
are
obtained
through
the
use
of
offset
connecting
rods.
When
the
rods
are
installed,
the
offset
"A"
in
Fig.
44 is
placed
away
from
the
nearest
main
bearing
"B".
The
oil
spray
hole
should
be
on
the
"follow"
side
or.
away
from
the
camshaft,
toward
the
right
side
of
the
vehicle.
Because
of
the
offset._
and
oil
spray
hole,
No.
1
and
2
or
No.
3
and
4
connecting rods
cannot
be
interchanged
for
if
they··'are
reversed,
the
oil
spray
hole
will
be
on
the
wrong
side.
No.
1
and
3
or
No.
2
and
4
can
be
interchanged.
FIG.
44---CONNECTING
ROD
OFFSET
Connecting
rod
bearings
sh::mld
be
replaced
as
a
complete
set.
Each
bearing
consists
of
two
halves.
Connecting
rod
bearing
sets
are
available
in
stand-
ard
size
and
the
following
undersize:
.001" [0,025 mm.] .012" [0,304
mm.]
.002"
[0,050
mm.]
.020" [0,508 mm.]
.010"
[0,254 mm.]
.030"
[0,762 mm.]
The
.001"
and
.002"
undersize
bearings
are
for
use
with
standard
size
crankshafts
having
slightly
worn
crankpins
that
do
not
require
grindinf;!;.
The
.012"
undersize
bearings
are
for
use
with
slightly
worn
crankshafts
that
have
been
previously
ground
for
.010"
undersize
bearings.
Should
it
be
necessary
to
replace
the
bearings
due
to
wear,
replacement
of
piston
rings
and
piston
pins
is
also
recommended.
D-45.
Connecting
Rod Bearing Inspection
The
bearing
fits
may
be
roughly
checked
by
shaking
the
connecting
rod
by
hand,
px;iO,F
1to
removal
of
the
bearing
cap,
to
determine
ifit
is loose
on
the
crankshaft.
The
crankpins
must
be
carefully
in-
spected
as
detailed
previously
in
Par.
D-38.
Worn
crankpins
will
require
undersize
bearings.
Scored,
ijaked,
or
worn
bearings
must
be
replaced.
D-46.
Installing
Connecting
Rod Bearings
New
bearings
must
be
installed
so
that
the
oil
spray.
hole
in
the
upper
bearing
half
aligns
with
the
oil
spray
hole
in
the
connecting
rod.
Each
bearing
cap
must
be
installed
to
seat
evenly
on
the
37