EasyManua.ls Logo

Jeep UNIVERSAL CJ-2A - Page 41

Jeep UNIVERSAL CJ-2A
281 pages
Print Icon
To Next Page IconTo Next Page
To Previous Page IconTo Previous Page
Loading...
D
L4-134
ENGINE
NOTE:
When
using
a
spring
checking
fixture
as
shown
in
Fig.
46,
it
is
necessary
to
convert
the
torque
wrench
reading
which
is
in
pounds-feet
to
the
static
pound
pressure
specified
above
according
to
the
instructions
furnished
with
the
wrench.
For
example;
should
the
torque
wrench
reading
be
50
lb-ft.
and
the
wrench
is
two
feet
long
the
static
pressure
of
the
spring
will
be
50 x 2
or
100 lbs.
Clean
the
valve
guides
with
a
standard
valve
guide
cleaner
or
a wire
brush.
Check
the
valve
guides
in
the
cylinder
block.
Replace
valve
guides
which
are
broken
or
worn
enough
to
cause
excessive
valve
'Stem-to-guide
clearance.
See
Par.
D-58.
Standard
intake
valve
clearance
is
.0015
to
.00325"
[0,038
a 0,083 mm.}
and
the
exhaust
valve
clearance
is .0025"
to
.0045" [0,0635 a 0,1143 mm.].
Excessive
clearance
between
the
valve
stems
and
guides
will
cause
improper
seating
and
burned
valves.
When
there
is a.
tendency
to
draw
oil
vapor
through
the
guide
causing
excessive oil
consumption,
fouled
spark
plugs,
and
poor
low-speed
performance.
To
check
the
clearance
of
the
valve
stem
to
the
valve
guide,
take
a
new
valve
and
place.
in
each
valve
guide.
Check
the
clearance
with
a
sUltably
mounted
dial
indicator
or
feel
the
clearance
by
moving
the
valve
stem
back
and
forth.
If
this
check
shows
excessive
clearance
it
will
be
necessary
to
replace
the
valve
guide.
D-55. Refacing Valves ,
Reface
the
valves
with
a
valve
refacer.
The
valve
refacer
manufacturer's
instructions
should
be
fol-
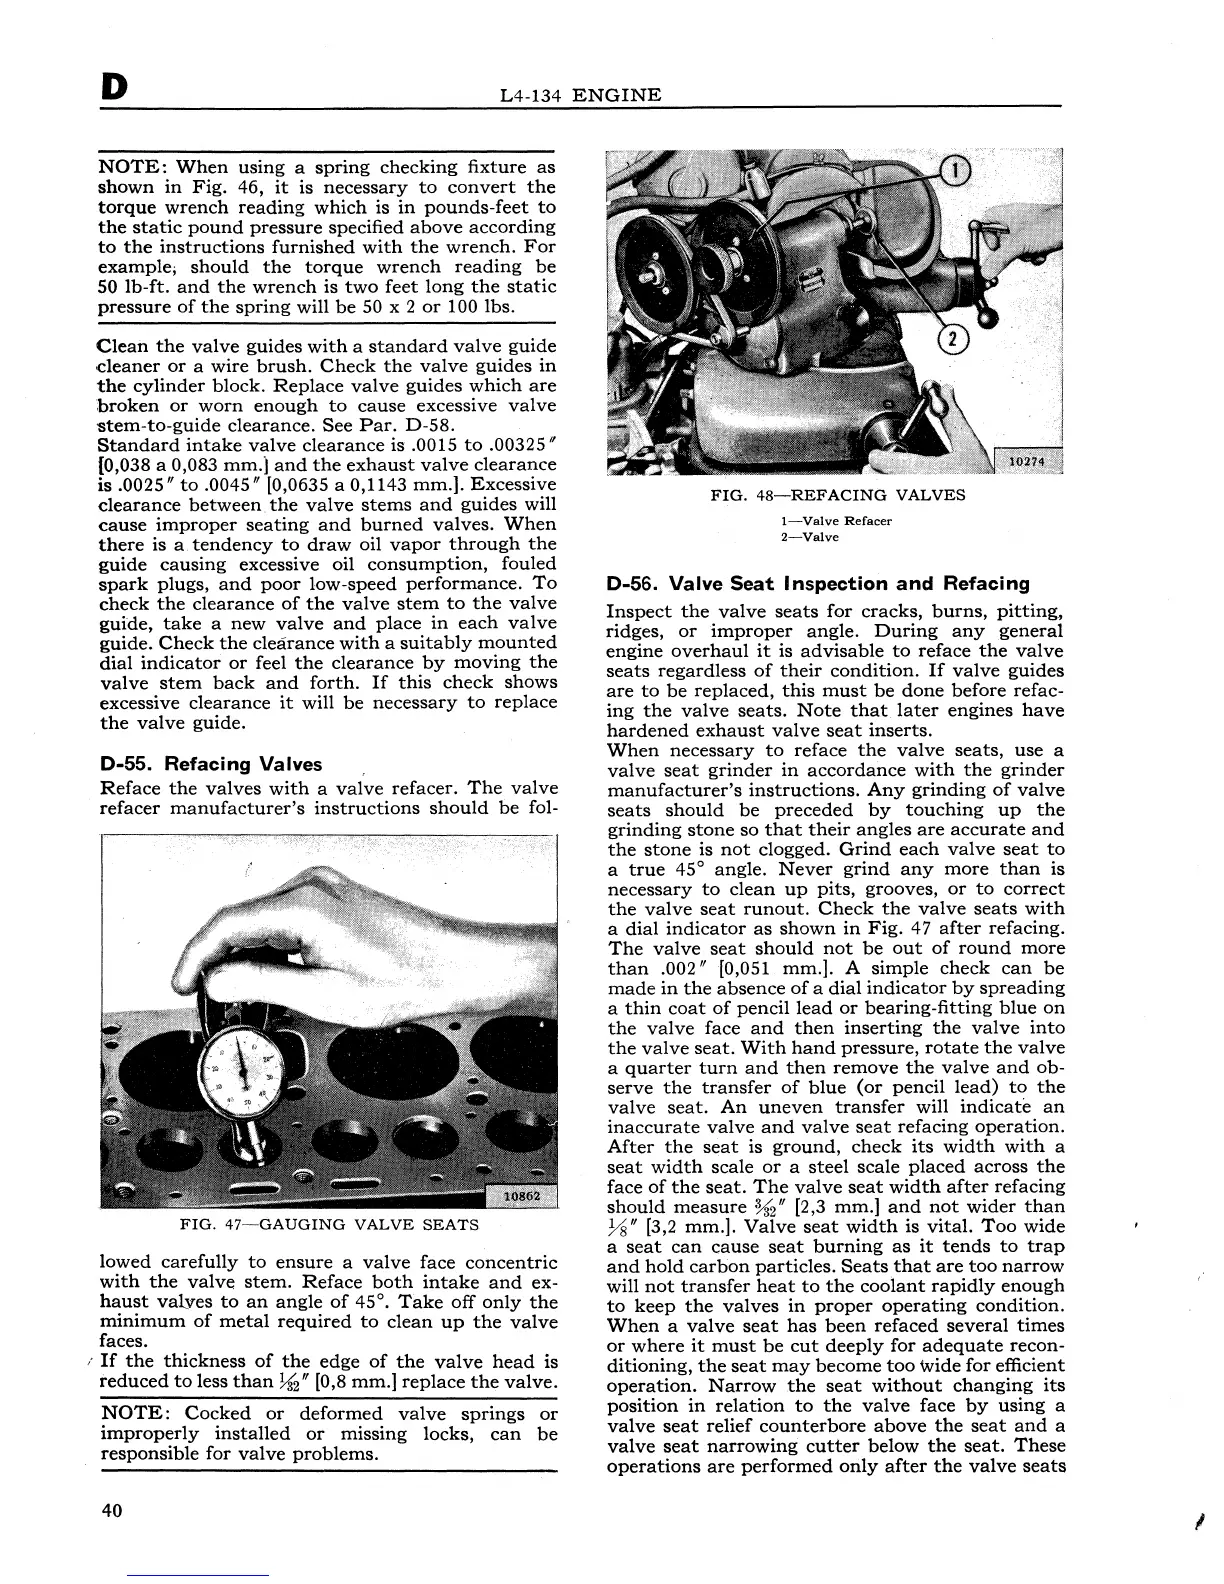
FIG.
47-GAUGING
VALVE
SEATS
lowed
carefully
to
ensure
a
valve
face
concentric
with
the
valve
stem.
Reface
both
intake
and
ex-
haust
val_ves
to
an
angle
of
45
o.
Take
off
only
the
minimum
of
metal
required
to
clean
up
the
valve
faces.
r
If
the
thickness
of
the
edge
of
the
valve
head
is
reduced
to
less
than~"
[0,8 mm.]
replace
the
valve.
NOTE:
Cocked
or
deformed
valve
springs
or
improperly
installed
or
missing locks,
can
be
responsible
for
valve
problems.
40
FIG.
48-REFACING
VALVES
1-Valve
Refacer
2-Valve
D-56. Valve
Seat
Inspection
and
Refacing
Inspect
the
valve
seats
for
cracks,
burns,
pitting,
ridges,
or
improper
angle.
During
any
general
engine
overhaul
it
is
advisable
to
reface
the
valve
seats
regardless
of
their
condition.
If
valve
guides
are
to
be
replaced,
this
must
be
done
before
refac-
ing
the
valve
seats.
Note
that
later
engines
have
hardened
exhaust
valve
seat
inserts.
When
necessary
to
reface
the
valve
seats,
use
a
valve
seat
grinder
in
accordance
with
the
grinder
manufacturer's
instructions.
Any
grinding
of
valve
seats
should
be
preceded
by
touching
up
the
grinding
stone
so
that
their
angles
are
accurate
and
the
stone
is
not
clogged.
Grind
each
valve
seat
to
a
true
45° angle.
Never
grind
any
more
than
is
necessary
to
clean
up
pits,
grooves,
or
to
correct
the
valve
seat
runout.
Check
the
valve
seats
with
a
dial
indicator
as
shown
in
Fig.
47
after
refacing.
The
valve
seat
should
not
be
out
of
round
more
than
.002" [0,051 mm.]. A
simple
check
can
be
made
in
the
absence
of
a
dial
indicator
by
spreading
a
thin
coat
of
pencil
lead
or
bearing-fitting
blue
on
the
valve
face
and
then
inserting
the
valve
into
the
valve
seat.
With
hand
pressure,
rotate
the
valve
a
quarter
turn
and
then
remove
the
valve
and
ob-
serve
the
transfer
of
blue
(or
pencil
lead)
to
the
valve
seat.
An
uneven
transfer
will
indicate
an
inaccurate
valve
and
valve
seat
refacing
operation.
After
the
seat
is
ground,
check
its
width
with
a
seat
width
scale
or
a
steel
scale
placed
across
the
face
of
the
seat.
The
valve
seat
width
after
refacing
should
measure
%2"
[2,3 mm.]
and
not
wider
than
Ys"
[3,2 mm.].
Valve
seat
width
is
vital.
Too
wide
a
seat
can
cause
seat
burning
as
it
tends
to
trap
and
hold
carbon
particles.
Seats
that
are
too
narrow
will
not
transfer
heat
to
the
coolant
rapidly
enough
to
keep
the
valves
in
proper
operating
condition.
When
a
valve
seat
has
been
refaced
several
times
or
where
it
must
be
cut
deeply
for
adequate
recon-
ditioning,
the
seat
may
become
too
wide
for
efficient
operation.
Narrow
the
seat
without
changing
its
position
in
relation
to
the
valve
face
by
using
a
valve
seat
relief
counterbore
above
the
seat
and
a
valve
seat
narrowing
cutter
below
the
seat.
These
operations
are
performed
only
after
the
valve
seats