cmha2p11
cmha2p10
-- 2 2 --
bh32d1e
6.5 MMA welding
Arc 151i / 201i gives direct current, and you can weld most metals to alloy and non--
alloy steel, stainless steel and cast iron.
Arc 151i / 201i allows you to weld most coated electrodes from Ø 1.6 to Ø 3.25.
MMA welding may also be referred to as welding with coated electrodes. Striking the arc
melts the electrode, and its coating forms protective slag.
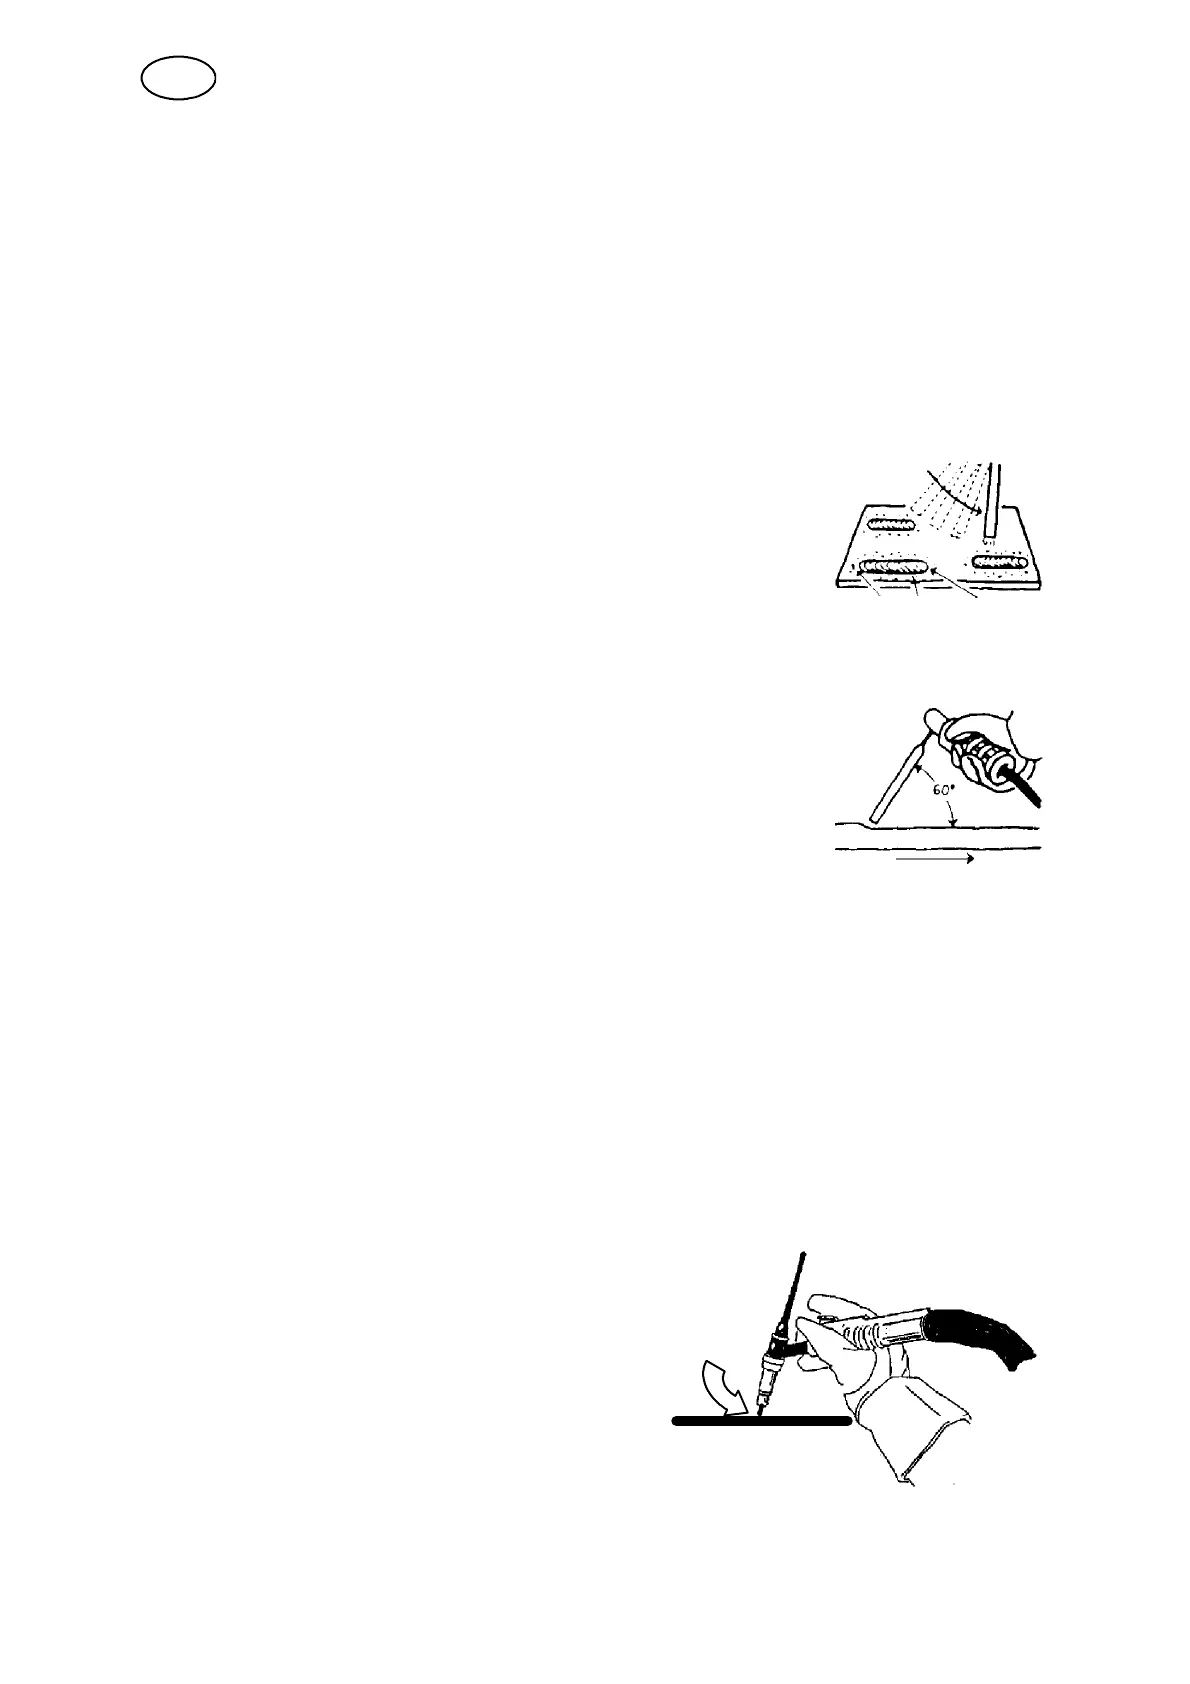
If, when striking the arc, the tip of the electrode is pressed against the metal, it immedi-
ately m elts and sticks to the metal, rendering continued welding impossible.
Therefore, the arc has to be struck in the same way that you would light a match.
Quickly strike the electrode against the metal, then raise it so
as to give an appropriate arc length ( approx. 2 mm). If the arc
is too long, it will crackle and spit before f inally going out com-
pletely.
If you are working on a welding bench, check before attempting
to strike the arc that residual waste metal, pieces of electrode
or other objects on the bench do not insulate the part to be
welded.
Once the arc has been struck, move the electrode from left to
right. The electrode must be at an angle of 60˚ to the metal in
relation to the direction of welding.
When you want to weld wide beads, or when you want the weld
to be so thick that you have to weld in a number of layers, how-
ever, you have to use lateral movements.
6.6 TIG welding
TIG welding melts the metal of the workpiece, using an arc struck from a tungsten
electrode, which does not itself melt. The weld pool and the electrode are protected
by shielding gas.
TIG welding is particularly useful where high quality is demanded and for welding
thin plate. Arc 151i / 201i also has good characteristics for TIG welding.
In order to TIG weld Arc 151i / 201i must be equipped with:
S a TIG torch with gas valve
S a welding gas cylinder (a suitable welding gas)
S a welding gas regulator (suitable gas regulator)
S tungsten electrode
S suitable auxiliary material, if necessary.
TIG scrape start (only A31)
To scrape start lightly scrape the tungsten
electrode against the workpiece to create an
arc.
GB






 To Next Page