6 CONTROL PANEL
0463 479 001
- 33 -
© ESAB AB 2017
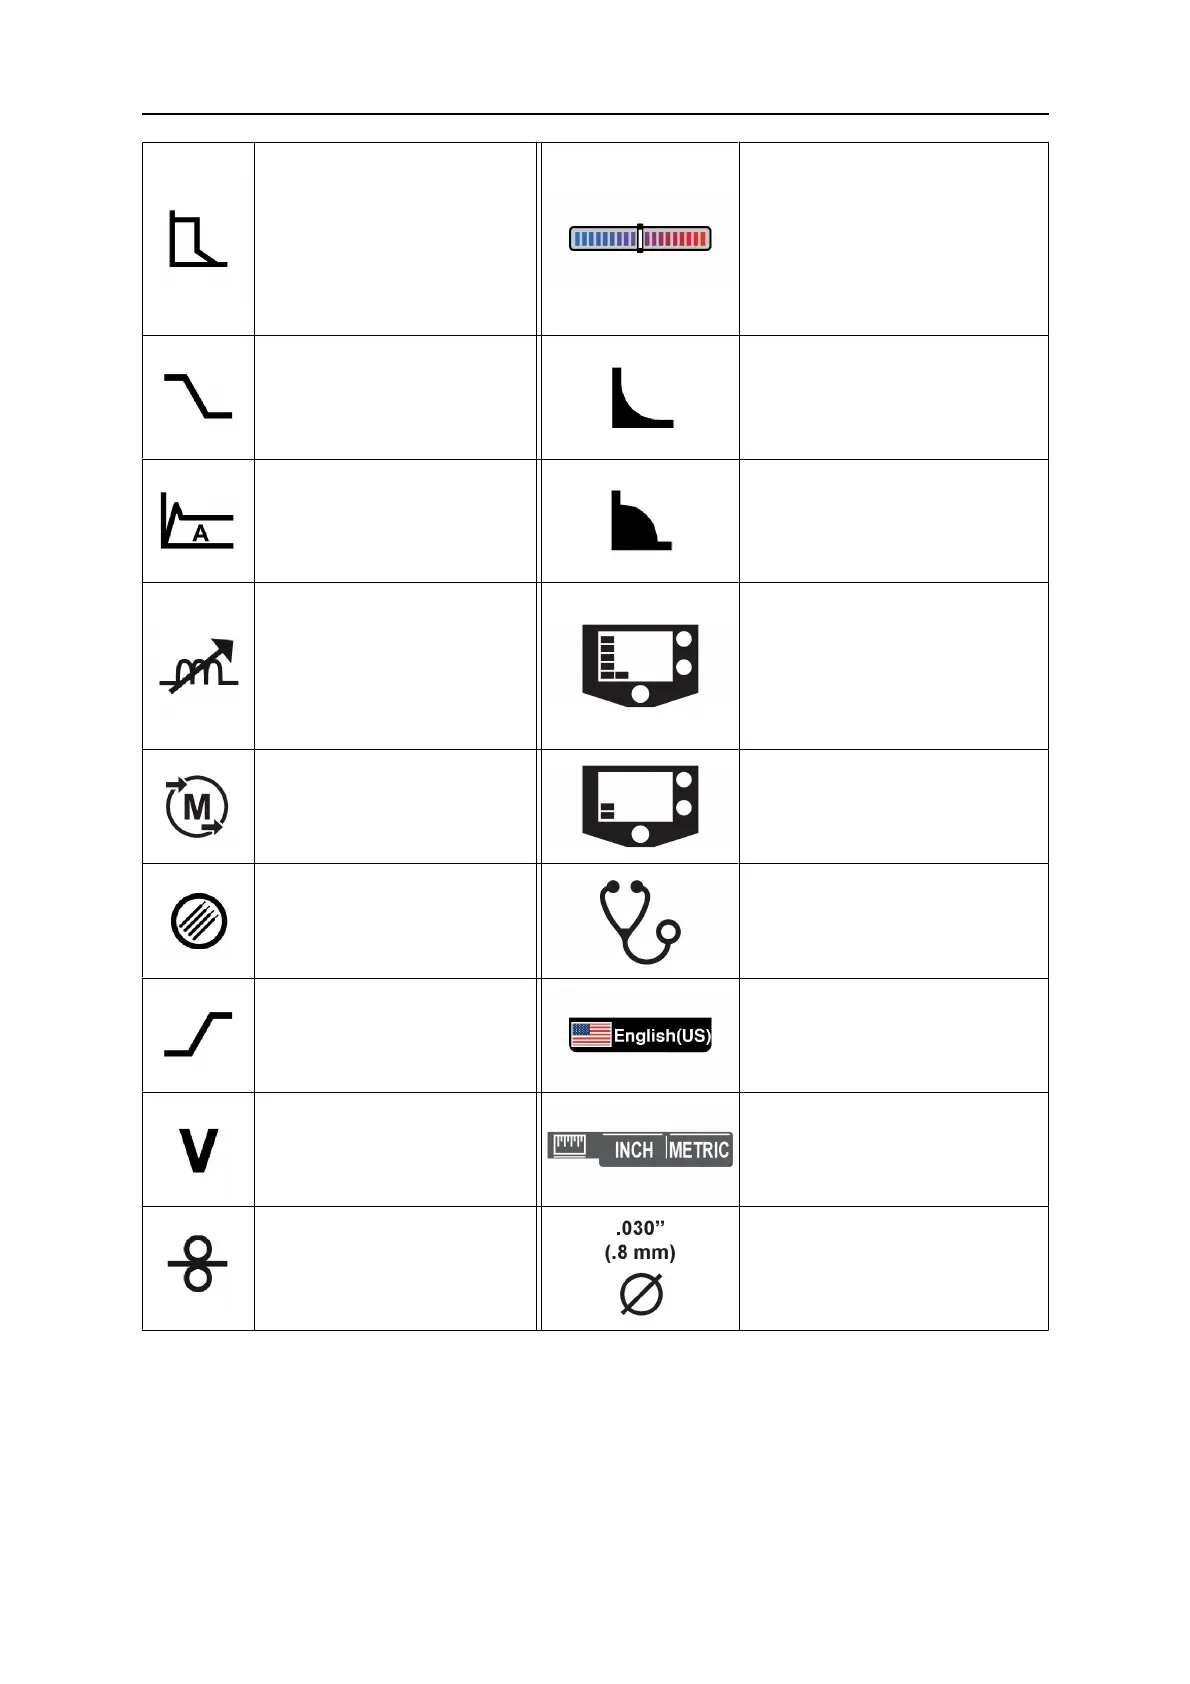
Arc force On stick
welding-increasing amps
when the arc length is
shortened to reduce or
eliminate the freezing of the
stick electrode in the weld
puddle
Trim bar Changing the weld
bead profile from flat to convex
or flat to concave
Downslope Sloping the
current down over a period
of time at the end of the
weld cycle
Bead profile, concave
Hot start The increase of
amps when striking the
electrode to reduce sticking
Bead profile, convex
Inductance The addition of
inductance into the arc
characteristics to stabilize
the arc and reduce spatter
when in the short circuit
process
Advanced Settings
Memory, able to save
welding programs for a
specific application
Basic Settings
Stick electrode choice Diagnostics
Upslope, Sloping the
current up over a period of
time at the beginning of the
weld cycle
Language selection
Volts Unit of Measure
Wire feed speed Wire diameter


 To Next Page