G9742 Metal Cutting Bandsaw (Mfg. Since 11/06
-21-
Feed Rate
The speed at which the saw blade will cut through
a workpiece is controlled by blade type and feed
rate.
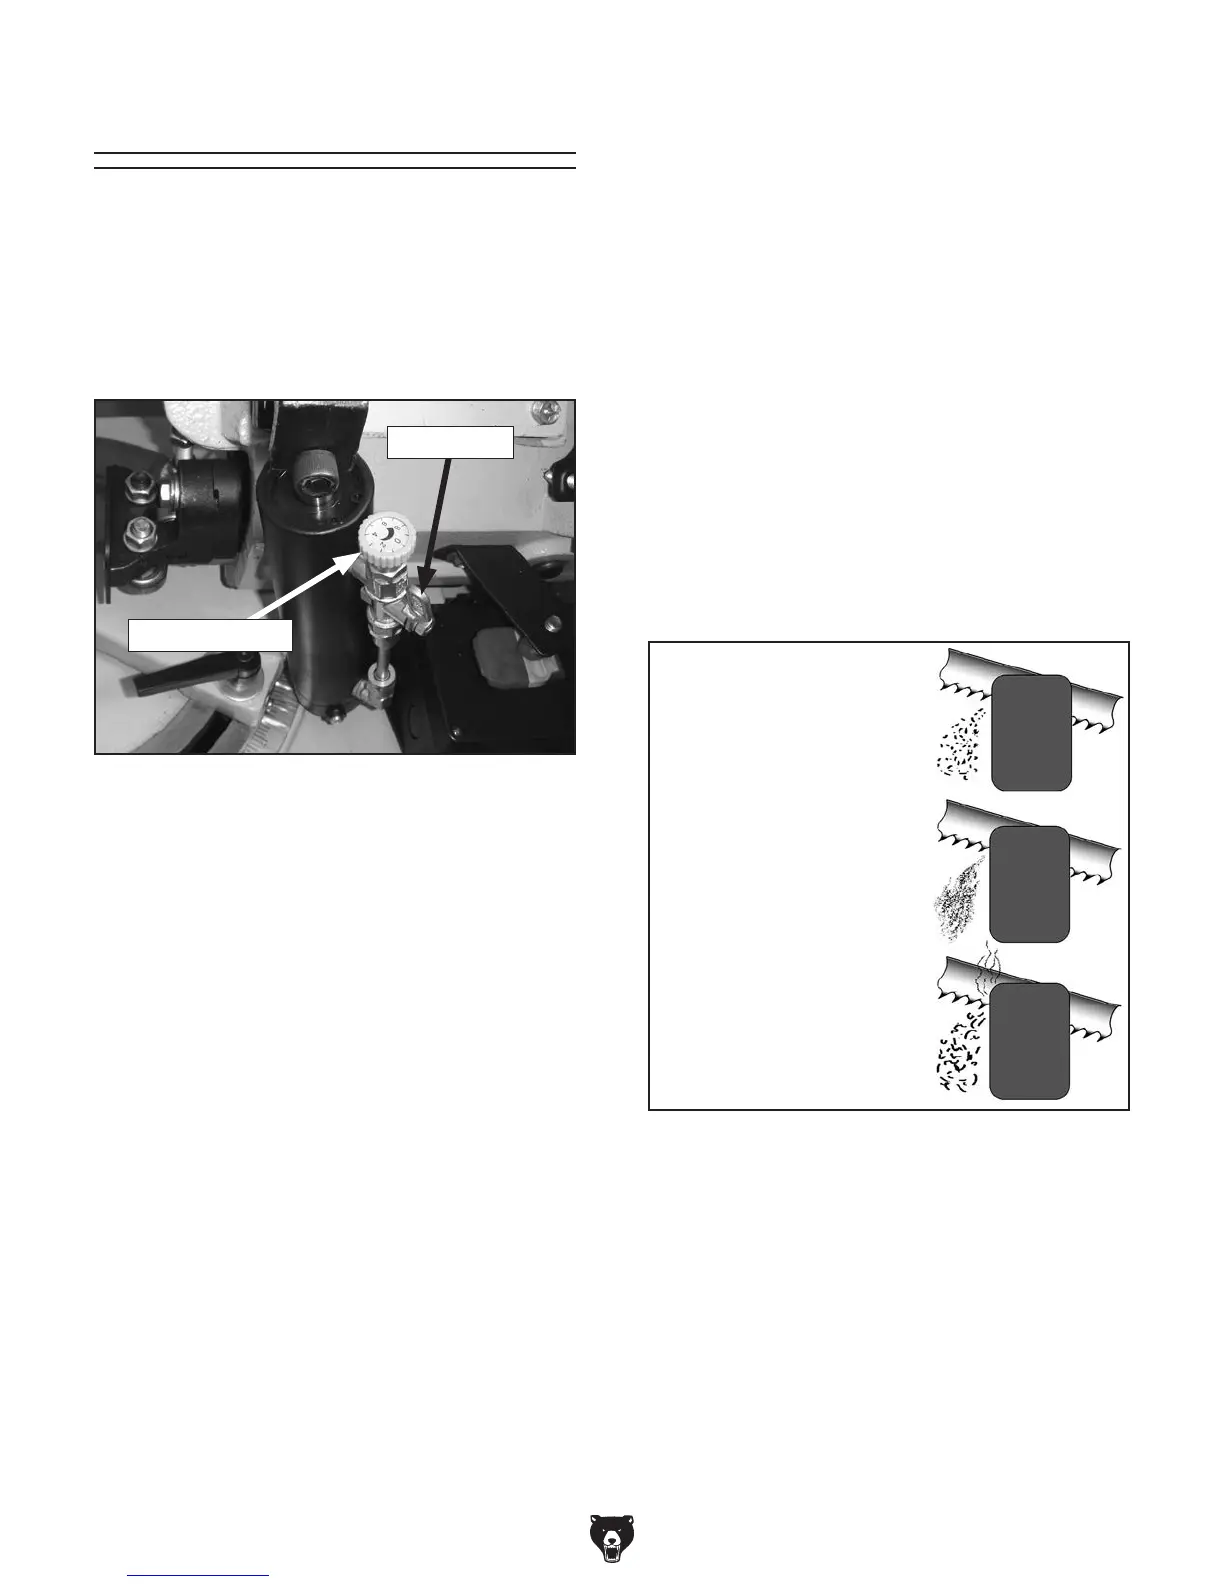
The feed rate is controlled by the valve lever and
feed rate dial on the hydraulic cylinder shown in
Figure 22.
To set the feed rate:
1. Raise the headstock and turn the valve lever
sideways (horizontally).
2. Clamp the workpiece in the table vise.
3. Move the headstock and blade a few inches
above the workpiece.
4. With the correct saw blade installed and
blade speed selected, turn the saw ON.
5. Slowly rotate the feed rate dial to a conserva-
tive feed rate until the saw begins to cut the
workpiece.
6. Observe the chips that exit the cut, and
increase or decrease the feed rate according
to the chip characteristics (see Figure 23).
Chips are silvery,
thin, small, or
powdery: Increase
feed rate.
Chips are large,
curled, blue or
brown, or smoking:
Decrease feed rate.
Chips are width
of tooth, thin and
curled, and silvery:
Optimum speed and
feed rate.
Figure 23. Reading chips.
Figure 22. Bandsaw feed rate control.
Valve Lever
Feed Rate Dial
Turning the valve lever in-line with the piping (as
shown in the Figure 22) opens it up, which allows
the fluid to circulate and allows the head to move.
Turning the valve lever sideways or perpendicular
to the pipiing closes it, which locks the headstock
in place.
The feed rate dial controls the amount of fluid that
circulates around the hydraulic cylinder, which in
turn, controls the speed that it moves.


 To Next Page