CHAPTER 8: OPERATION 8-15
EXPRESS 332 S2
4.2.2. Application setup
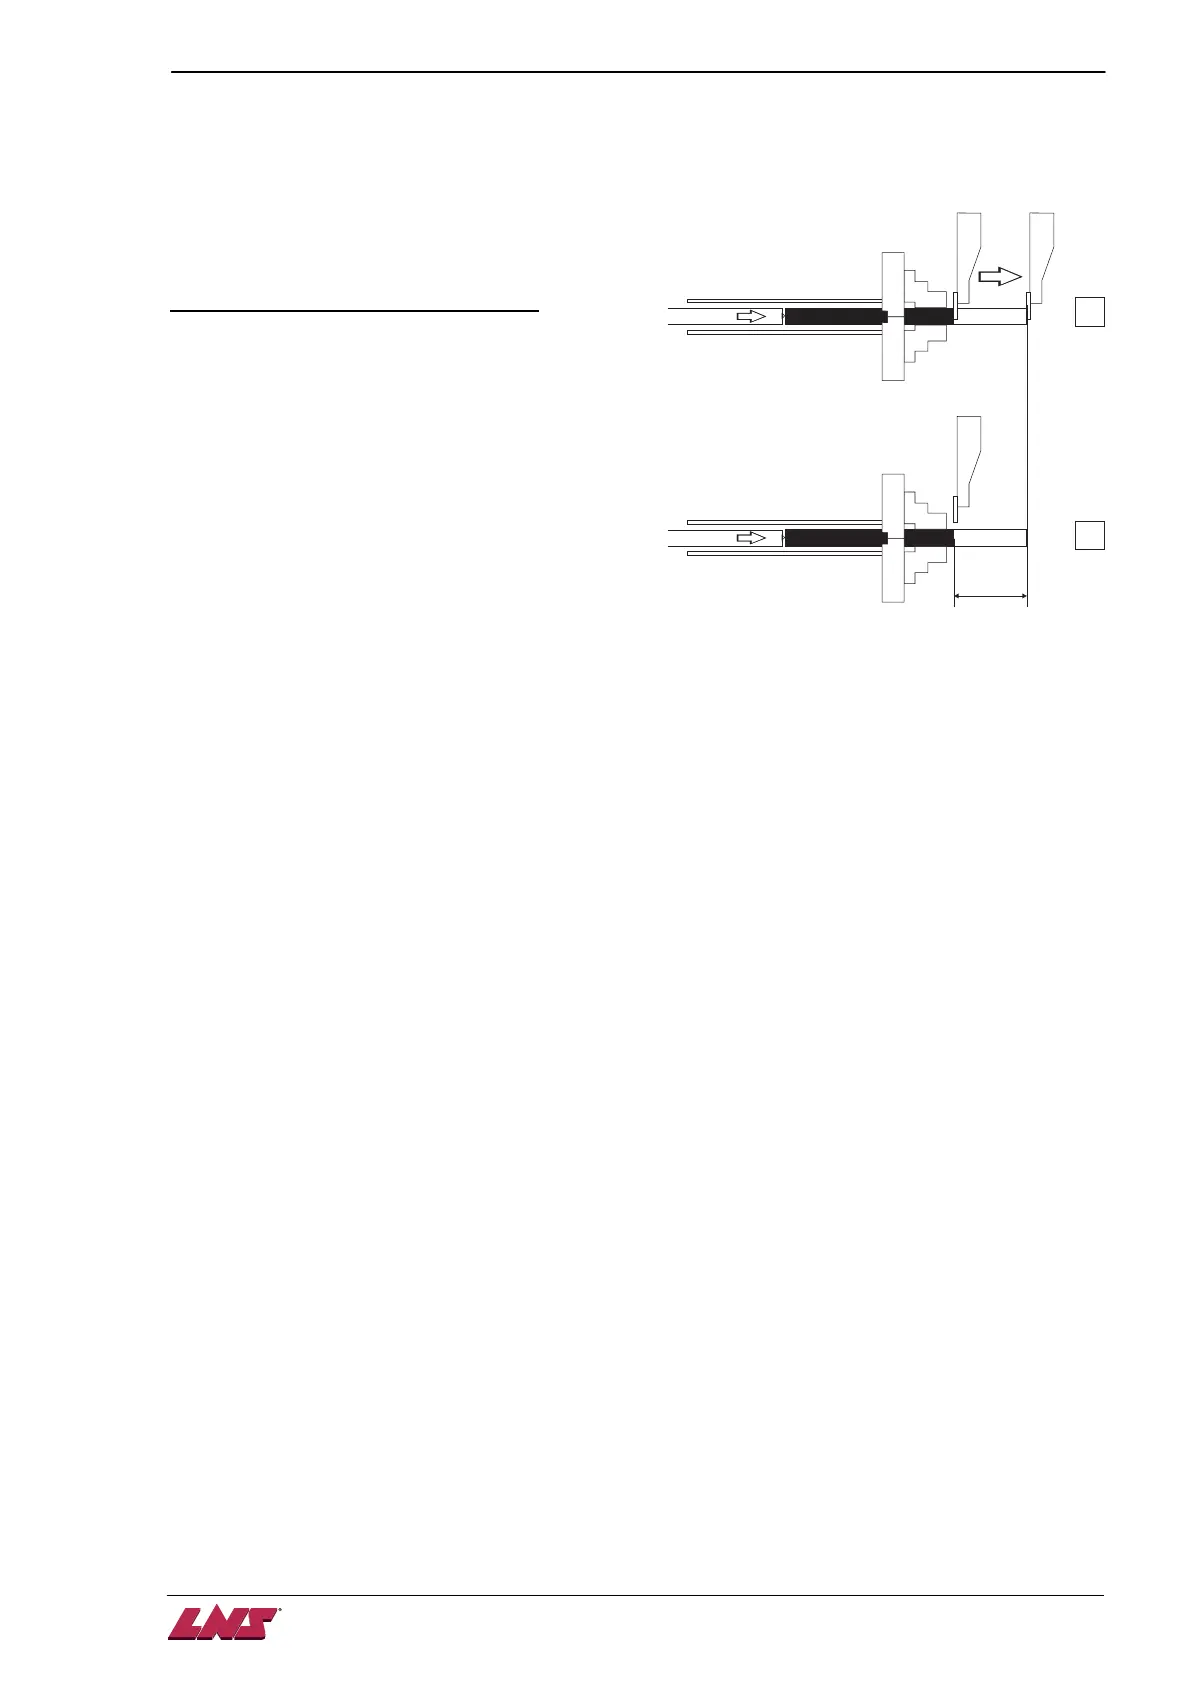
Part feed out with turret
This parameter determines whether the lathe or the
bar feed will control the positioning of the part.
Additional parameter (may be not visible):
a) The turret is parked in position:
the turret travels to the point the bar stock will be
pushed to and waits that the bar feed has pushed
the material to this point.
b) The turret is moving to position:
The turret comes to the bar stock end; the bar
feed starts pushing against the turret. Then, the
turret moves to the desired feeding length, the bar
feed still maintaining the bar stock pressure
against the turret.
Part feed out without turret
The bar feed drives the feeding cycle. When the clamping device opens, the bar feed pushes the bar
stock according to the parameter "overall part length" value. The bar feed is not able to drive the feeding
cycle if the machining process requires several clamping device openings.
Part feed out with M-function (may be not visible)
This parameter is used to deactivate the M function receipt of the turret if this function is not used in the
lathe interface. In this case, a timer can be used to give the receipt.
Dry Run (may be not visible)
This function allows the lathe to run without the bar feeder, ex.: hand loading pieces, etc.


 To Next Page