OM-225 590 Page 29
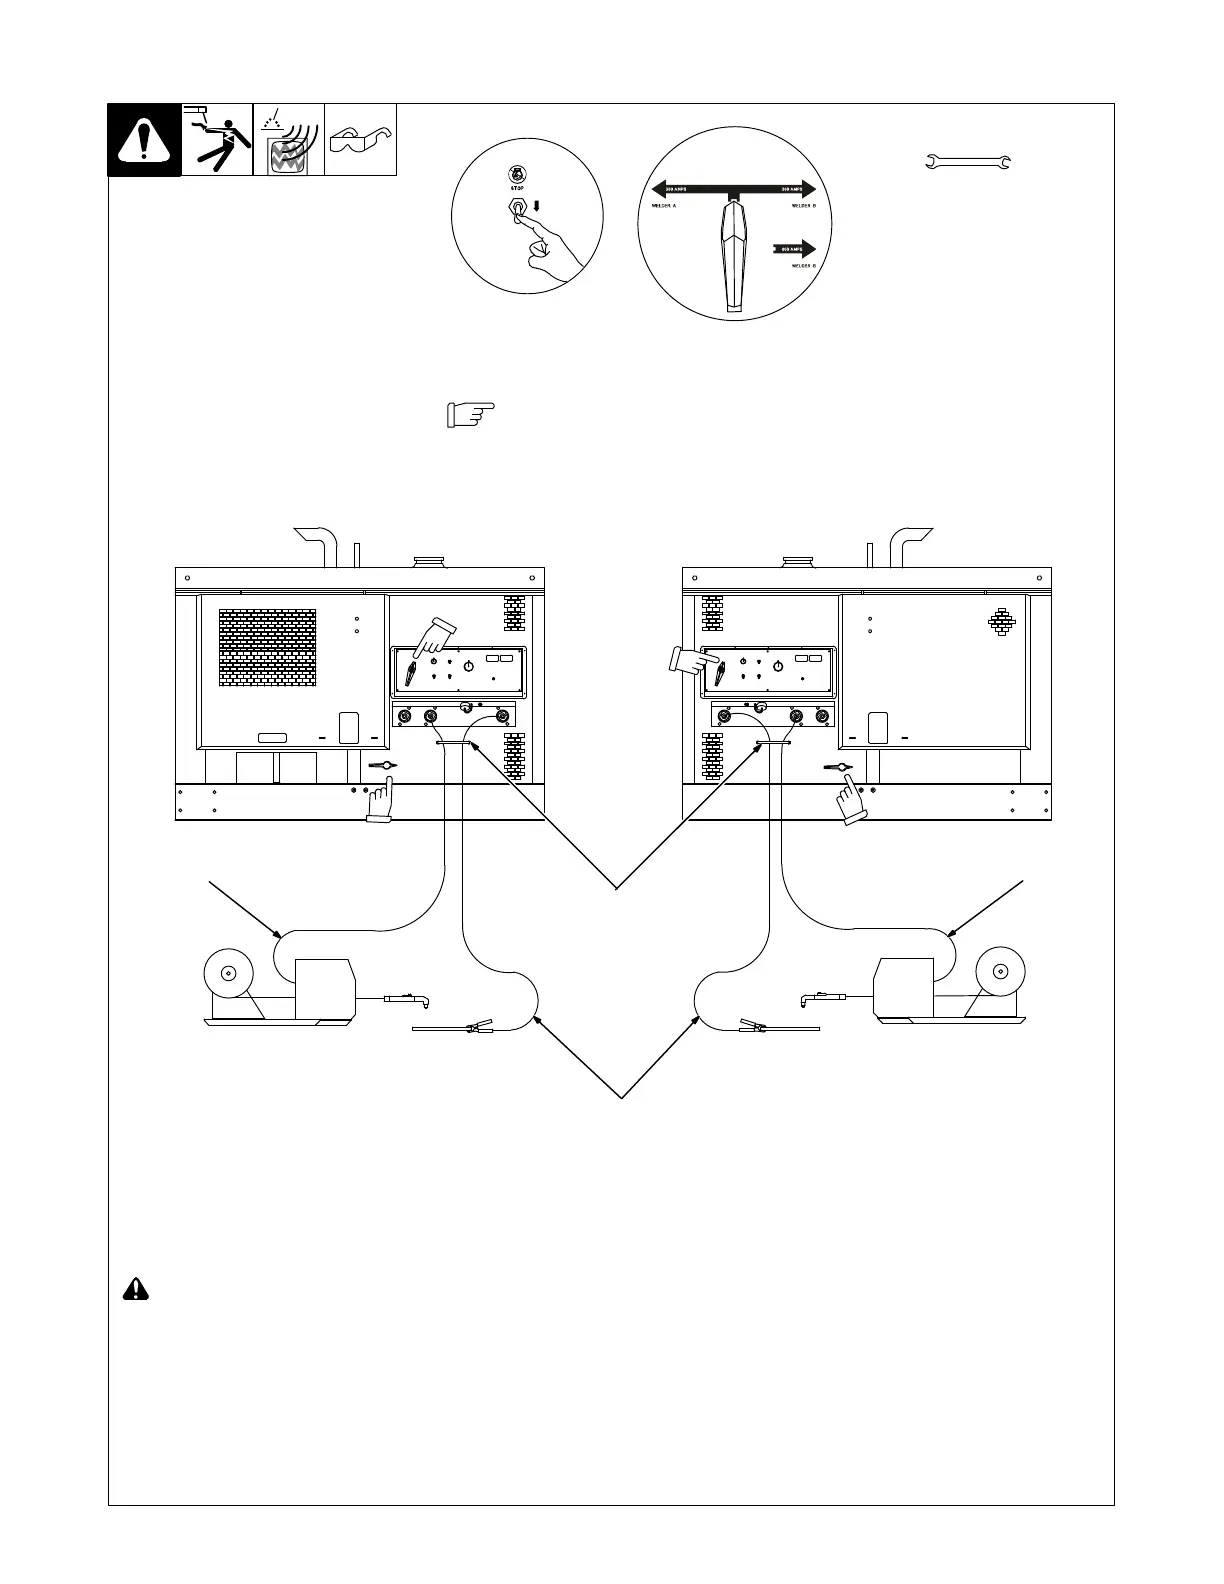
5-12. Making Dual Operator CV Weld Connections w/ Separate Work Cables
Ref. 225 543 / 802 292-A
! Stop engine.
NOTICE − Do not exceed machine duty
cycle.
Use Dual Operator mode for CC and
CV welding (see Section 6-1).
See Section 5-17 for proper cable size.
1 Strain Reliefs
Route cables through strain reliefs.
2 Wire Feeder Cables
3 Work Cables
For MIG and FCAW welding Direct Current
Electrode Positive (DCEP), connect work
cables to Negative (−) terminals and wire
feeder cables to CV terminals.
For MIG and FCAW Direct Current Elec-
trode Negative (DCEN), connect work
cables to CV terminals and wire feeder
cables to Negative (−) terminals.
If unit has the Polarity switch option, con-
nect work cables to Work receptacles and
wire feeder cables to CV receptacles.
Place optional Polarity switches in Re-
verse position when using CV weld re-
ceptacles. There is no CV weld output
when switch is in Straight position.
Be sure Process Selector and Polarity
switches are set correctly. See Section
6-3.
Tools Needed:
Welder A (Left) Side
3/4 in
Welder B (Right) Side
1
2
3
2
Direct Current Electrode Positive
(DCEP) connections are shown.
Note position
of Process
Selector
switches.
Note position
of optional
Polarity
switch.
Note position
of optional Po-
larity switch.




 To Next Page