-- 1 0 --
bh36d1ea
8 MMA WELDING
8.1 Symbol and function explantions
MMA weld in g
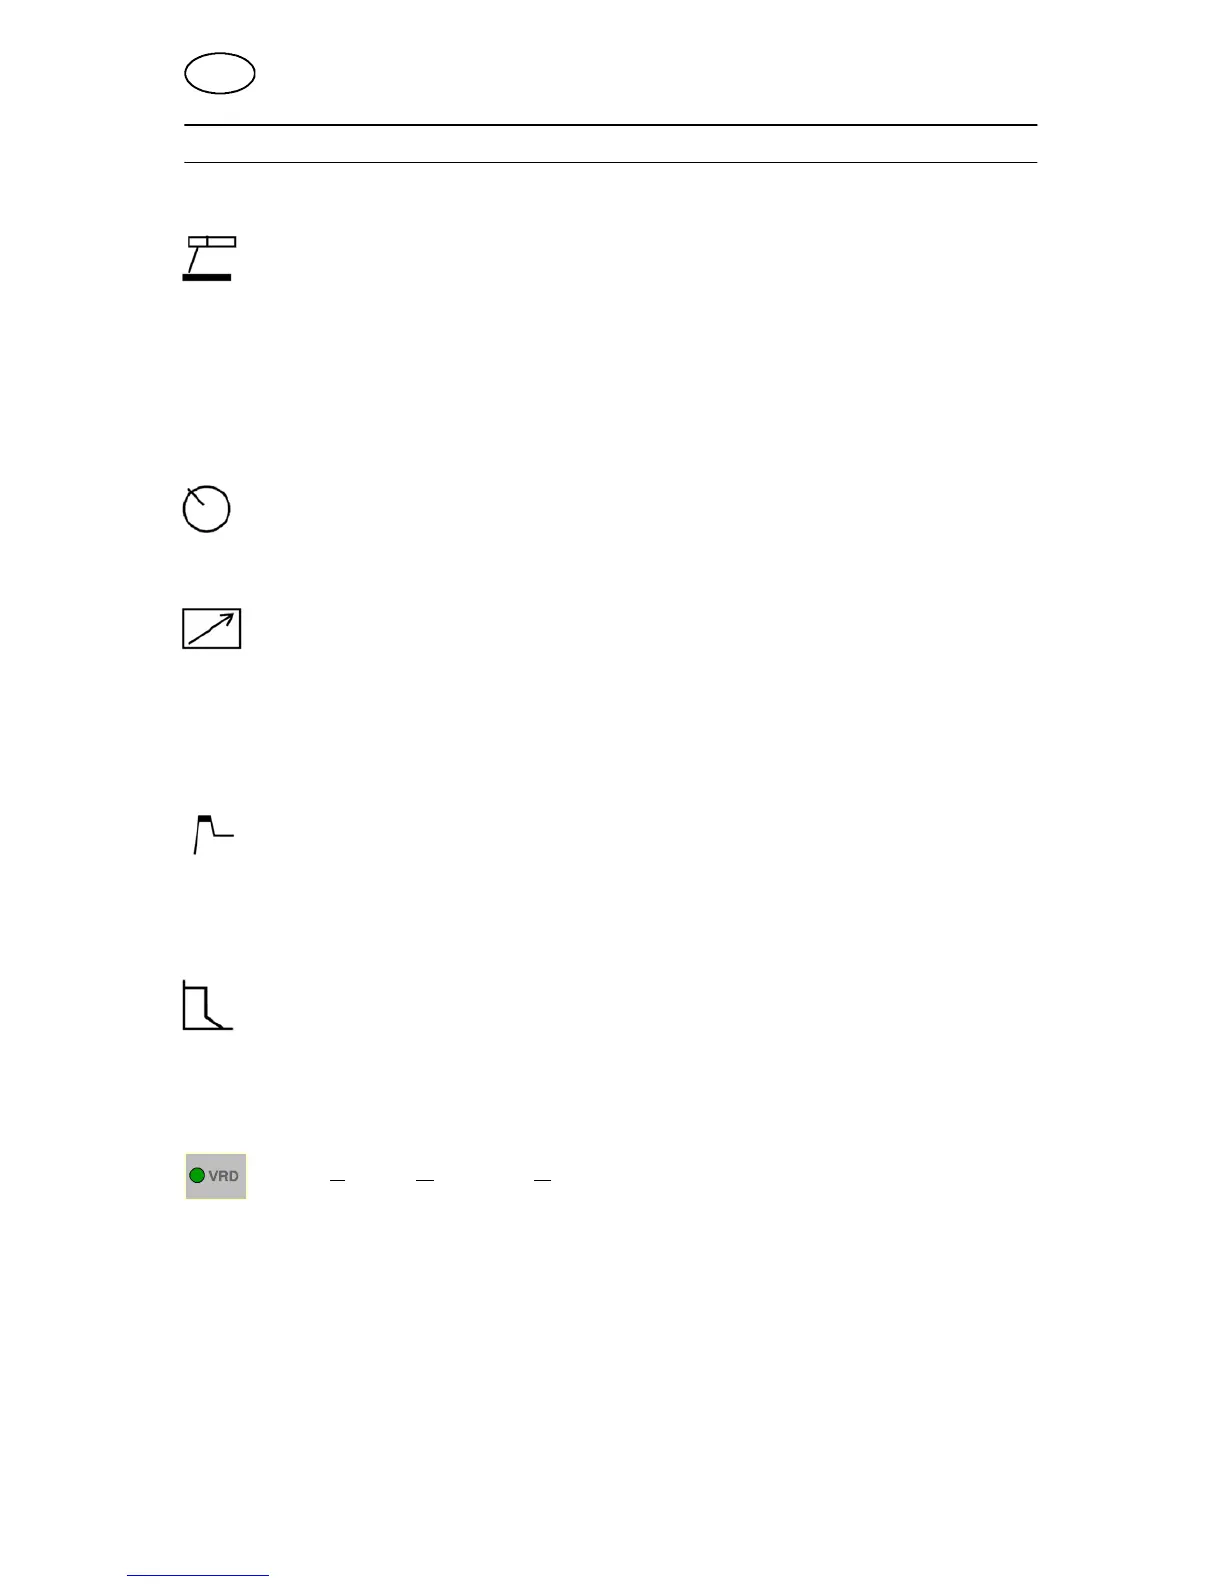
MMA welding may also be referred to as welding with coated electrodes. Striking the
arc melts the electrode, and its coating forms protective slag.
Setting current
A higher current produces a wider weld pool, with better penetration into the
workpiece.
Active panel
Settings are made from the control panel.
Remote control unit
Settings are made from the remote control unit.
The remote control unit must be connected to the remote control unit socket on the
machine before activation. When the remote control unit is activated the panel is
inactive.
Hot Start
Increases the welding current during a fixed time at the start of the welding process.
Set the value of the hot start current by using the knob. This reduces the risk of
incomplete fusion at the start of the weld.
Arc force
The arc force is important in determining how the current changes in response to a
change in the arc length. A lower value gives a calmer arc with less spatter.
VRD (Voltage Reduction Device)
Note! The VRD function is not active (LED has gone out) on delivery. Contact an
authorised ESAB service technician to activate the function.
The VRD function ensures that the open--circuit voltage does not exceed 35 V when
welding is not being carried out. This is indicated by a lit VRD LED. The VRD
function is deactivated when the system senses that welding has started.
If the VRD function is activated and open--circuit voltage exceeds the 35 V limit, this
is indicated by an error message (16) appearing in the display and welding cannot
be started whilst the error m essage is displayed.
GB




 To Next Page