5699-E P-63
SECTION 4 INSPECTION, MAINTENANCE AND ADJUSTMENTS
Procedure :
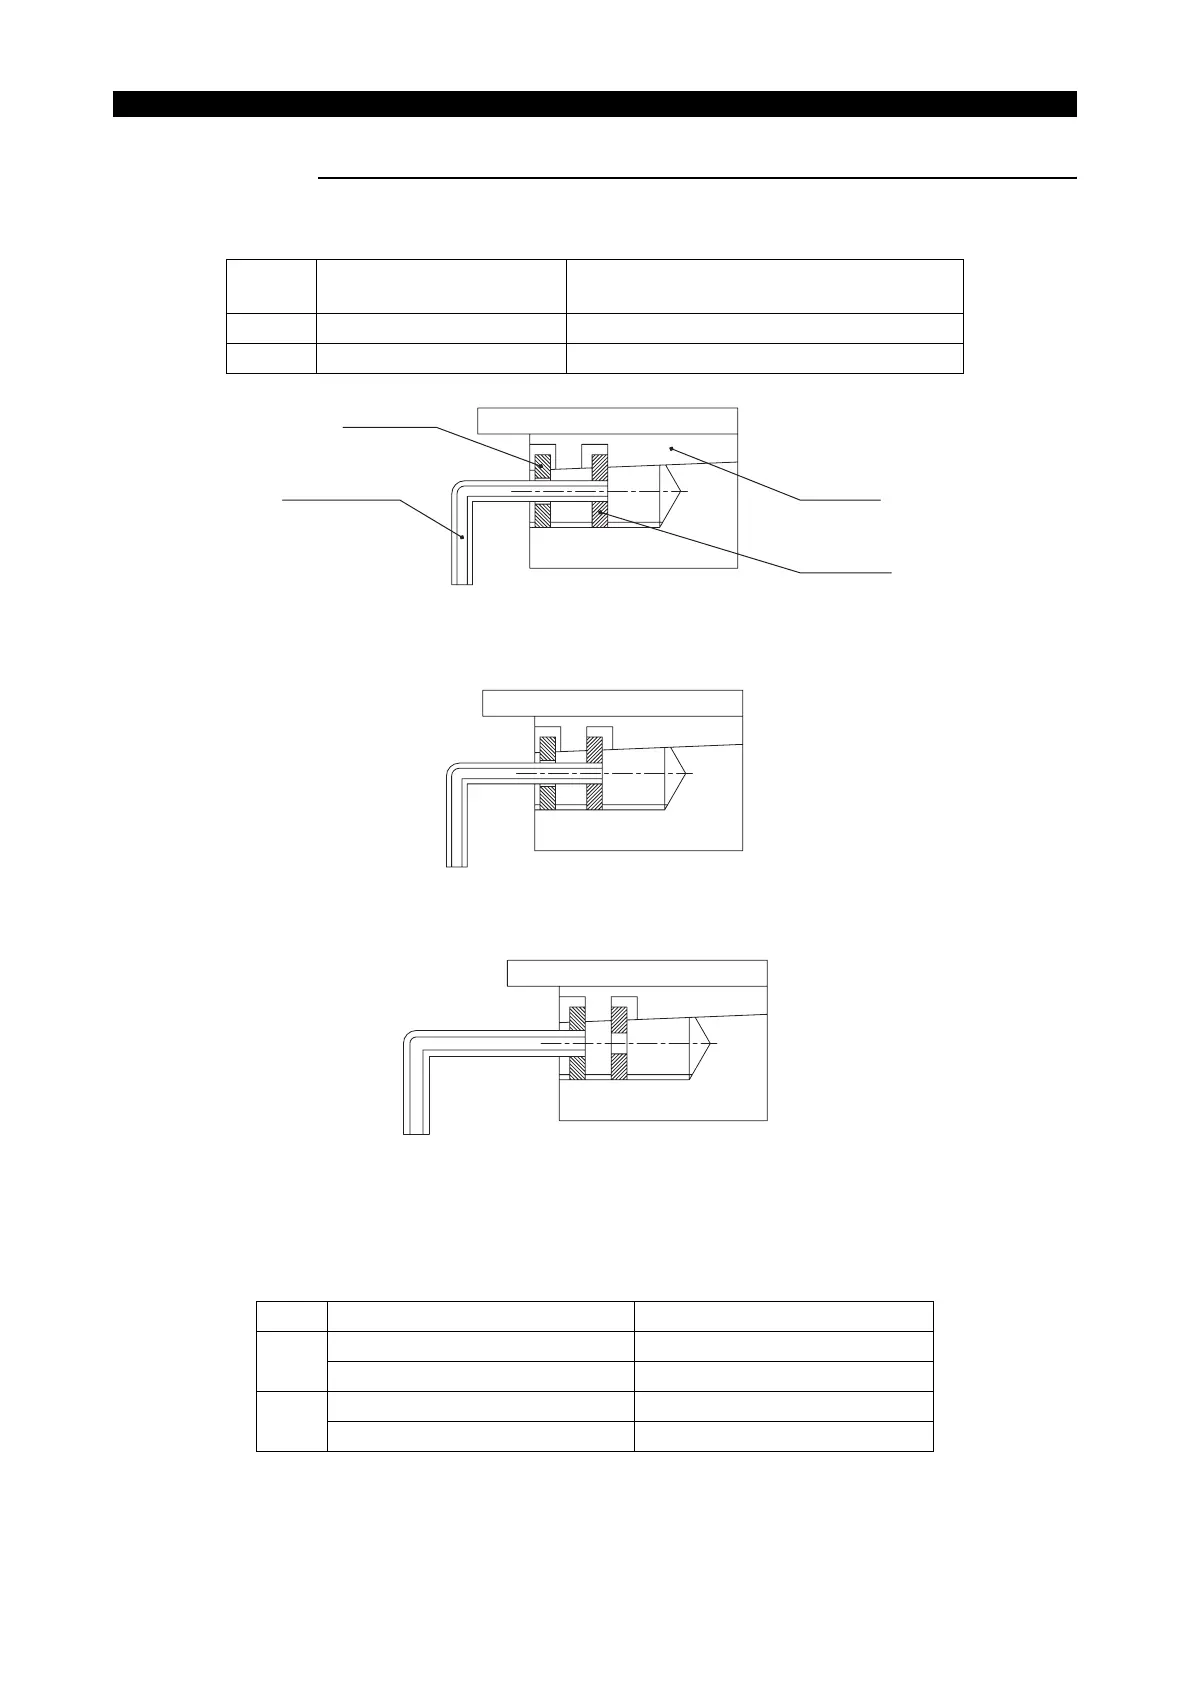
1- Tighten the screw 2 until it no longer turns.
LE11214R0100600190002
2- Turn the screw 2 back by 90° to loosen.
LE11214R0100600190003
3- Tighten the screw 1 to fix the tapered gib.
LE11214R0100600190004
4- To check that each feed axis has proper load value as specified in the chart below, press the
pushbutton to feed the turret. If the load value is considerably off, adjust the screws until you
obtain the proper value.
Axis
Tightening torque
(Nm (lbf-ft))
Appropriate tools
X-axis 23.5 (17.3) Ball driver, flat head ratchet (L=120 (4.72))
Z-axis 23.5 (17.3) Ball driver, flat head ratchet (L=120 (4.72))
Axis Feedrate override (%) Load value (%)
X-axis
180 25
2500 20
Z-axis
180 80 (up), 10 (down)
2500 70 (up), 25 (down)
Screw 2
Screw 1
Tapered gib
Hexagonal wrench


 To Next Page