www.parweld.com
19
0.5 s
0.5 s
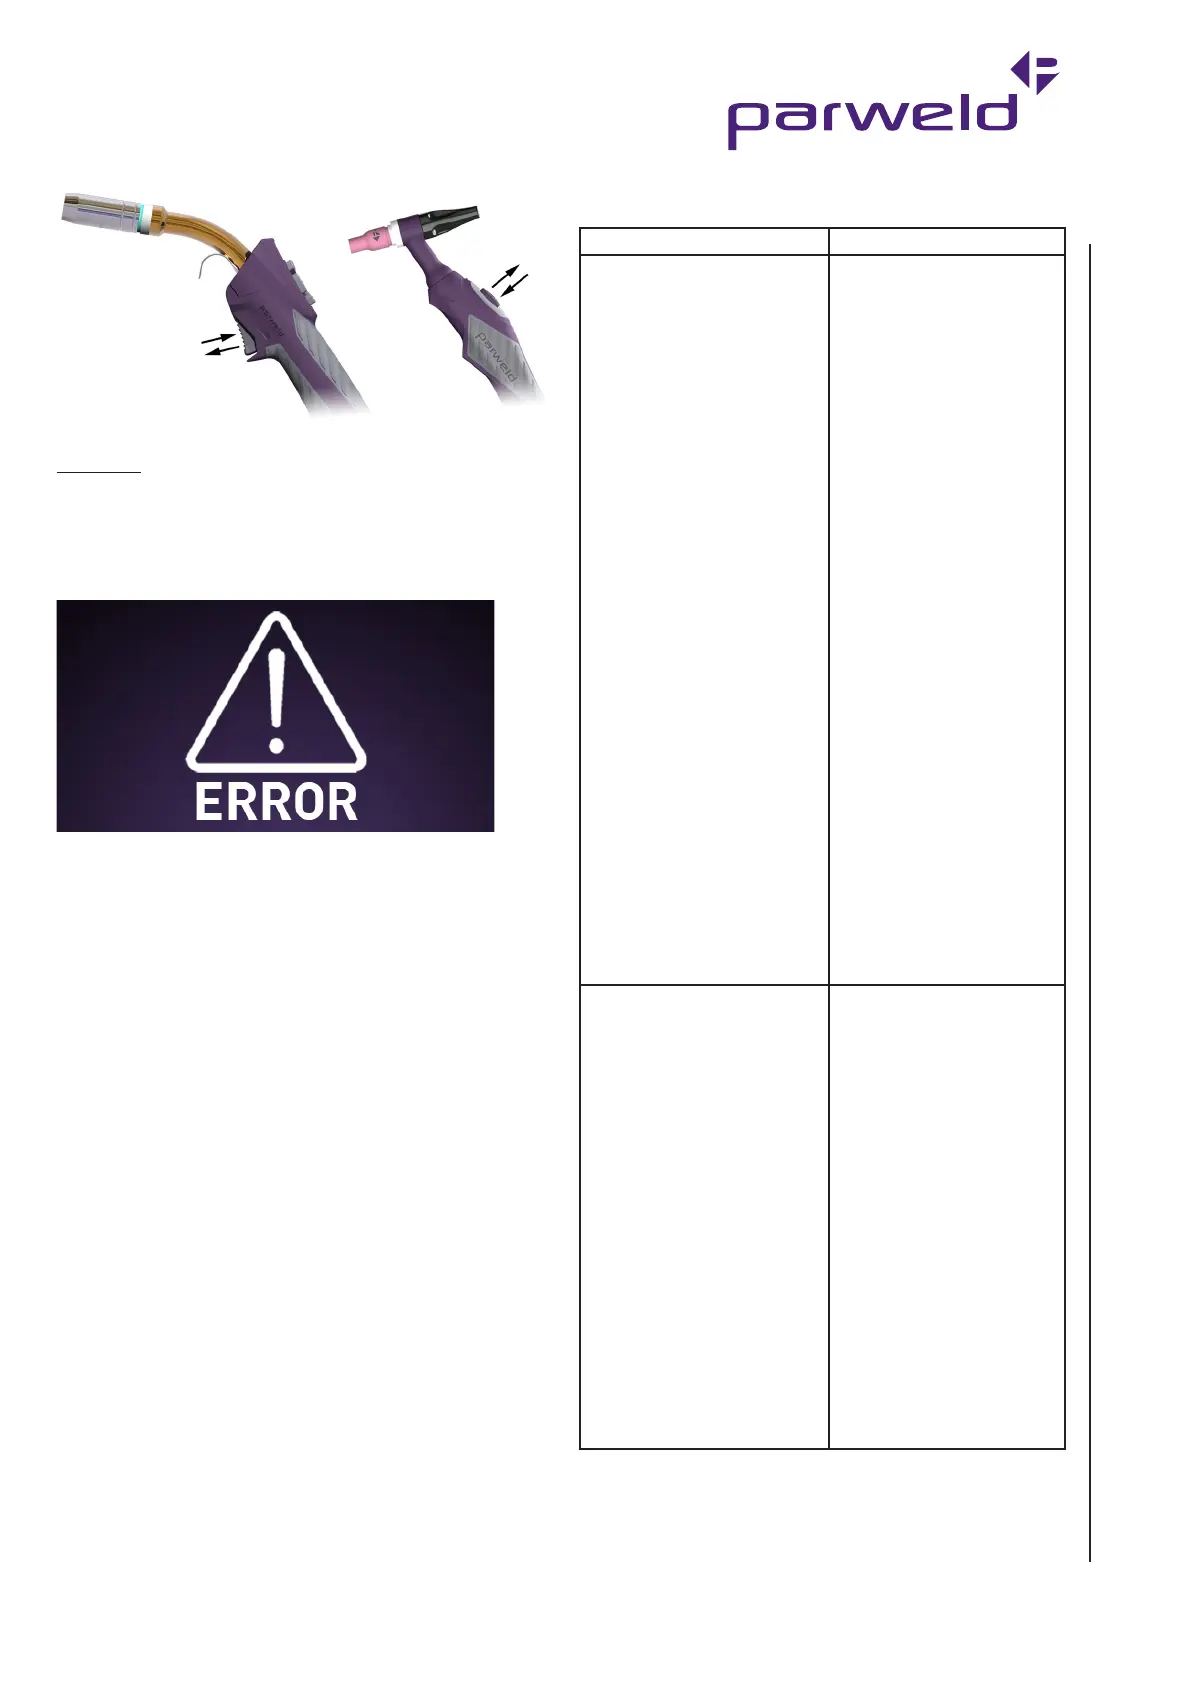
Selects MIG
Operation
Selects TIG
Operation
Please note this machine uses auto polarity switching so there is
no need to change the work lead connections on the front of the
machine.
8.0 Fault Finding
• If error message is displayed allow machine to cool with
power o for 10 minutes.
• If error remains switch o and on again.
• Reduce welding current to prevent over current condition.
• If error remains contact your local service centre.
Problem Cause/Corrective Action
Porosity - small cavities or holes
resulting from gas pockets in
weld metal.
Inadequate shielding gas
coverage. Check for proper
gas ow rate.
Remove spatter from gun
nozzle.
Check gas hoses for leaks.
Eliminate drafts near welding
arc.
Place nozzle 6-13 mm from
work piece and hold gun near
bead at end of weld until
molten metal solidies.
Wrong gas. Use welding
grade shielding gas; change to
dierent gas.
Dirty welding wire. Use clean,
dry welding wire. Eliminate
pickup of oil or lubricant on
welding wire from feeder or
liner.
Work piece dirty. Remove all
grease, oil, moisture, rust,
paint, coatings, and dirt from
work surface before welding.
Use a more highly deoxidizing
welding wire (contact supplier).
Welding wire extends too far
out of nozzle.
Be sure welding wire extends
not more than 13 mm beyond
nozzle.
Incomplete fusion to base metal. Work piece dirty. Remove all
grease, oil, moisture, rust,
paint, coatings, and dirt from
work surface before welding.
Insucient heat input. Select
higher voltage range and/or
adjust wire feed speed.
Improper welding technique.
Place stringer bead in proper
locations at joint during
welding.
Adjust work angle or widen
groove to access bottom
during welding.
Momentarily hold arc on
groove side walls when using
weaving technique.
Keep arc on leading edge of
weld puddle. Use correct gun
angle of 0 to 15 degrees.
8.1 MIG Welding Problems


 To Next Page