CHAPTER 4: DEVELOPING WELD SCHEDULES
DUAL PULSE 125
STORED ENERGY RESISTANCE WELDING POWER SUPPLY
4-2 990-270
Procedure
Developing a Weld Schedule is a methodical procedure which consists of making sample welds and
evaluating the results. The first weld should be made at low energy settings. Adjustments are then
made to adjust the parameters one at a time until a successful weld is made.
WELD HEAD - Parameter: Electrode Force
Insert the correct electrodes in the weld head. Refer to the Miyachi Unitek Resistance Welding Catalog
for Electrode Material Recommendations.
Use the Force Adjustment Knob on the Weld Head to set the Firing Force. Start at a moderate force
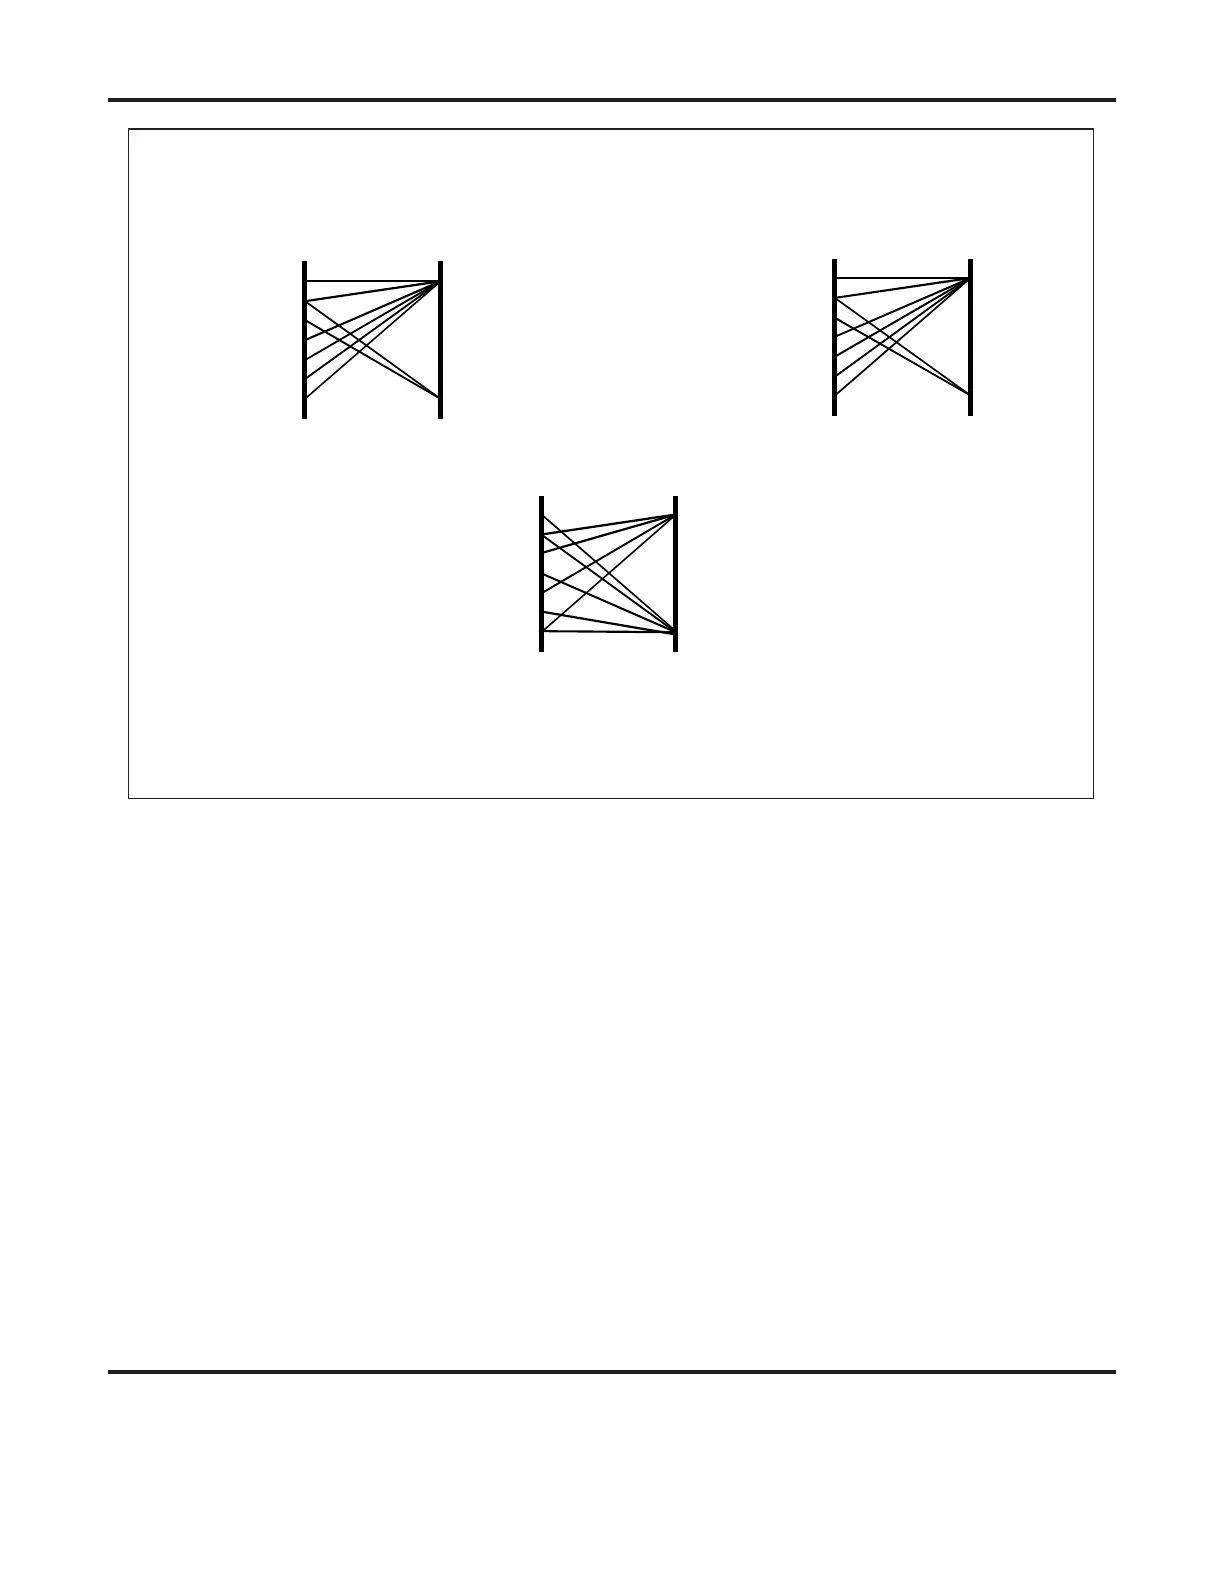
setting, #3 on a Miyachi Unitek Weld Head. Figure 4-1 illustrates the effect of electrode force on the
part.
Adjust the air pressure for Air Operated Heads. See Chapter 2.
HEAT
Excessive
Insufficient
CAUSEPROBLEM
Parts Overheating
Weak Weld
Insufficient Nugget
Metal Expulsion
Warping
Discoloration
Electrode Damage
PRESSURE
Excessive
Insufficient
CAUSE
PROBLEM
Parts Overheating
Weak Weld
Insufficient Nugget
Metal Expulsion
Warping
Discoloration
Electrode Damage
TIME
Excessive
Insufficient
CAUSE
PROBLEM
Parts Overheating
Weak Weld
Insufficient Nugget
Metal Expulsion
Warping
Discoloration
Electrode Damage
%
ENERGY
PULSE
WIDTH
FIRING
FORCE
Figure 4-1. A graphic presentation of the effects of %ENERGY, Time and
Pressure on the Weld



 To Next Page