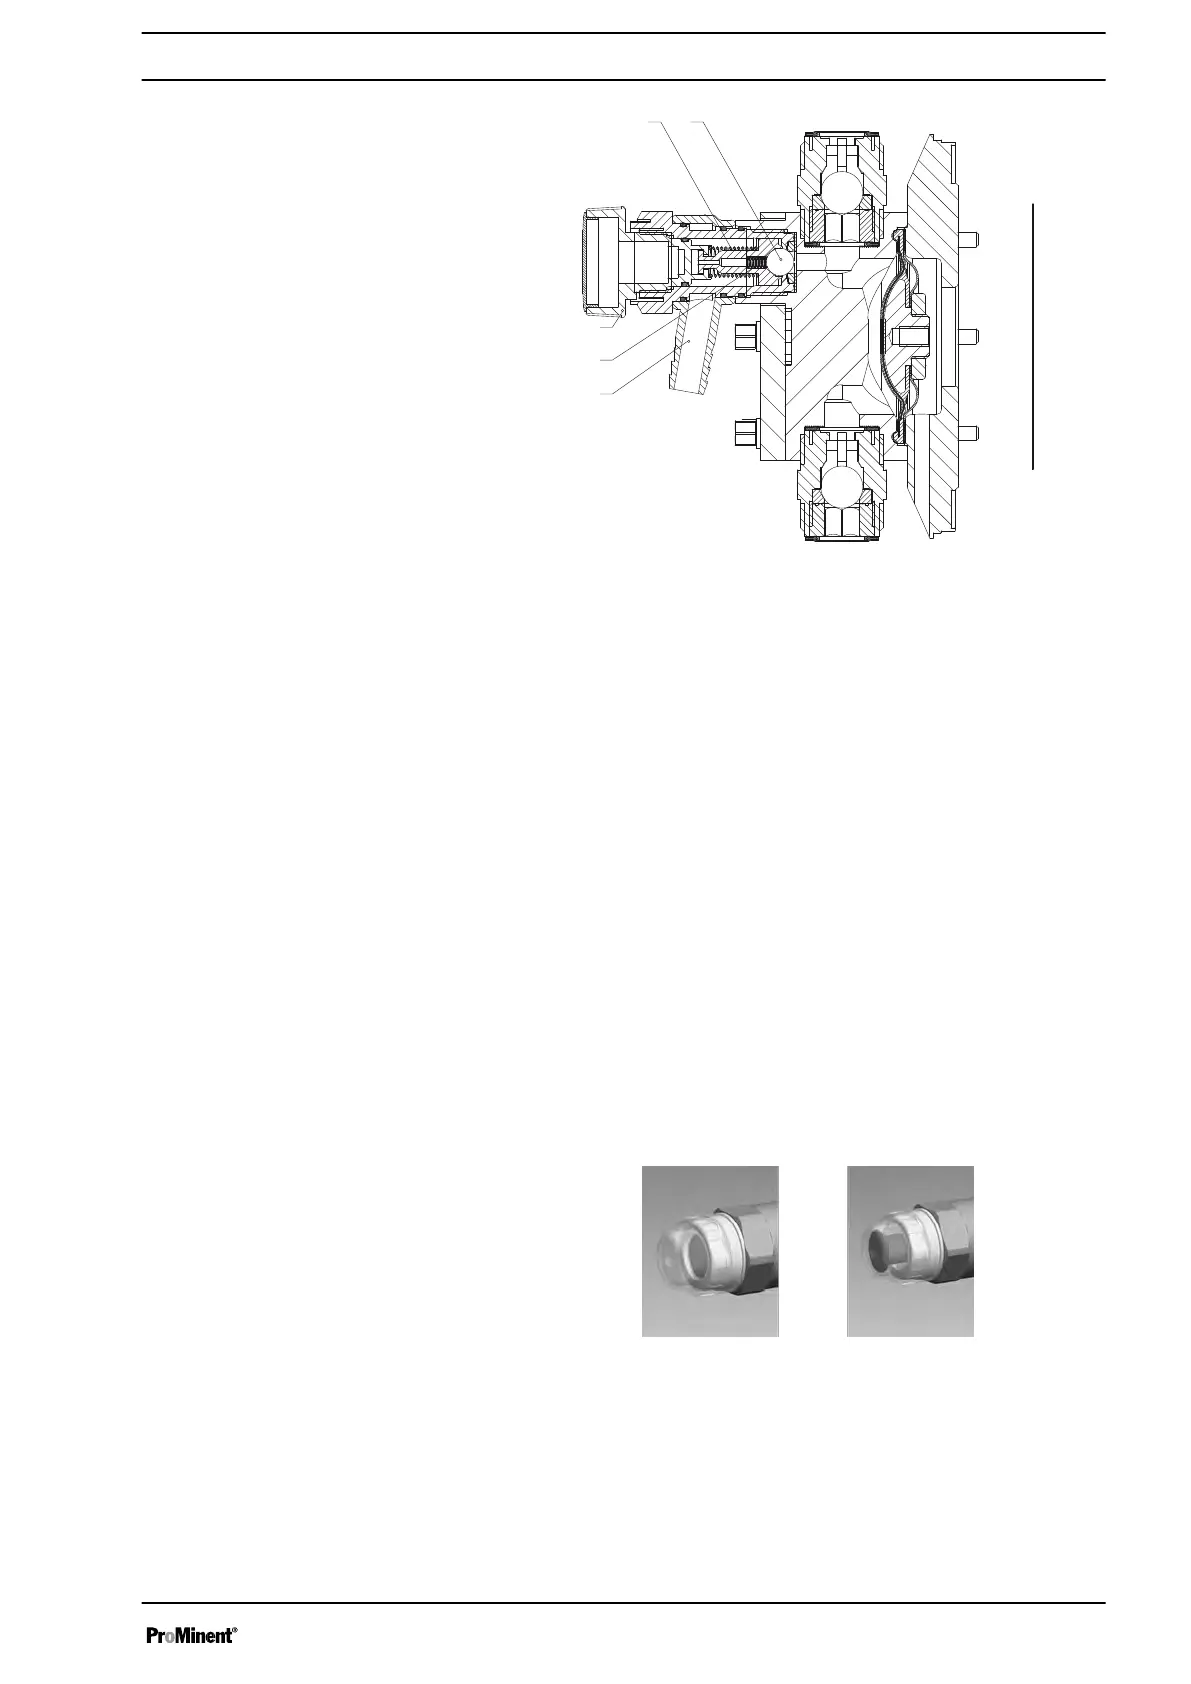
Fig. 8: Integral relief valve
1 Spring, large
2 Ball
3 Rotary dial
4 Spring, small
5 Hose connection
5.4 Multi-layer safety diaphragm
The multi-layer safety diaphragm has the same function as the conven‐
tional double diaphragm system with working and safety diaphragms; how‐
ever it also has the advantage that both diaphragms are joined together in
a single unit.
If the working layer (1) breaks, the feed chemical penetrates between the
working and safety (2) layers and spreads out. The safety layer ensures
that not feed chemical penetrates to the outside.
As soon as the feed chemical reaches the flap (3) on the edge of the multi-
layer safety diaphragm, it inflates it. The flap presses a piston (4) in the
membrane rupture sensor (5), so that this triggers.
With the visual diaphragm rupture sensor, the lowered red cylinder (6)
springs forward beneath the transparent cover (7) so that it then becomes
clearly visibleFig. 9.
With the electrical
diaphragm rupture sensor, a switch is switched. A con‐
nected signalling device must signal the diaphragm rupture.
Fig. 9: Visual diaphragm rupture sensor, triggered and untriggered
The electrical diaphragm rupture sensor is connected to the "diaphragm
rupture indicator" terminal. If a diaphragm rupture occurs, the red LED
“Fault”
indicator illuminates on the pump, the identifier
“Error”
and
“DIAPH”
flash on the LCD screen. Dependent on the identity code variant
selected under "Displacement body", the pump either continues metering
(
“Pump emits alarm”
) or stops (
“Pump stops”
).
Functional description
17



 To Next Page