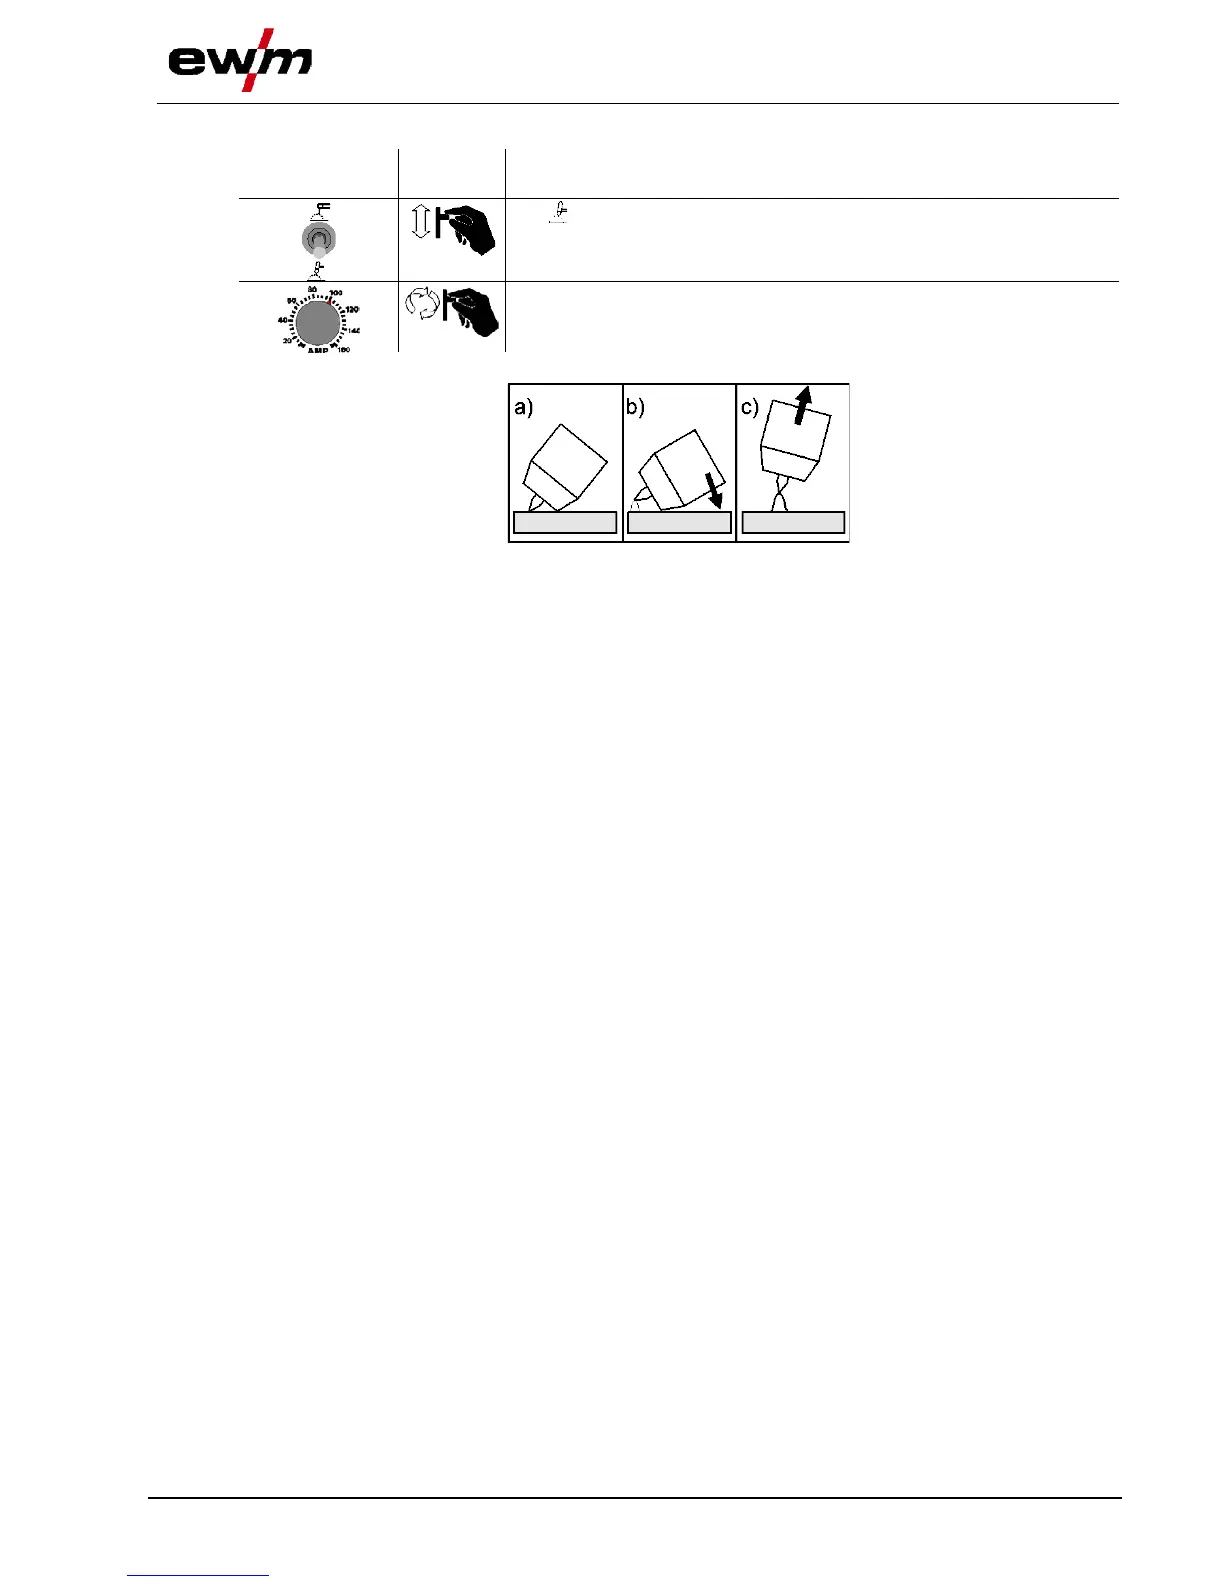
5.6.1.4 TIG arc ignition
Figure 5-6
The arc is ignited on contact with the workpiece:
a) Carefully place the torch gas nozzle and tungsten electrode tip onto the workpiece (liftarc current
flowing, regardless of the main current set).
b) Incline the torch towards the torch gas nozzle until there is a gap of approx. 2-3mm between the tip of
the electrode and the workpiece (arc ignites, current increases to the main current set).
c) Lift off the torch and swivel to the normal position.
Ending the welding process: Remove the torch from the workpiece until the arc goes out.


 To Next Page