Function description
Operating Manual PSENvip RL D P Set
1001641-EN-09
| 35
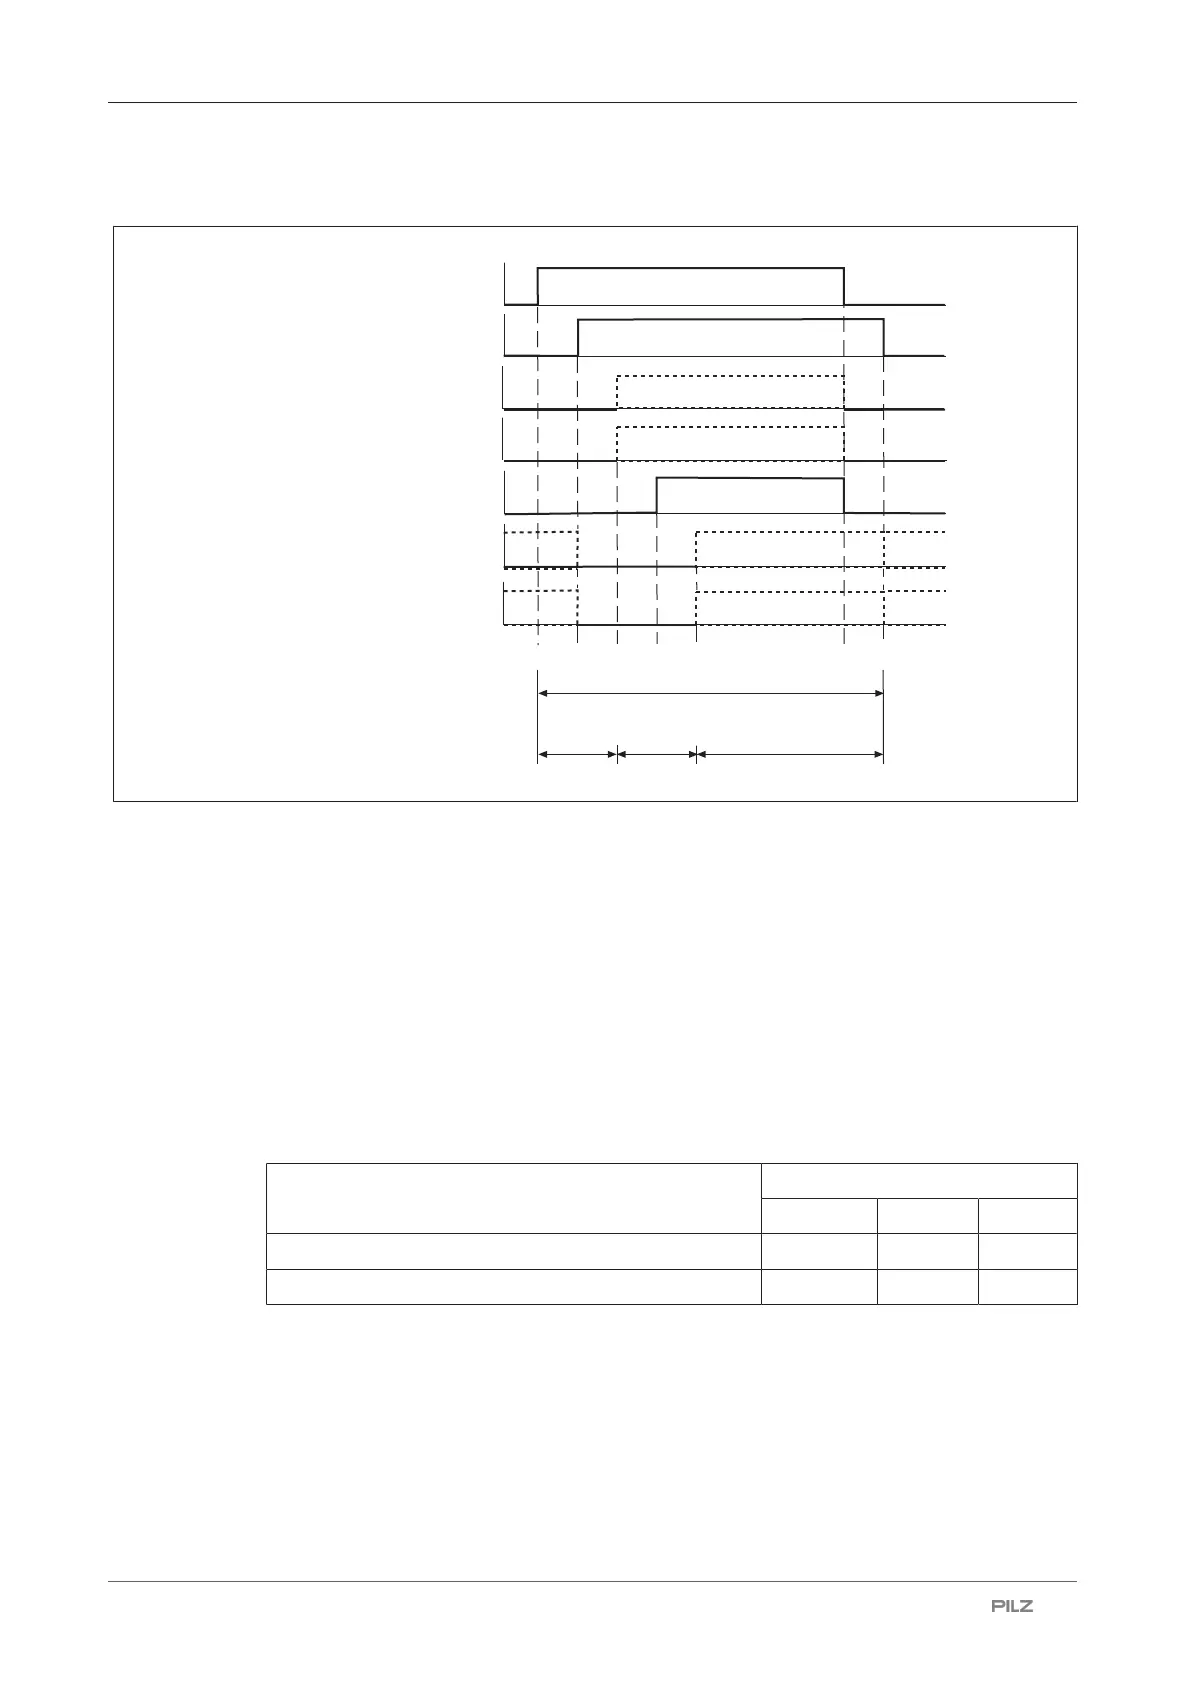
Communication sequence:
PLC Ready
1
0
1
0
1
0
1
0
1
0
Activate
Acknowledge PSENvip -> PLC
1
0
Tool class PSENvip -> PLC Bit 1
1
0
Tool class PSENvip -> PLC Bit 2
Tool class PLC -> PSENvip Bit 1
Tool class PLC -> PSENvip Bit 2
1 2 3 4 5 6 7
max. 600 ms
max.
200 ms
max.
200 ms
max.
200 ms
} 1
– The PSENvip starts communication.
Activate = 0/1 pulse edge
– Tool class PLC -> PSENvip Bit 1/2: Bits can have any status
} 2
– The safety system is ready for communication.
PLC Ready = 0/1 pulse edge
– Tool class PLC -> PSENvip Bit 1/2 = 0 to step 5
} 3
The PSENvip sends the detected tool class to the safety system.
Tool class
1 2 3
Tool class PSENvip -> PLC Bit 1 0 1 1
Tool class PSENvip -> PLC Bit 2 1 0 1
} 4
The PSENvip confirms the validity of the tool class registered on the safety system in step
3.
Acknowledge PSENvip -> PLC = 0/1 pulse edge


 To Next Page