9 TROUBLESHOOTING
0463 772 001
- 34 -
© ESAB AB 2023
9 TROUBLESHOOTING
Perform these checks and inspections before sending for an authorised service technician.
Check that the mains voltage is disconnected before starting any type of repair action.
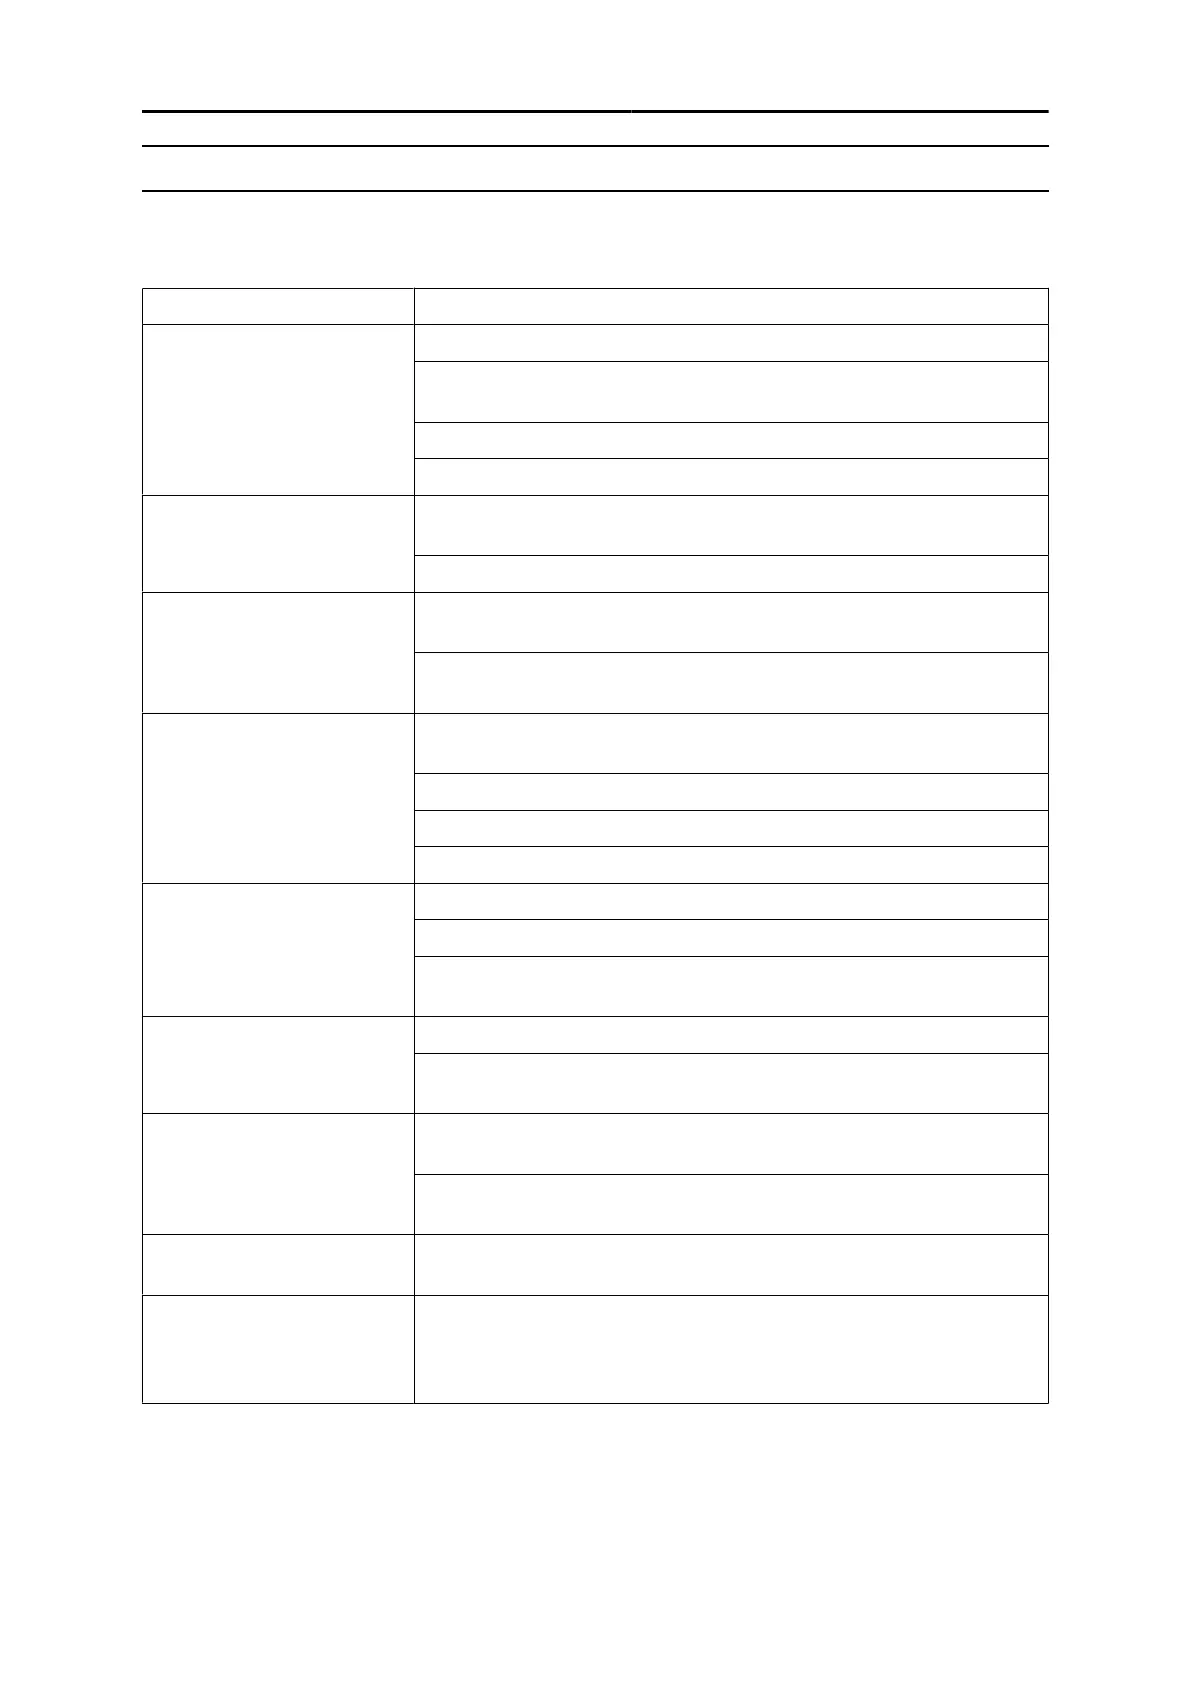
Type of fault Corrective action
No arc Check that the mains power supply switch is turned ON.
Check that the mains, welding and return cables are correctly
connected.
Check that the correct current value is set.
Check the mains power supply fuses.
The welding current is
interrupted during welding
Check whether the thermal protection trip has operated (indicated by
LED on Overtemperature indicator in control panel).
Check the mains supply fuses.
The thermal protection trips
frequently
Make sure that you are not exceeding the rated data for the power
source (i.e. that the unit is not being overloaded).
Check that the ambient temperature is not above the one for the rated
duty cycle 40°C/104°F.
Poor welding performance Check that the welding current supply and return cables are correctly
connected.
Check that the correct current value is set.
Check that the correct welding wires are being used.
Check the main power supply fuses.
Poor cooling effect Clean the cooling element using compressed air.
Check the coolant level.
Check that the ambient temperature is not above the one for the rated
duty cycle 40°C/104°F.
Intermittent gouging stops or
contact between carbon and
metal lost
Air pressure is too high. Reduce the air pressure.
Check the air pressure whether it is set to the recommended value.
Check the manual of the torch used.
Carbon deposit on the gouge
metal
Air pressure is too low. Turn on air before striking the arc and air
should flow between the electrode and the workpiece.
Check the air pressure whether it is set to the recommended value.
Check the manual of the torch used.
No arc during start or erratic
arc during gouging
Check whether the voltage is set to the recommended value.
Intermittent arc action
resulting in an irregular
groove surface or copper
deposition on the metal plate
Check whether the voltage is set to the recommended value.


 To Next Page